Why Printing Paste Viscosity Drops After Adding Dye, Salt or Alkali
Printing paste can become thinner after dye, salt or alkali is added because of simple...
Printing paste viscosity can fall after dye, salt or alkali is added because of dilution, electrolyte response, a pH shift, ingredient interactions, temperature or preparation history. Start with a matched comparison before changing the thickener dose. Sodium alginate, CMC and commercial synthetic grades—including the selected FSX CMS route—need their own formulation tests. Calcium can also increase alginate association or form gel rather than simply thinning the paste. This guide explains how to build a controlled diagnostic sequence and approve the finished print.
Why Printing Paste Can Become Thinner After Chemical Addition
A stock thickener is usually measured under a simple, controlled condition such as thickener + water + defined concentration + defined temperature. The production printing paste is different.
It can contain dye solution or pigment dispersion, salt, alkali, urea or humectants, dispersing agents, binders, fixers, reducing or oxidizing auxiliaries, wetting agents and defoamers.
Each addition changes either the polymer concentration, the chemical environment, the temperature, or all three.
FSX Chemical’s current technical guidance therefore recommends measuring viscosity after critical components are added rather than assuming that the water-only stock paste predicts the final formula.
The useful question is not “Why did the thickener fail?” It is “Which variable changed when the viscosity changed?”
Alkali, acid or dye package creates a non-dilution change
Temperature / measurement effect
Sample is warmer or test conditions differ
Viscosity partly recovers after conditioning to standard temperature
More than one mechanism can occur in the same paste. A reactive dye solution can simultaneously add water, urea, dye-associated salts and heat.
If all components are added at once, the root cause becomes difficult to identify.
1. Dilution: Did You Simply Reduce the Polymer Concentration?
This is the simplest explanation and one of the easiest to overlook.
Suppose a mill prepares a concentrated stock thickening and then adds a dye solution containing dye, water, urea and other dissolved auxiliaries. The final paste now contains the same amount of polymer distributed through a larger total mass or volume.
The effective thickener concentration has decreased.
Because polymer concentration and viscosity are often strongly nonlinear, even a moderate dilution can create a large viscosity drop.
Before blaming salt or dye chemistry, calculate:
Supplied-thickener concentration in final paste (wt%) = mass of supplied product represented in that paste ÷ total final paste mass × 100. Include product already present in a weighed stock. If calculating polymer instead, use a separately documented polymer mass fraction; total product solids are not automatically active polymer. State the concentration basis and use compatible mass units.
Then prepare a dilution control:
Equal stock portions + either the actual commercial addition or reference water of the same total addition mass. Balance to the same final mass and supplied-thickener concentration; a more concentrated unadded stock is a separate baseline.
A similar result in a matched water-addition control is consistent with dilution contributing; it does not show that dilution dominates or rule out ingredient interactions. Match final thickener concentration, total sample mass, temperature, mixing and elapsed time, and record pH. Opposing ionic, pH or association effects can give a similar endpoint, so investigate appearance, holding response and the complete print as well.
2. Electrolyte Screening: Why Salt Can Collapse an Anionic Polymer Coil
Sodium alginate and sodium CMC carry anionic groups under suitable aqueous conditions. The charge and response of a commercial synthetic product should be taken from its grade-specific information, not inferred from the FSX CMS series name. The following screening explanation applies to anionic systems where that mechanism is relevant.
These charged polymer chains can expand because like charges along the chain repel each other. When monovalent salts are added, dissolved ions can screen part of that electrostatic repulsion.
The chain can adopt a more compact conformation, reducing its hydrodynamic volume and apparent thickening efficiency.
This general polyelectrolyte mechanism is well established: increasing ionic strength can reduce intrinsic viscosity because charge screening allows an expanded anionic chain to contract.
The size of the effect depends on thickener chemistry, degree of substitution where relevant, molecular weight, polymer concentration, salt type, salt concentration and water hardness.
There is no universal percentage viscosity loss after salt addition.
3. Alkali: pH Change and Ionic Strength Happen Together
Alkali is more complicated than a neutral salt.
When sodium bicarbonate, sodium carbonate, sodium hydroxide or another alkaline material is added, at least two variables can change: pH and ionic strength.
Depending on the polymer, pH can change ionization of carboxyl groups, hydration, polymer-chain conformation and compatibility with other paste components.
At the same time, sodium-containing alkali increases the concentration of counterions in solution.
Therefore, if viscosity falls after alkali addition, do not conclude “High pH destroyed the thickener.”
First investigate final pH, alkali identity, dosage, ionic strength, water quality, temperature and addition order.
In reactive printing, alkali timing also affects dye chemical stability, which is separate from thickener rheology.
4. Dye Addition: Colorant Chemistry Is More Than “Adding Color”
A dye product is not always chemically neutral to the thickener.
Depending on dye class and commercial form, the colorant addition can introduce water, electrolytes, dispersants, solubilizing agents, pH-control chemicals and other formulation components.
Reactive dye solutions can change ionic strength and pH. Disperse dyes are supplied as dispersions containing dispersing chemistry and fine particles. Pigment dispersions can interact with binder and synthetic-thickener systems.
FSX Chemical’s current CMC/CMS technical guidance notes that viscosity changes after colorant addition can result from electrolyte, pH or ingredient compatibility and recommends testing the stock paste and final color paste under the same conditions.
Do not compare only “before dye” and “after dye.” Also compare:
Water-Dilution Control vs. Dye-Containing Sample
A controlled difference between those samples can indicate a response to the commercial dye package beyond the chosen water-addition control. It does not isolate dye molecules from the salts, dispersants, pH or other ingredients supplied with them. A similar viscosity reading likewise does not prove the chemistry had no effect.
5. Temperature: A Hidden Reason the Final Paste Reads Lower
Viscosity is temperature-dependent.
A printing paste can become warmer because dye was dissolved in warm water, urea solution was heated, high-speed mixing generated heat, or the color kitchen is warmer than the QC laboratory.
If the stock paste is measured at 25°C and the completed paste is measured at 32°C, part of the apparent viscosity loss may simply be a temperature effect.
A useful control is:
Measure Warm → Condition Back to Standard Temperature → Measure Again
If viscosity recovers substantially after temperature conditioning, the original comparison was not temperature-controlled.
Do not correct such a paste by adding more thickener before confirming the test temperature.
Why Addition Order Can Change the Result
The final ingredient list is not the whole formula. The sequence of addition can change local chemical conditions during mixing.
A practical general principle in printing-paste preparation is to add thinner solutions or dispersions gradually into a well-prepared thickening while maintaining controlled agitation.
This can reduce local over-dilution, localized high salt concentration, gel or floc formation and poor dye dispersion.
For many water-soluble polysaccharide thickeners, a useful starting sequence is:
Water → Controlled Thickener Hydration → Dye/Auxiliary Addition → Salt/Alkali at the Validated Stage → Final Adjustment
This is not a universal recipe. Some pigment or specialty formulations require a different order because binder, neutralizer, synthetic thickener or fixer interactions dominate.
Local High Concentration vs. Final Average Concentration
A formula can be chemically acceptable at its final average composition and still fail during addition.
Pouring concentrated salt or alkali directly into one region of a thickener paste creates a temporary local concentration far higher than the final calculated value.
That can cause local polymer collapse, gel particles, flocculation or irreversible-looking lumps.
Possible controls include pre-dissolving the chemical where the process allows, adding gradually, maintaining effective circulation and avoiding dead zones in the tank.
Therefore, “same final formula” does not always mean “same paste” if the addition procedure changes.
How Sodium Alginate Can Respond
Sodium alginate is an anionic polysaccharide widely used as a benchmark thickener in conventional reactive printing.
Monovalent electrolytes can alter chain expansion and apparent viscosity.
However, sodium alginate has an important exception: divalent calcium can create stronger interchain association and may increase viscosity or cause gelation rather than thinning.
If alginate viscosity changes after salt or alkali addition, check whether the change is a drop or increase, total hardness, calcium contamination, final electrolyte package and temperature.
Carboxymethyl cellulose is also an anionic polymer.
Its salt tolerance depends strongly on the commercial grade, including degree of substitution, substitution uniformity, molecular weight, purity and concentration.
Published reviews of CMC note that degree of substitution has a significant effect on solubility, viscosity stability and salt tolerance.
A CMC grade that produces high viscosity in pure water can therefore lose more or less viscosity in an electrolyte-containing print paste than another grade with a similar initial viscosity.
Pure-water viscosity and salt tolerance are separate purchasing parameters.
How CMS Can Respond
FSX CMS is a commercial synthetic printing-thickener family, not a chemical composition established by the letters CMS. Do not assign a starch backbone, ionic character, CMC degree of substitution or a digital-printing approval from the series name. Confirm the selected grade’s current TDS and intended dye, fabric and application route.
Test the actual commercial CMS grade after the intended dye, salt and alkali additions, using its supplier-approved preparation sequence. A useful comparison fixes the supplied-product concentration and final sample mass, records pH and temperature, and checks gel, floc, separation and holding behavior as well as apparent viscosity.
Different grades may respond differently because their documented composition, formulation and preparation requirements differ. Generic carboxymethyl starch is a separate modified-starch chemistry; if that material is being evaluated, identify it explicitly and obtain its own specifications. Do not transfer its substitution or starch-structure explanation to FSX CMS.
Therefore, a CMS grade should be tested at:
Stock Paste → After Dye → After Salt → After Alkali → After Holding
rather than selected by water viscosity alone.
How Synthetic Thickeners Can Respond
Synthetic printing thickeners cover multiple commercial architectures and applications, including FSX CMS grades where specified. Confirm each grade’s declared composition information and activation method, then test it in the intended complete paste. BYK’s acrylic-thickener guidance describes neutralization-driven swelling as one synthetic mechanism; it does not establish the composition or activation route of an individual FSX CMS grade.
Some synthetic thickener systems are highly sensitive to electrolyte concentration, neutralization state and binder/auxiliary chemistry.
Possible symptoms include rapid viscosity loss after pigment or binder addition, loss of body after salt contamination and different viscosity after pH adjustment.
Because commercial synthetic thickeners vary widely, do not transfer an electrolyte rule from one product to another.
In pigment printing, evaluate the complete Pigment + Binder + Thickener + Fixer + Auxiliaries system rather than testing the thickener in water alone.
Important Exception: Calcium Can Increase Viscosity or Cause Gelation
Not every ion causes viscosity loss.
Multivalent ions can create stronger interactions with anionic polysaccharides. The clearest textile example is sodium alginate with Ca²⁺.
The progression can be:
Normal Alginate → Increased Association → Higher Apparent Viscosity → Gel Particles → Calcium Alginate Gel / Precipitate
If the paste becomes unexpectedly thicker after adding an auxiliary or using a new water source, do not assume the thickener concentration increased. Check calcium and other multivalent contamination.
This exception is why the title describes a common problem—not a universal rule for every chemical addition.
The Best Diagnostic: Build the Formula in Stages
The most useful troubleshooting experiment is a staged addition test.
Stage 0: Stock Thickener
Measure the fully hydrated thickener under the standard method.
Stage 1: Dilution Control
For a proposed dye-package comparison, split a uniform stock into equal portions. Add reference water to the control equal to the total mass of dye solution or dispersion added to the test portion, not just the water contained in that product. Keep final mass and thickener concentration on the same basis; the unadded stock remains a separate baseline.
Stage 2: Add Dye
Use the real dye solution or dispersion.
Stage 3: Add Salt / Electrolyte
Use the production identity and dosage.
Stage 4: Add Alkali or pH-Control Component
Add using the approved sequence.
Stage 5: Add Remaining Auxiliaries
Complete the formula.
Stage 6: Hold
Measure again after realistic production holding time.
At every stage, record paste mass, temperature, pH, conductivity where useful, viscosity, appearance, gel/floc and foam.
This creates a viscosity-loss map of the formula.
How to Test Whether the Dye Is the Cause
Use three samples prepared from the same stock paste.
Namuna
Addition
Purpose
A
Nothing
Stock-paste baseline
B
Reference water equal to the total mass of the dye solution or dispersion added to C
Water-addition reference at matched final mass and thickener concentration
C
Actual dye solution/dispersion
Response to the complete commercial dye addition under matched handling
If B and C are similar, dilution may contribute, but the comparison cannot establish dominance or exclude chemical effects. If C differs from B, examine the commercial dye’s salts, dispersants, pH and other ingredients using further controlled trials. Record sample mass, pH, temperature, mixing and elapsed time for each arm.
If C drops substantially more than B, investigate dye-associated salt, pH, dispersant/solubilizer and polymer-dye interaction.
Repeat with representative light and dark shades if dye loading changes widely in production.
How to Build a Salt-Response Test
Prepare one fully hydrated thickener stock and split it into equal samples.
For each salt level, keep the final thickener concentration and total sample mass on the same declared basis. If using an aqueous salt stock, give its reference arm water equal to the total salt-solution mass added; account separately for dry-salt and balancing-water additions where relevant. Report salt identity and mass per final sample mass, temperature, mixing, pH and elapsed time. Identify the matched no-salt reference used in a retention ratio rather than automatically using the more concentrated pre-addition stock.
Likewise, restoring the original stock-paste viscosity by adding more thickener does not guarantee better printing.
The corrected paste can become too elastic, difficult to transfer, too high in polymer solids or harder to wash off.
The target is the approved application rheology—not the original water-only viscosity number.
Should You Add More Thickener to Correct the Viscosity?
Only after the cause is identified.
Ushbu ketma-ketlikni ishlating:
Verify Test Method → Check Dilution → Check Temperature → Identify Chemical Effect → Print Test → Then Consider Dosage Adjustment
Adding dry powder directly to an already completed paste can create incomplete hydration, lumps, local high concentration and air incorporation.
If a dosage correction is technically justified, use a controlled preparation method such as an approved concentrated stock paste or the mill’s validated correction procedure.
Then recheck the complete print result.
Muammolarni bartaraf etish jadvali
Kuzatilgan muammo
Tekshirilishi kerak bo'lgan birinchi o'zgaruvchilar
Paste becomes thicker or gels after chemical addition
Calcium/multivalent ions, local concentration
All salts reduce viscosity
Viscosity is lower but printing remains good
Shear rheology, recovery, deposit
Original stock viscosity must be restored
Corrected paste becomes hard to wash
Excess thickener solids, dosage correction
More viscosity always improves printing
Same formula differs between shifts
Water, temperature, addition order, holding time
Thickener batch is the only variable
Production QC and Formula Control
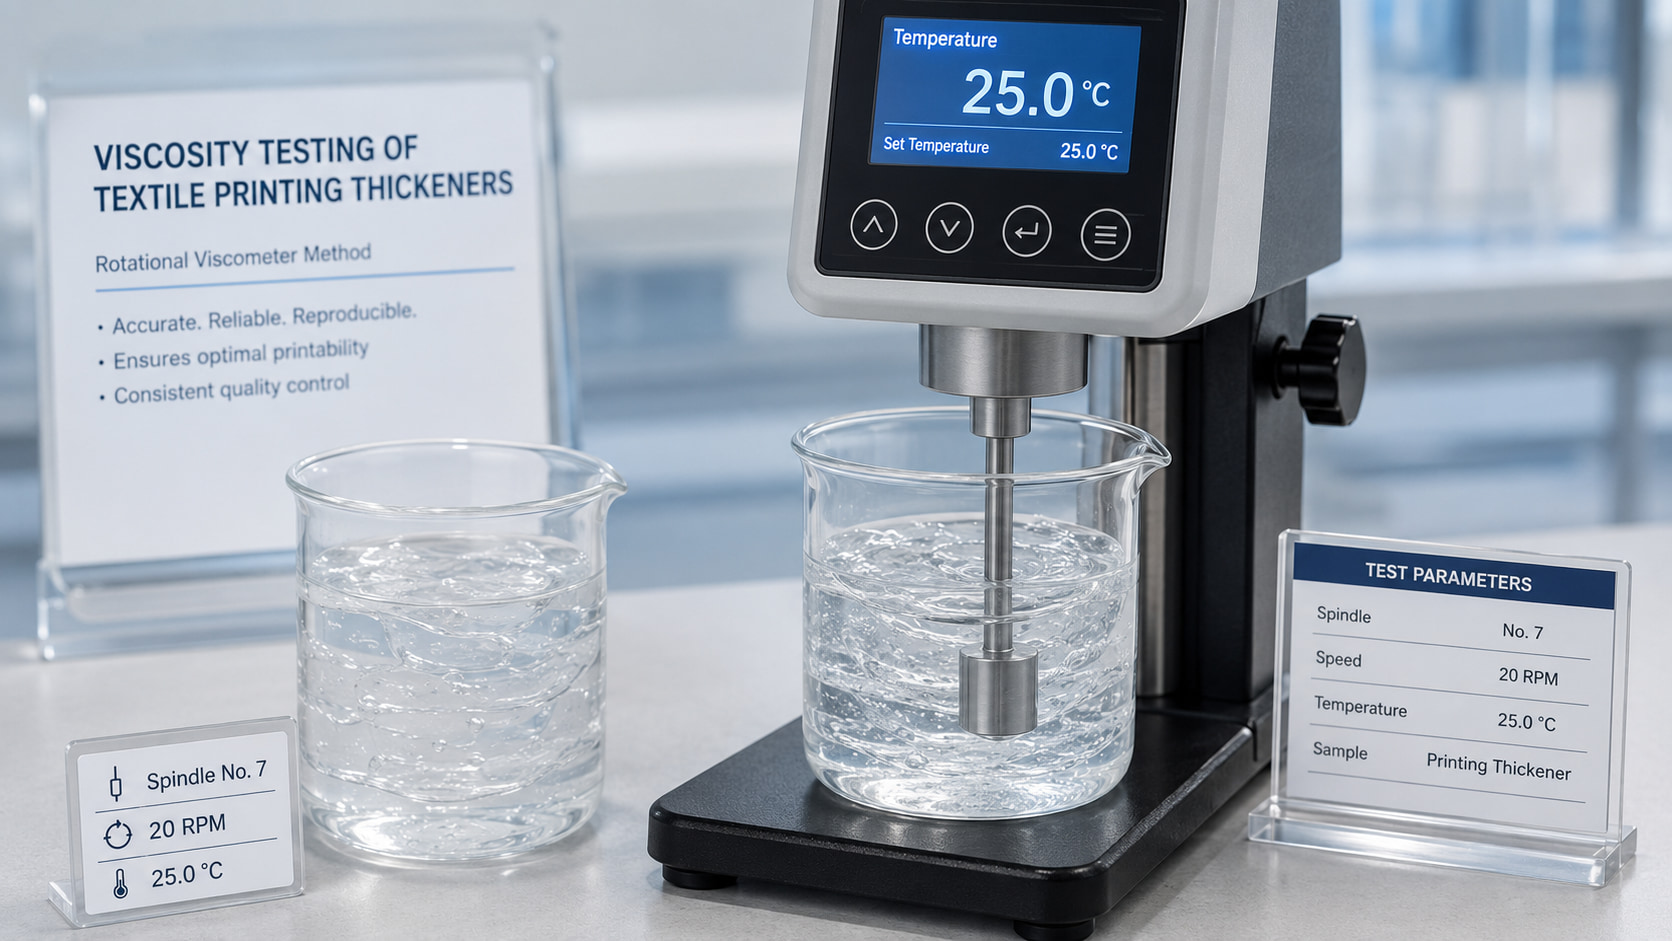
A useful viscosity-control record can include thickener batch, stock concentration, hydration time, water source, stock viscosity, dye identity and dosage, salt identity and dosage, alkali identity and dosage, final pH, paste temperature, final viscosity, holding-time viscosity and viscometer/spindle/RPM.
For a recurring problem, add one column after each critical formulation stage.
This turns viscosity troubleshooting from an operator impression into a traceable process.
Foydalanishdagi umumiy xarajat
A viscosity drop can create unnecessary cost if the response is simply to add more thickener.
Possible hidden costs include extra thickener, longer hydration or mixing, poor screen transfer, higher wash-off load, shade correction and rework.
A useful framework is:
Cost per accepted m² = allocated monetary costs of recipe inputs, preparation, printing, fixation, washing and rework ÷ accepted fabric area. Use actual supplied-product consumption × current delivered price for chemical costs. State water, energy, labor and disposal allocations in the same currency and boundary. Keep efficiency or capacity as separate operating indicators unless explicitly priced; do not charge the same rejected output or material loss twice.
Sometimes the cheapest solution is not a higher-viscosity grade. It may be a better salt-tolerant grade, a corrected dilution calculation, a different addition order, temperature-controlled viscosity testing or a compound-thickener route.
The correct solution is the one that keeps the complete paste inside a stable production window.
Qalinlashtiruvchi yetkazib beruvchiga qanday ma'lumotlarni yuborishingiz kerak?
If your printing paste loses viscosity after dye, salt or alkali is added, send:
Current thickener name/TDS/sample
Thickener concentration
Stock viscosity and complete test method
Dye class and commercial product
Dye dosage and dissolution/dispersion method
Amount of water introduced with the dye
Salt identity and dosage
Alkali identity and dosage
Oxirgi pH
Water hardness/conductivity where relevant
Addition sequence
Paste temperature
Vaqtni ushlab turish
Yakuniy viskozlik
Printing route and current defect
FSX Chemical ushbu ma'lumotlardan orqali foydalanishi mumkin Namunalar va mos mahsulot tanlash to identify whether the next trial should focus on thickener grade, dosage, salt tolerance or formulation sequence.
How Should a Mill Diagnose a Printing-Paste Viscosity Drop?
A practical decision chain is:
Verify Measurement → Calculate Dilution → Condition Temperature → Add Components Separately → Measure Salt/pH Response → Hold → Print → Approve Final Formula
Dye addition can reduce viscosity simply by diluting the polymer concentration.
Monovalent salts can reduce the effective hydrodynamic size of anionic polymer chains through charge screening.
Alkali changes both pH and ionic strength, so the two effects should not be confused.
Dyes and commercial dispersions can introduce salts, solvents and auxiliary chemistry in addition to color.
Calcium and other multivalent ions can create the opposite response—viscosity increase, association or gelation.
The final acceptance standard is complete-paste printing performance, not restoration of the original stock-paste viscosity.
Ko'p beriladigan savollar
1. Why does printing paste viscosity drop after adding dye?
The dye addition may dilute the thickener, add electrolytes or change pH and temperature. Use a water-only dilution control to separate dilution from dye-package chemistry.
2. Why does salt reduce thickener viscosity?
For many anionic thickeners, dissolved ions screen repulsion between charged polymer segments, allowing chains to contract and reducing hydrodynamic volume and apparent viscosity.
3. Does salt always reduce printing paste viscosity?
No. Response depends on polymer and ion type. Multivalent ions such as calcium can increase alginate association and eventually cause gelation.
4. Why does alkali reduce paste viscosity?
Alkali can change both pH and ionic strength. The effect depends on thickener chemistry, alkali type, concentration, water and formula.
5. Does a viscosity drop mean the thickener has degraded?
Not necessarily. Dilution, ionic screening and temperature can create a reversible or formulation-dependent viscosity decrease without polymer degradation.
6. Should I add more thickener after dye makes the paste thinner?
Only after identifying the cause and checking actual printing performance. Restoring the stock-paste viscosity can produce excessive polymer solids or unsuitable rheology.
7. How can I tell whether dilution is the cause?
Use equal portions of uniform stock and a control receiving reference water equal to the total mass of the commercial dye addition. Match final mass, thickener concentration, temperature, mixing and elapsed time, and record pH. A similar viscosity change is consistent with dilution contributing; it does not prove a dominant mechanism or exclude offsetting chemistry.
8. Why can the same thickener tolerate one dye better than another?
Commercial dyes can differ in electrolyte level, pH, dispersants, solvents and other formulation components.
9. Why does viscosity drop after high-speed mixing?
The paste may have warmed, undergone shear thinning or not yet recovered its structure. Condition the sample and remeasure after a defined recovery time.
10. Can hard water make the response worse?
Yes. Calcium and magnesium add ionic complexity, and calcium can strongly associate with sodium alginate. Compare plant water with a controlled reference water.
11. What is the best way to find which ingredient causes the drop?
Prepare the formula in stages and measure after water dilution, dye, salt, alkali and remaining auxiliaries separately.
12. What should I send FSX Chemical for viscosity-loss troubleshooting?
Send the current thickener, concentration, viscosity method, dye, salt, alkali, water, addition order, temperature, holding time and the viscosity after each stage if available.
Find the Real Cause Before Adding More Thickener
If your printing paste loses viscosity after dye, salt or alkali is added, FSX Chemical can help determine whether the cause is dilution, electrolyte sensitivity, pH, water quality, temperature or the thickener grade itself.
For a useful technical comparison, send:
Your current thickener sample, TDS or COA
Stock concentration and viscosity
Complete viscosity test method
Dye class, product and dosage
Dye dissolution/dispersion method
Water added with the dye
Salt type and dosage
Alkali type and dosage
Oxirgi pH
Plant-water information
Qo'shimcha buyurtma
Paste temperature
Vaqtni ushlab turish
Viscosity after each critical stage where available
When printing paste becomes thinner after dye, salt or alkali is added, do not correct the number first. Identify whether the paste was diluted, ionically screened, chemically shifted or simply measured under different conditions—then optimize the complete printing system.
To'qimachilik bosib chiqarish uchun qalinlashtiruvchining viskozitet qiymatlari konsentratsiya, harorat, asbob, mil, tezlik, tayyorlash usuli va sinov vaqti mos kelmasa solishtirilmasligini o'rganing.
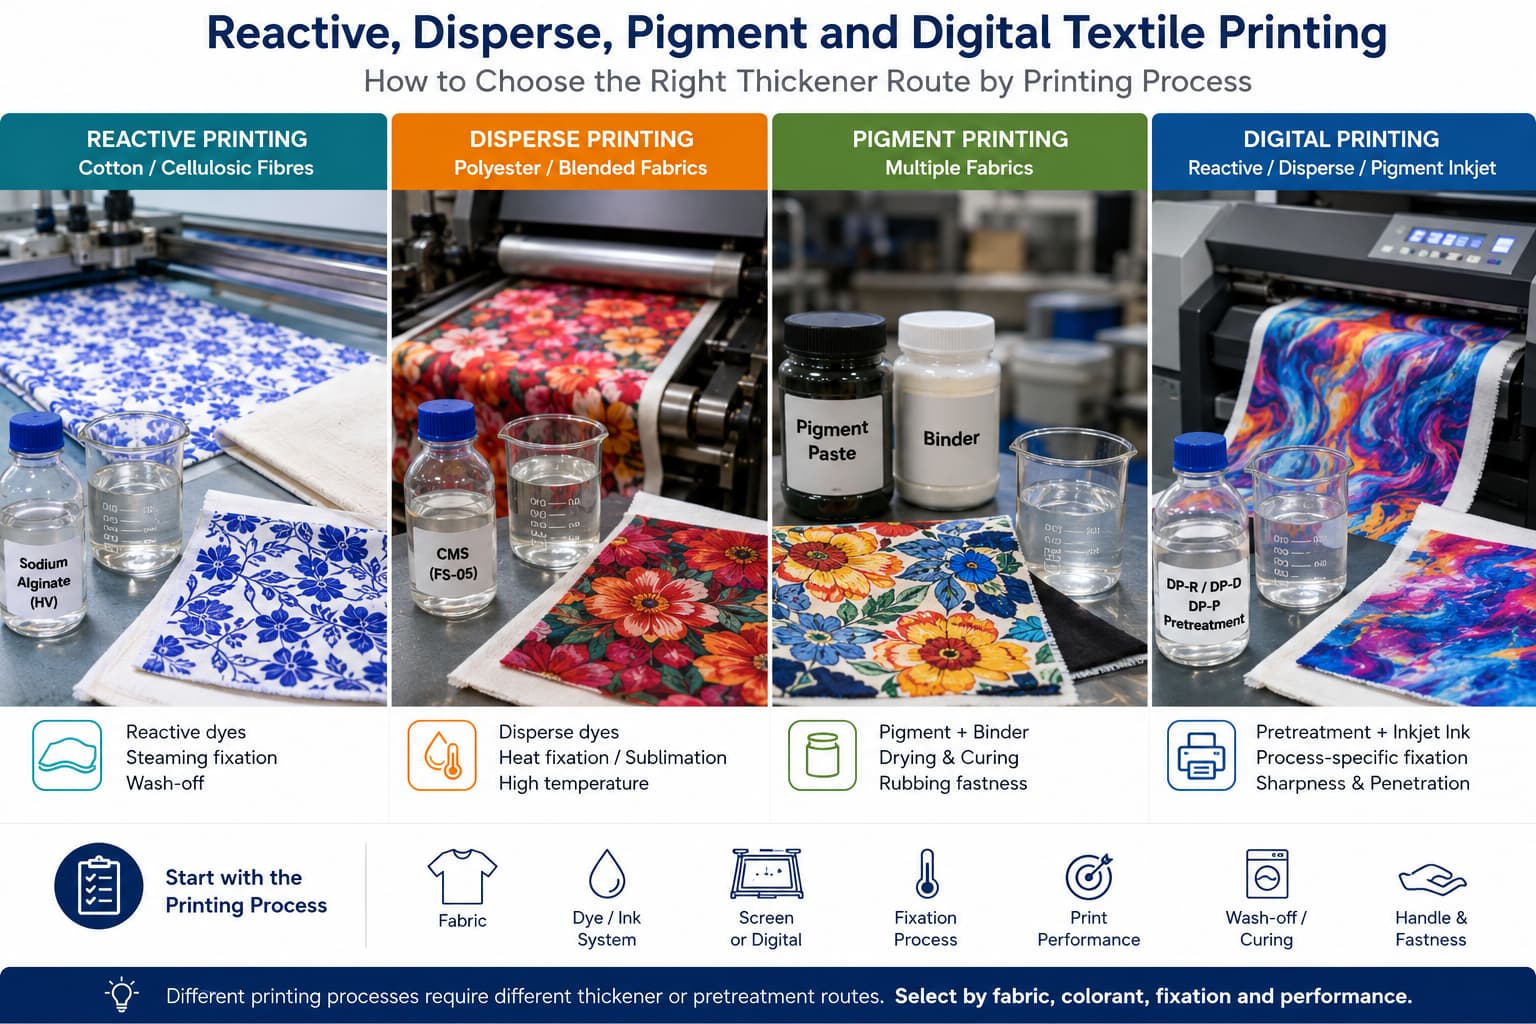
Mato, bo'yoq yoki siyoh, fiksatsiya, yuvib tashlash va bosib chiqarish sifati talablariga asoslanib reaktiv, dispergatsion, pigment va raqamli to'qimachilik bosib chiqarish uchun qalinlashtiruvchi va oldindan ishlov berish usullarini qanday tanlashni o'rganing.
To'qimachilik bosish uchun CMC, CMS, natriy alginat va raqamli bosish pastalarini solishtiring. Har bir usul reaktiv, dispers, pigment va raqamli jarayonlarga qanday mos kelishini hamda xaridorlar namuna sinovi, toifa mosligi va katta miqdorda xarid qilishdan oldin nima tekshirishlari kerakligini o'rganing.
Natriy alginati reaktiv bosma pastaning barqaror va yuviladigan qalinlashtiruvchisi sifatida to'qimachilik bosishda keng qo'llaniladi. Sotib olishdan oldin viskozlik darajasi, tozaligi va qo'llashga yaroqliligini qanday baholashni hamda FSX Chemical kompaniyasining global xaridorlarga texnik ma'lumotlar va namuna taqdim etish orqali qanday ko'maklashishini o'rganing.
Choose CMC for textile printing by application, DS, viscosity method and formulation trials. Use a practical checklist to compare grades before bulk purchase.
Karboksimetil sellyuloza suv asosidagi siyohlar, gravür bosib chiqarish va inkjet oldindan ishlov berishda qalinlashtiruvchi va barqarorlashtiruvchi sifatida ishlatiladi. Ushbu qo'llanma xarid guruhlari uchun asosiy toifa parametrlari va ta'minot manbalarini tanlash bo'yicha masalalarni o'z ichiga oladi.
Natriy alginat hamda CMC mato bosishda qalinlashtiruvchi moddalar sifatida ishlatiladi, ammo ular turli bo'yoq tizimlari va jarayon sharoitlariga mos keladi. Ushbu qo'llanma asosiy farqlarni va har birini qachon qo'llashni tushuntiradi.
Matolarga raqamli inkjet bosib chiqarish sitach bosib chiqarishga nisbatan turli xil xamir va oldindan ishlov berish talablariga ega. Ushbu qo'llanma natriy alginatning raqamli matobop bosib chiqarishda qanday qo'llanilishini va xarid guruhlari qaysi darajadagi parametrlarni belgilashi kerakligini tushuntiradi.
Oziq-ovqat va sanoat darajasidagi CMC asosiy kimyoviy tarkib jihatidan bir xil bo'lsa-da, ularning tozaligi, DS diapazoni va tartibga soluvchi talablari jihatidan sezilarli farqlarga ega. Ushbu qo'llanma asosiy farqlarni va noto'g'ri darajadagi mahsulotni ishlatish ishlab chiqarishda qanday muammolarni keltirib chiqarishini tushuntiradi.
Prepare sodium alginate printing paste with a grade-specific concentration and controlled powder dispersion. Validate hydration, viscosity, filtration, air removal and holding time before production.
Assess sodium alginate in reactive-printing wastewater using measured COD load, product-specific biodegradation evidence and controlled process comparisons. Includes a buyer checklist and illustrative load calculation.
Reaktiv bo'yoq bilan bosishda bo'yoqni mahkamlash darajasi to'g'ridan-to'g'ri rang hosil bo'lish miqdoriga, yuvilish barqarorligiga va chiqindi suvlar hajmiga ta'sir qiladi. Ushbu qo'llanma natriy alginat bo'yoqni mahkamlashni qanday qo'llab-quvvatlashini, qanday xamir parametrlari mahkamlash darajasiga ta'sir qilishini va ishlab chiqarishda mahkamlash darajasi past bo'lganda muammolarni qanday bartaraf etishni tushuntiradi.
Mahsulot nomi, qo‘llanish sohasi, miqdori, yetkazib berish manzili hamda mavjud TDS, namuna surati yoki hujjatni yuboring. FSX Chemical ma’lumotlarni ko‘rib chiqib, narx taklifi, mos namuna yoki mahsulot tanlash uchun keyingi qadamni tavsiya qiladi.
Mahsulot haqida ma'lumotMahsulot nomi, markasi, modeli, yorliq surati yoki yetkazib beruvchi ma’lumoti.
Mavjud hujjatlarTDS, SDS, COA, namuna surati, mahsulotlar ro‘yxati yoki sinov ma’lumotlari.
Buyurtma tafsilotlariTaxminiy miqdor, qadoqlash, yetkazib beriladigan mamlakat, port yoki savdo sharti.
Qo‘llanish sohasi yoki muammoMatoga gul bosish jarayoni, retseptura talabi, amaldagi muammo yoki maqsadli natija.