Choose sodium alginate for reactive printing by fiber chemistry, fabric construction, printing method and full paste behavior. Fabric type changes absorbency and penetration, but it does not create one universal viscosity grade for cotton, viscose, linen or blends. Approve the grade using a documented viscosity method and a controlled print, fixation and wash-off trial.
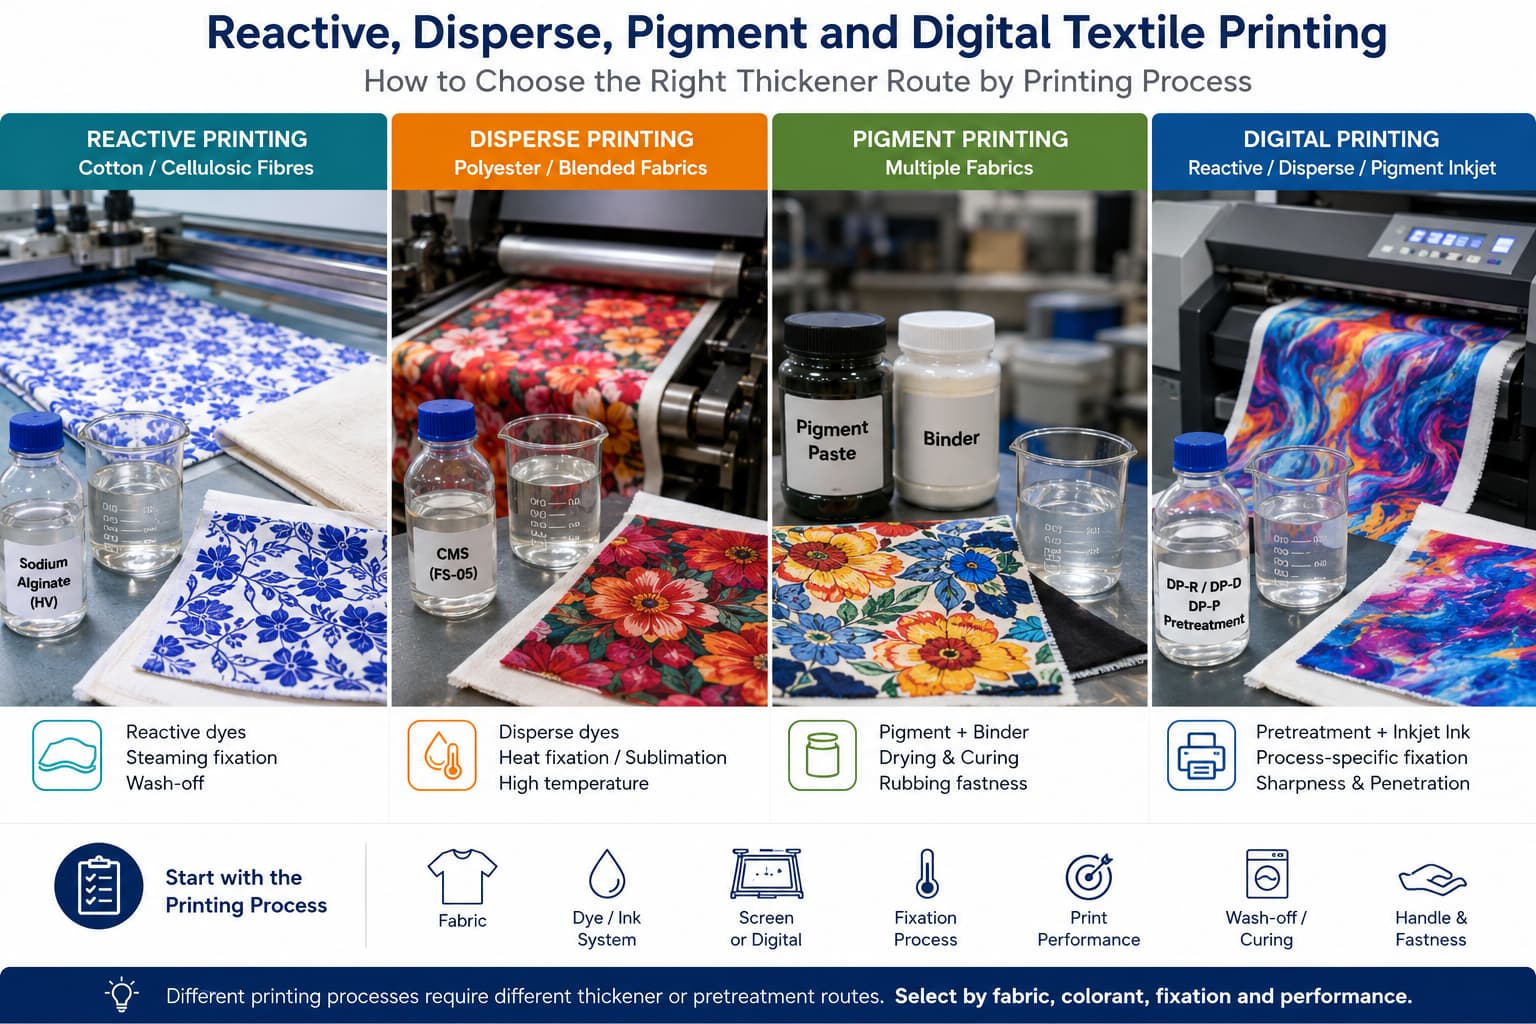
Sodium alginate is a common thickener for reactive printing on cellulosic fabrics. Start by confirming the dye route: cotton, viscose, linen and cellulosic portions of blends may be suitable; polyester portions require a separate disperse or pigment route.
Fabric Route and Trial Priorities
| Mato | First route decision | Trial priorities |
|---|---|---|
| Paxta | Reactive printing candidate | Fabric pretreatment, viscosity, outline, fixation and wash-off |
| Viscose or lyocell | Reactive printing candidate | Absorbency, pickup, penetration, shade and handle |
| Linen or ramie | Reactive route after fabric-specific trial | Construction, surface irregularity, penetration and outline |
| Cotton/polyester blend | Two-fiber color strategy required | Reactive portion plus separate disperse/pigment requirements |
| Coated or finished fabric | Check surface treatment first | Wetting, compatibility, adhesion or fixation and final fastness |
Why Fabric Type Affects Sodium Alginate Selection
Fiber Structure and Dye Uptake
These differences in dye uptake translate into different paste formulation requirements. A paste optimized for cotton may not perform identically on viscose or linen, even when the same dye class and steaming conditions are used.
How Fabric Weight and Construction Affect Paste Requirements
Fabric weight, construction, pretreatment and absorption affect paste transfer and penetration. Compare candidate grade-concentration combinations on the actual fabric rather than deriving a fixed viscosity from weight or weave alone.
Account for fiber type and fabric construction when designing the trial, but do not require different viscosity targets solely because one cotton fabric is lighter or heavier than another. Compare the candidate grade and concentration on each actual fabric at a documented viscosity method. Keep the dye system and preparation controlled, then inspect deposition, penetration, outline, fixation and wash-off before changing a working specification.
Sodium Alginate for Cotton Printing
Why Cotton Is the Primary Application for Reactive Dye Printing
Cotton is a major substrate for reactive textile printing. Cellulose structure, accessible hydroxyl groups, fabric preparation and moisture during fixation influence dye uptake and reaction. The required paste behavior still needs to be established for the actual fabric and process; the fiber category does not prove that a commercial alginate grade is already optimized for that application.
For reactive printing on cotton, sodium alginate is a widely used candidate because it generally has low interaction with many reactive dyes compared with more reactive hydroxyl-rich thickeners. FAO’s alginate chapter describes this as minimal reaction, not a universal inertness guarantee. Confirm the actual dye, alkali, water, holding time, fixation and washing conditions. Alginate selection alone does not establish preserved dye availability or a particular final color yield.
Set Viscosity by Test Method and Fabric Construction
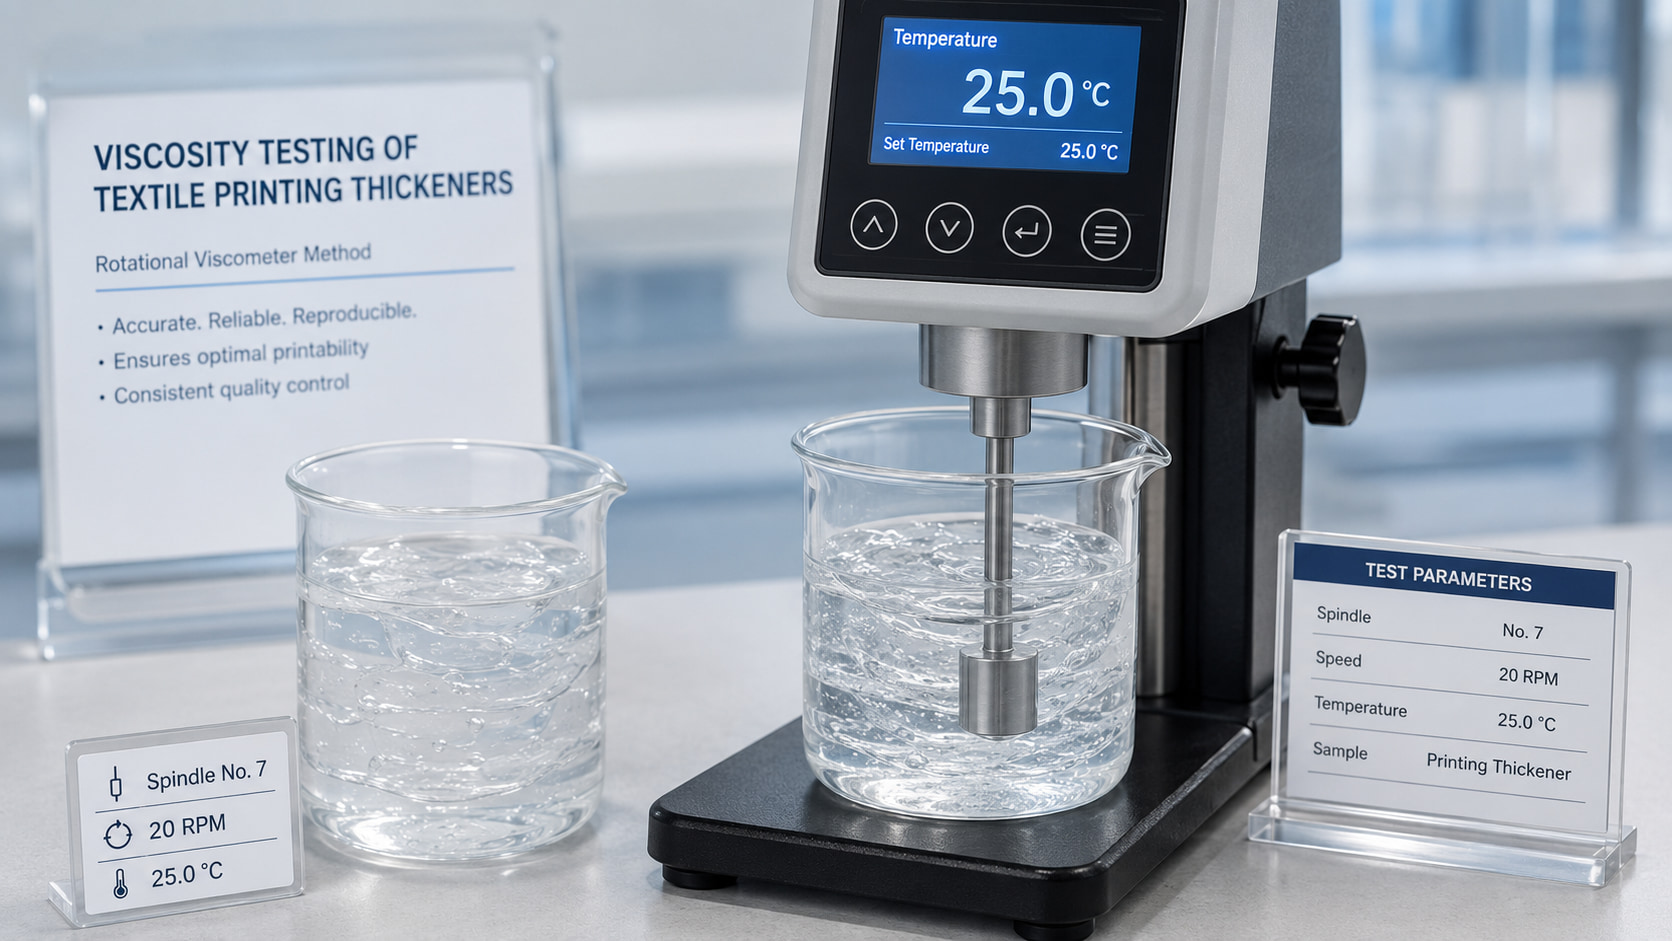
Do not apply a universal 8,000–20,000 mPa·s target. Define viscosity together with solution concentration, water, hydration time, temperature, instrument, spindle and speed. Then adjust paste solids against fabric weight, mesh, squeegee settings, speed, penetration and outline.
HV, MV and LV supplier labels are not comparable without their test methods. Screen candidate grades at controlled solids, then select the grade-concentration combination that gives stable preparation, filtration, transfer, fixation and wash-off.
Paste Concentration and Screen Mesh Considerations
Choose the stock-paste concentration from the commercial grade’s preparation guidance and controlled trials. Record whether a percentage describes stock paste or the complete color paste. Screen mesh, squeegee settings and shear response must be evaluated together; mesh count alone does not determine the required viscosity.
If you are switching between cotton weights — for example, from lightweight shirting to heavier twill — reassess paste viscosity and concentration even if the fiber type is the same. The interaction between paste viscosity and fabric construction can significantly affect print quality and dye penetration depth.
Sodium Alginate for Viscose and Lyocell Printing
Differences from Cotton in Dye Uptake
Viscose and lyocell are regenerated cellulosic fibers, but they should not be treated as structurally identical. Fabric preparation, construction and wet-processing behavior can differ. Confirm pretreatment, dye penetration and fixation on the actual substrate.
Do not promise a deeper shade or faster fixation merely from the fiber name. Compare matched fabrics after the complete printing, fixation and washing sequence, and adjust the process only on the basis of the measured result.
Viscosity and Concentration Adjustments for Viscose
Viscose constructions can differ greatly in weight, surface and absorbency. Use fabric-specific trials to balance outline and penetration; do not assume viscose always requires a lower viscosity than cotton.
When moving a recipe from cotton to viscose, keep the preparation method controlled and test a small concentration range. Measure pickup, print definition, penetration, post-wash shade and handle before changing the production formula.
Fixation and Washout Considerations
Set washing tension and action for the particular fabric’s wet-processing behavior. Verify both residual dye and thickener removal and inspect dimensions, surface appearance and hand. Do not shorten washing solely because the thickener is sodium alginate.
Sodium Alginate for Linen and Ramie Printing
Coarser Fiber Structure and Paste Penetration
Linen and ramie fabrics require their own evaluation of preparation, surface irregularity, construction and penetration. Do not infer lower moisture absorption or incomplete fixation from the bast-fiber category alone.
Validate steaming and moisture-control conditions for the actual fabric and reactive dye system. Higher temperature, longer steaming or more urea is not a default correction for linen; change one factor at a time and assess shade, fastness, definition and wash-off.
Grade Selection for Linen Substrates
Select the grade and concentration from trials that balance penetration with outline control on the intended linen fabric. An MV label is not a universal requirement, and supplier grade labels need a complete viscosity test method.
If you are switching from cotton to linen printing with the same paste formulation, run a fixation trial to confirm that color yield and fastness are acceptable under your standard steaming conditions. Adjustments to steaming time, alkali concentration, or urea content may be needed before production.
Sodium Alginate for Blended Fabrics
Cotton-Polyester Blends
In a conventional cotton-polyester reactive-printing route, the reactive dye primarily colors the cellulosic portion. Do not expect that route alone to provide the required shade and fastness on polyester. Define the color strategy for both fiber components before selecting the paste.
Check whether differential coloration is an intended design effect or a defect. Trial the complete blend and, where useful, reference fabrics for each component; do not adjust dye concentration from the fiber percentage alone.
If both cotton and polyester need coloration, evaluate a suitable disperse/reactive or pigment strategy with the appropriate fixation and post-treatment sequence. Compatibility must be demonstrated for the combined process.
Cotton-Viscose Blends
Cotton-viscose blends are common in apparel fabrics, particularly for softness and drape. Both fibers are cellulosic and reactive with reactive dyes, but their different dye uptake rates can result in differential color depth between fiber types at the same dye concentration and fixation conditions.
For cotton-viscose blends, check shade balance, penetration and final fastness on the actual construction. A recipe approved on one reference fabric should not be assumed equivalent on every blend.
Challenges of Printing on Multi-Fiber Substrates
Multi-fiber blends introduce complexity because each fiber type responds differently to the same paste formulation, dye concentration, and fixation conditions. When developing paste formulations for new blend substrates, it is worth running color yield and fastness trials on each fiber type separately (if reference fabrics are available) before printing on the blend, to understand the baseline behavior of each component.
For blends, evaluate thickener grade, concentration, dye system and fixation together. Confirm the required performance after the complete process rather than assuming that only dye concentration needs to change.
Summary: Grade Selection Parameters by Fiber Type
- Cotton: compare grade and concentration on the actual fabric using a defined method and validated steaming and washing conditions.
- Viscose / Lyocell: evaluate each fabric separately for application uniformity, penetration, shade, washing behavior and hand.
- Linen / Ramie: check preparation, surface and construction; validate fixation rather than automatically increasing heat or urea.
- Cotton-Polyester blend: define how both fiber components will be colored, then validate the complete printing and fixation sequence.
- Cotton-Viscose blend: evaluate shade balance and final quality on the actual blended fabric.
Ko'p beriladigan savollar
Is one sodium alginate viscosity suitable for every cotton fabric?
No. Fabric weight, construction, absorbency, screen, speed and design change the required paste rheology. Use a documented viscosity method and print trial.
Does viscose always need a lower-viscosity paste than cotton?
No. Viscose constructions vary. Compare controlled concentrations and evaluate pickup, penetration, outline, post-wash shade and handle.
Can sodium alginate print the polyester part of a cotton/polyester blend?
Reactive dye targets the cellulosic portion. The polyester portion requires a compatible disperse or pigment route and a combined process trial.
How should HV, MV and LV grades be compared?
Match solution concentration, water, hydration, temperature, instrument, spindle and speed. Then compare filtration and complete printing performance.
What should be supplied for fiber-specific grade matching?
Send fabric composition and weight, dye route, printing method, current grade and dosage, full viscosity method, fixation and wash-off conditions through Namunalar va mos mahsulot tanlash.
How FSX Chemical Supports Fiber-Specific Applications
FSX Chemical supplies HV, MV and LV sodium alginate grades for reactive textile printing. The TDS should define viscosity with its test conditions; sodium alginate does not use the CMC degree-of-substitution specification.
Keyingi qadamlar:
Texnik jamoamiz bilan bog'laning — share fabric composition, construction, current paste and controlled test results for application-specific evaluation.
TDSni so'rang — review grade specifications for your target fiber type and application
Namuna so'rang — run paste trials on your specific fabric substrate before bulk ordering
Ask for Grade Matching — share your fiber type, fabric weight, and printing method for a specific recommendation
📧 Elektron pochtaService@fsxchemical.com