Incoming QC Specifications for Textile Printing Thickeners: What Should You Test on Every Batch?
Incoming QC should confirm that each thickener batch matches the approved commercial specification before production....
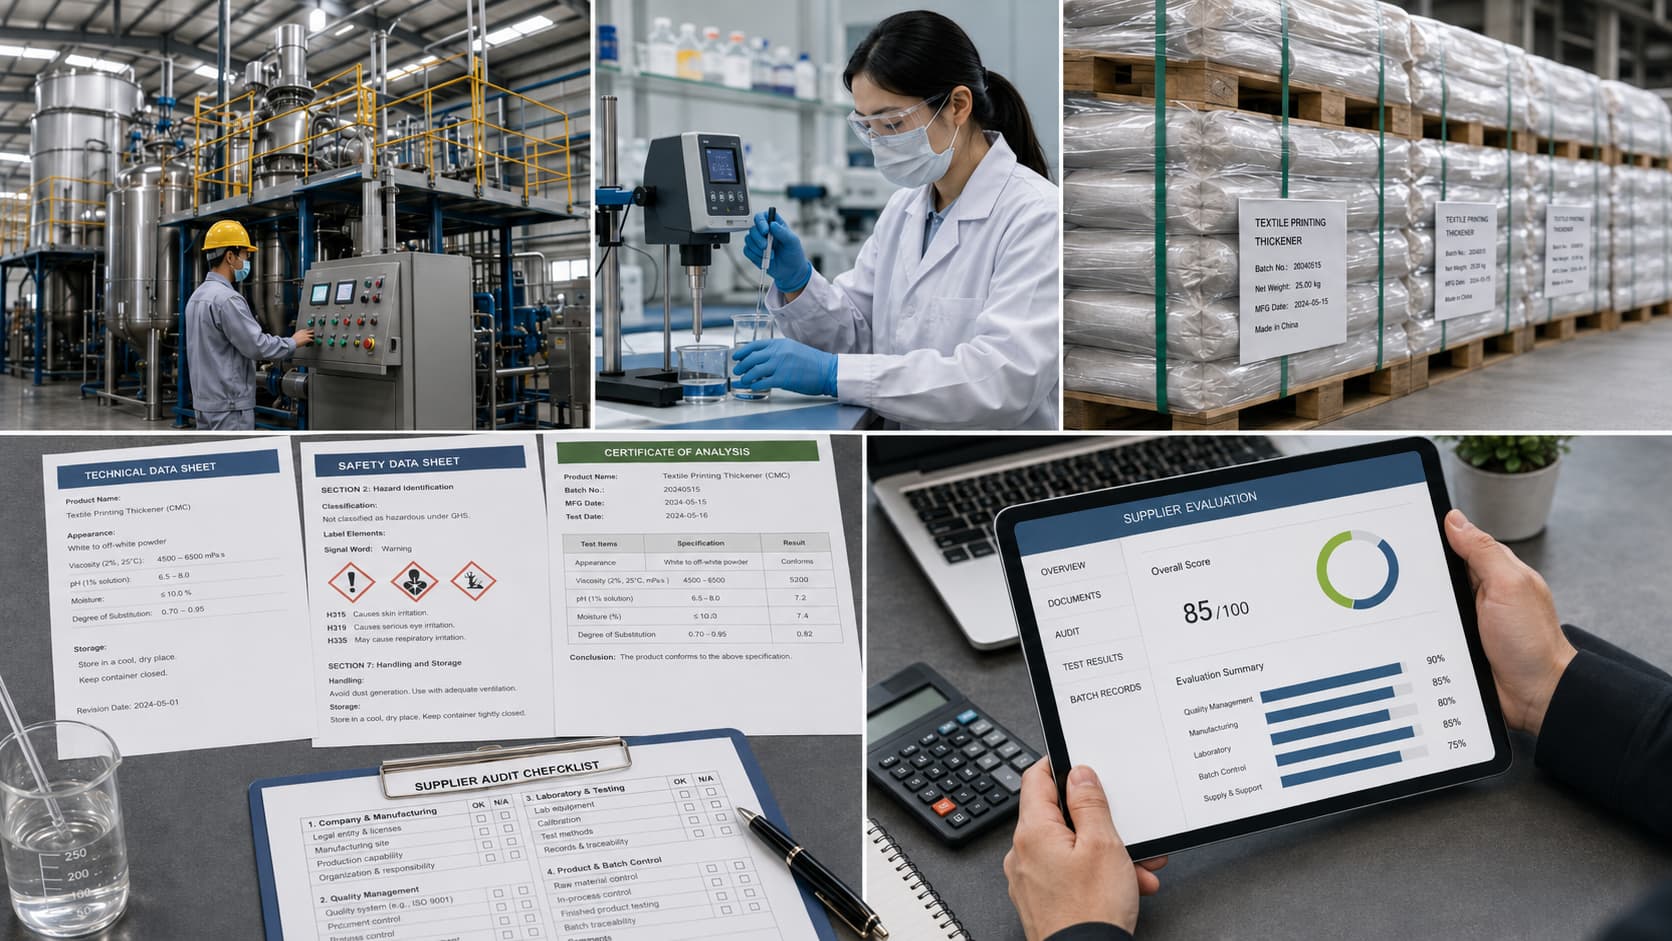
Incoming quality control for textile printing thickeners should confirm that each delivered batch matches the buyer’s agreed product specification before it enters production. The most useful every-batch checks are usually a small set of repeatable controls—batch identity and documents, appearance, standard viscosity, pH, moisture or solids, and any filtration or residue parameter that is truly critical to the mill. More complex chemistry and application tests such as degree of substitution, purity, salt tolerance, screen running, K/S and wash-off can be managed through risk-based periodic verification unless they are contractual batch-release requirements. This guide shows how to build a practical incoming QC specification for sodium alginate, CMC, CMS and formulated printing thickeners without turning every delivery into a full production trial.
What Incoming QC Should Actually Prove
Incoming QC has a narrower purpose than product development or production approval.
It should answer:
“Does this delivered commercial batch match the product and specification that our mill already approved?”
It should not try to answer every possible printing question again.
A practical incoming program separates three jobs:
Batch conformance: Is the shipment inside the agreed raw-material specification?
Preparation consistency: Does the identified product still disperse, dilute, hydrate or activate normally under its approved form-specific procedure?
Application verification: Does the approved grade continue to behave correctly in the mill’s formulation and printing route?
These jobs require different test frequencies. Testing every property on every delivery can waste laboratory time. Testing only supplier paperwork can miss batch drift.
The objective is a risk-based control plan that checks the parameters most likely to protect production.
Use Three QC Tiers Instead of Testing Everything on Every Batch
QC Tier
Typical Frequency
Purpose
Tier A
Every incoming batch / lot
Confirm identity and critical specification parameters
Tier B
Periodic, risk-based, supplier-change or trend-triggered
Verify chemistry, preparation and formulation robustness
Tier C
Initial approval, major change, repeated failure or requalification
Confirm full application and production suitability
This structure follows a basic supplier-quality principle: verification should be appropriate to the risk and the specified requirements rather than identical for every externally supplied product.
For textile thickeners, a critical reactive-printing sodium alginate grade may justify a different control intensity from a lower-risk formulated auxiliary.
Tier A: What Should Usually Be Checked on Every Batch?
For many textile printing thickeners, a practical every-batch panel includes:
Product identity / grade
Batch number and COA review
Зовнішній вигляд
Standard viscosity
pH
Moisture or solids content
Filtration / insoluble residue if this is a known production-critical parameter
The exact list should be written into the purchasing specification.
Not every item is universal. A liquid digital pretreatment may require solids content instead of powder moisture. A highly filtration-sensitive product may justify a quick filter test on every batch, while another mill may keep that test in periodic verification.
1. Product Identity, Batch Number and Documents
Before any laboratory measurement, confirm that the shipment is the product that was ordered.
Supplier name
Product / grade code
Batch or lot number
Manufacturing date where supplied
Package label
Quantity
COA
Applicable TDS / specification revision
This protects traceability. If a complaint occurs later, the mill should be able to connect:
Warehouse Lot → Supplier Batch → Incoming Test → Production Batch → Finished Fabric
2. Appearance and Physical Form
Appearance is fast and inexpensive.
For powder thickeners, inspect color, powder uniformity, visible lumps, caking, foreign matter and moisture damage.
For liquid or formulated products, inspect color or opacity, separation, sediment, skin formation, gel particles and abnormal odor where relevant.
Appearance does not prove application performance, but it can reveal packaging damage, storage problems or obvious batch abnormalities before the material reaches production.
3. Standard Viscosity — The Core Incoming Test
Viscosity is one of the most important repeat-order controls for textile printing thickeners.
But the number is meaningful only when the method is fixed.
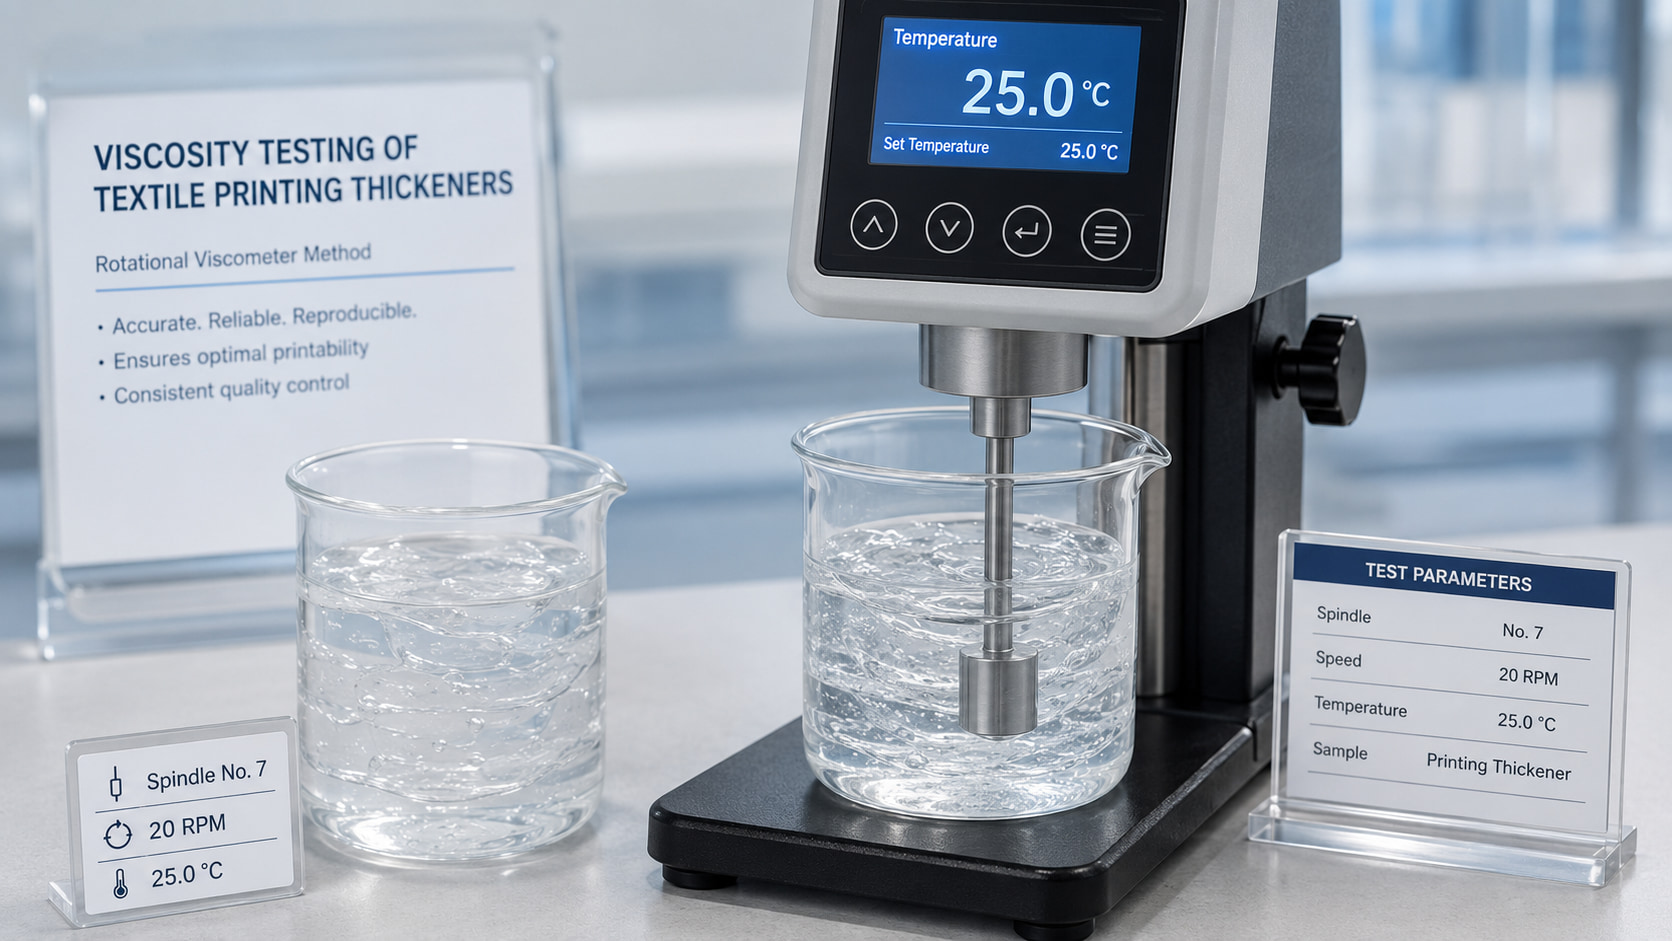
The incoming SOP should define:
Концентрація продукту
Whether concentration is as-received or dry basis
Джерело води
Sample size
Applicable powder addition, liquid dilution or activation procedure
Mixing speed and time
Grade-specific preparation endpoint and defined hydration, activation or measuring-rest time
Температура вимірювання
Viscometer / rheometer
Шпиндель, ротор або геометрія
RPM or shear-rate condition
Час читання
FSX Chemical’s current QC guidance similarly emphasizes that viscosity values cannot be compared correctly when concentration, hydration, temperature, spindle or speed differ.
A useful incoming specification is therefore:
Viscosity Range + Complete Measurement Method
not simply:
“Viscosity: 30,000.”
4. pH
pH is a useful low-cost batch indicator.
It can help detect manufacturing variation, storage change, contamination and potential compatibility differences.
For textile printing, pH can influence interaction with reactive dye systems, alkali, binders, fixers and other auxiliaries.
Measure pH using the agreed concentration and preparation method.
5. Moisture or Solids Content
For dry powder thickeners, moisture affects both quality and commercial value.
Higher measured moisture can mean less dry matter per kilogram and can accompany caking or storage change in a powder. Dry matter may include polymer, salts and other constituents; moisture alone does not quantify the active-polymer fraction. Use the agreed moisture method and declared dose basis when interpreting the change.
For a liquid or paste product, a specified nonvolatile-content test can track batch consistency. Record its temperature, heating time and calculation method. The retained mass is not automatically active thickening polymer; compare it with a separately declared component assay only where that assay actually exists.
Moisture or solids should be measured using the agreed method and compared with the approved specification.
6. Filtration / Insoluble Residue Where Process-Critical
Some textile printing routes are highly sensitive to undissolved particles, gel particles, foreign matter and insoluble residue.
These can contribute to screen blockage, filter loading, uneven paste transfer and digital pretreatment filtration problems.
If filtration performance is a recurring production risk, include a quick standardized filtration or residue check in Tier A. If it has historically been stable, it may be more efficient to keep it in Tier B periodic verification.
Tier B: What Should Be Verified Periodically or by Risk?
Tier B tests are important, but they do not always need to be repeated by the buyer on every incoming batch.
They may be checked after a supplier change, after a trend shift, after a complaint, on selected lots or according to a defined monthly or quarterly plan.
Typical Tier B items can include:
Particle size
Hydration curve
Чистота
Ступінь заміщення
Salt / alkali response
Complete-paste holding stability
More detailed filtration
Particle Size and Dissolution / Hydration Behavior
Particle size can influence powder wetting, hydration speed, dust, lump formation and mixing time.
But particle size alone does not fully predict hydration.
Two powders with similar mesh data can disperse differently because of polymer chemistry, surface condition and manufacturing process.
A useful periodic check can combine Particle Size / Mesh + Standardized Hydration Observation rather than relying on sieve data alone.
Degree of Substitution, Purity and Other Chemistry-Specific Parameters
Chemistry-specific parameters should be selected by product family.
For CMC, relevant data may include degree of substitution, purity and by-product content where specified.
For FSX CMS, start with the exact commercial synthetic-thickener grade, supplied form and current TDS. Apply only the chemistry-specific tests declared for that grade; do not infer carboxymethyl-starch chemistry or DS from the CMS family name.
For sodium alginate, purity, insoluble matter or other grade-specific chemistry may be part of the agreed specification.
These tests can require more time or specialized methods. Many mills therefore review them through supplier COA plus periodic independent verification unless the parameter is critical enough to justify buyer testing on every lot.
If a parameter is important enough to reject a batch, define the method, limit and verification responsibility before ordering.
Salt / Alkali / Complete-Paste Compatibility
A thickener can pass its water viscosity and still behave differently in the production formula.
Periodic application verification can include dye addition, salt addition, alkali addition, binder compatibility, holding-time viscosity and pH stability.
This is especially useful for new suppliers, newly approved grades, critical reactive-printing routes and products with historical electrolyte sensitivity.
Tier C: When Is Full Application Requalification Needed?
Full application testing should be triggered when risk is high.
Examples include initial supplier approval, new grade, major raw-material or manufacturing change, repeated incoming drift, serious customer complaint, unexplained printing failure or a major formula or machine change.
Tier C can include complete paste, screen or machine trial, pattern definition, penetration, K/S, fixation, wash-off, fastness and fabric hand.
This is product requalification, not normal receiving inspection.
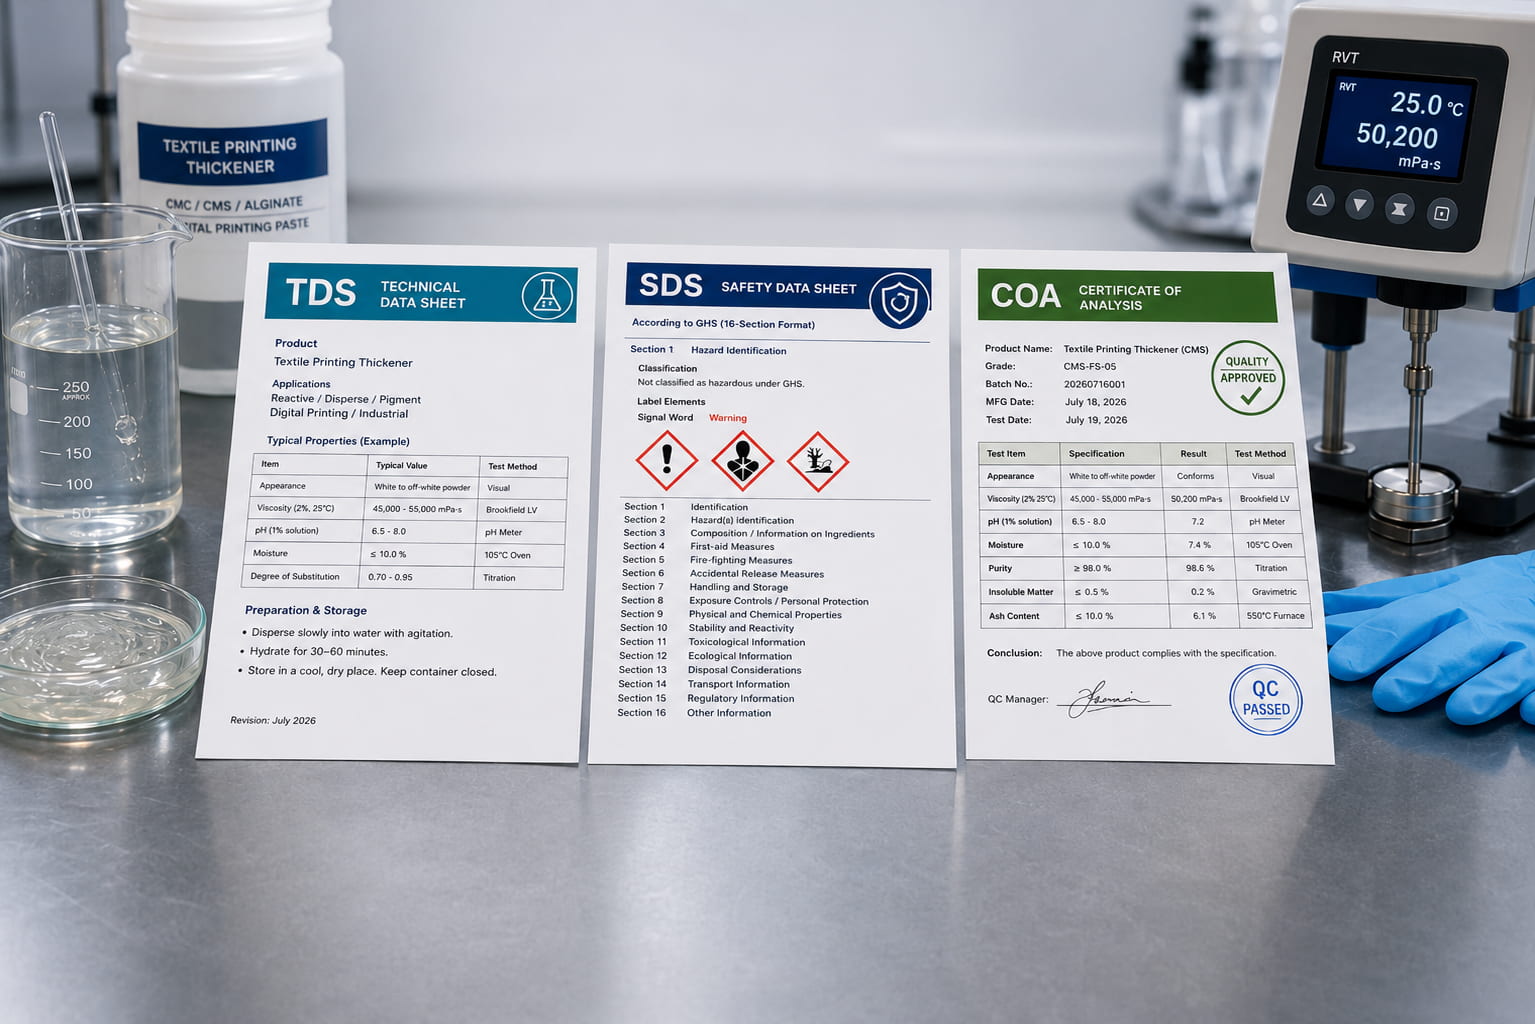
Why a COA Does Not Replace Incoming QC
A COA is valuable because it provides supplier-reported batch data and helps confirm batch identity, tested parameters, reported results and specification conformance.
But COA review and buyer verification have different roles.
COA = supplier-reported results for the identified lot, applicable specification revision and stated methods. Distinguish measured numerical results from an unqualified “pass” or a typical TDS value; a COA does not imply every possible parameter was tested.
Incoming QC = buyer acceptance evidence.
For a critical thickener, the buyer should independently verify selected high-value parameters such as viscosity, pH or moisture rather than accepting every shipment only from paperwork.
Representative Sampling: Test the Batch, Not One Convenient Bag
A precise laboratory method is useless if the sample does not represent the delivered lot.
The mill should define a sampling plan appropriate to lot size, number of packages, product homogeneity, supplier history and criticality.
For large lots, selected packages may be sampled according to the mill’s acceptance-sampling procedure. Where appropriate, a composite or representative laboratory sample can be prepared.
Do not invent an arbitrary universal “sample three bags” rule for every shipment.
Standardize the Test Method Before Setting Limits
Specification limits only work when the method is reproducible.
For each test, document sample preparation, equipment, calibration status, temperature, time, calculation basis and acceptance range.
Do not build a viscosity range using one viscometer and later judge incoming batches with another method without establishing a correlation.
The same principle applies to moisture, pH, particle size and filtration.
Build a Buyer-Owned Incoming Specification
A useful incoming specification should include four things for every controlled parameter:
Field
Example Structure
Parameter
В’язкість
Method
Defined concentration, temperature, instrument, spindle and speed
Acceptance range
Buyer-approved range
Action if failed
Quarantine / retest / supplier review
Do not copy a generic TDS range into the purchase specification unless the mill has confirmed that the range protects production.
Incoming QC for Sodium Alginate
Every Batch
Batch identity / COA
Зовнішній вигляд
Standard viscosity
pH
Вологість
Periodic / Risk-Based
Purity / insoluble matter where specified
Particle size
Фільтрація
Характеристики гідратації
Calcium / hard-water response if this is a known risk
Complete reactive-paste stability
Requalification
Screen running
K/S
Змивається
Тканина ручної роботи
FSX Chemical’s current sodium alginate guidance also identifies viscosity, moisture, pH, purity and particle-size / filtration-related properties as relevant grade-review parameters, with final application testing required separately.
Incoming QC for CMC
Every Batch
Batch identity / COA
Зовнішній вигляд
Standard viscosity
pH
Вологість
Periodic / Risk-Based
Ступінь заміщення
Чистота
Particle size
Гідратація
Salt tolerance
Фільтрація
DS can strongly influence CMC solubility, salt response and application behavior, but the buyer does not necessarily need to re-run a chemistry-level DS determination on every shipment if it is controlled contractually and periodically verified.
Incoming QC for CMS
Every Batch
Batch identity / COA
Зовнішній вигляд
Standard viscosity
pH
Moisture for a specified powder method, or nonvolatile content for a specified liquid/formulated grade
Periodic / Risk-Based
Chemistry-specific data explicitly declared for the exact commercial grade
Чистота
Powder particle-size method, or other form-specific physical checks where specified
Applicable dispersion, dilution, hydration or activation response
Salt / alkali response
Complete-paste holding stability
The FSX CMS commercial synthetic-thickener family includes grade-specific printing routes. Confirm the exact identity and form before selecting this panel; a disperse, reactive or specialty route label is not one universal composition or release specification.
Incoming QC for Digital Printing Paste / Formulated Thickeners
Every Batch
Batch identity / COA
Appearance / separation
pH
Viscosity where specified
Solids content where specified
Periodic / Risk-Based
Фільтрація
Storage stability
Interaction of the fabric-applied pretreatment with the actual ink during printing and required post-treatment
Pretreatment pickup behavior
Bleeding / color yield
For filtration-sensitive fabric-pretreatment routes, filtration may be moved into the every-batch Tier A panel. Check the actual application bath and equipment requirement. A fabric-pretreatment test does not qualify a product as a printhead-ink ingredient; that needs a separately engineered and validated ink formulation.
Trend Every Batch — Do Not Look Only at Pass/Fail
A batch can technically pass while moving steadily toward the edge of the specification.
Наприклад:
Viscosity: Center → Center → Lower → Lower → Near Lower Limit
Every batch may still be “PASS,” but the trend deserves investigation.
Track at least viscosity, pH, moisture/solids and filtration result where critical.
A simple trend chart can help identify supplier drift, seasonal raw-material variation, method drift or laboratory error.
Retained Samples and Complaint Traceability
Keep a retained incoming sample when practical, especially for critical grades, new suppliers, large lots and products with customer-specific approvals.
The retained sample should be labeled with supplier, grade, batch, receipt date and incoming QC record.
If production later fails, the mill can retest the retained material beside a known-good batch, the supplier’s retain or the complaint sample.
What to Do When a Batch Fails Incoming QC
Place the identified lot on hold and preserve the original result. A later passing result does not erase an unexplained failure. Use the mill’s documented investigation and release process rather than repeating tests until a passing number appears.
Separate preparation error from a material problem
Investigation step
Запис
Decision boundary
Identity and sampling
Bag or container references, lot, sampling locations, seals and handling
A convenient replacement sample must not silently replace the original evidence
Method review
Actual concentration basis, water, hydration, temperature, spindle, speed and instrument checks
A result from a different method is not a direct retest
Repeat measurement
Predefined reason and number of repeats, all individual readings
Distinguish re-reading one preparation from independently preparing another sample
Reference comparison
Approved retained material prepared alongside the questioned batch
If both fail, investigate the method or environment before blaming the new lot
Disposition
Evidence, risk assessment, responsible approver and scope
Production cannot release a held lot merely because it needs material
Do not average away an unexplained failure
Near a specification boundary, examine repeatability, sample homogeneity and the agreed decision rule. Retain unrounded readings and report rounding consistently. Do not widen the limit after seeing the result or average results from incompatible methods. If a calculation, instrument or preparation error is demonstrated, document why the original result is invalid and how the replacement test was performed.
Keep exceptions traceable
A concession requires a documented, authorized decision and must not override a contractual or mandatory requirement. Define the approved quantity, use, extra checks and expiry of the exception. Rework or blending requires its own controlled procedure and subsequent verification; it is not a way to conceal a nonconforming lot.
Give the supplier the lot identity, specification revision, method, original readings, observations and retained-sample availability. After resolution, review whether sampling, test frequency or application requalification needs to change. The workflow is a proposed industrial QC practice, not a claim that FSX applies a particular certification standard.
Incoming QC vs. Application Verification
Incoming QC
Application Verification
Identity
Complete printing formula
Зовнішній вигляд
Стабільність утримання
Standard viscosity
Screen / machine behavior
pH
Pattern definition
Moisture / solids
K/S / відтінок
Selected filtration
Wash-off / fastness / hand
Incoming QC is faster because it protects the gate into production. Application verification is deeper because it confirms the product still works in the complete process.
How to Reduce Testing After a Stable Supply History
Testing intensity can change as supplier confidence increases.
A new supplier may start with full Tier A on every lot, frequent Tier B verification, retained samples and periodic application checks.
After a strong history, the mill may reduce selected periodic tests if incoming trends are stable, supplier COAs are reliable, complaints are low, change control is effective and application performance remains stable.
Risk-based supplier control is more efficient than either extreme: Test Everything Forever або Stop Testing Because the Supplier Has Been Good.
Incoming specification covers every application variable
Example Incoming QC Record
Field
Запис
Supplier / Grade
Approved commercial source
Batch / Lot
Supplier batch code
COA Reviewed
Yes / No
Зовнішній вигляд
Pass / observation
В’язкість
Result + method reference
pH
Result
Moisture / Nonvolatile content
Applicable result, method and basis; not an inferred active-polymer assay
Filtration / Residue
If required
Trend Status
Normal / Watch / Investigate
Retained Sample
Reference ID
Disposition
Release / Quarantine / Reject / Concession
Total Cost in Use: Balance Inspection Cost and Failure Risk
Incoming QC has a cost in laboratory time, sampling, testing equipment and retained samples.
But a failed thickener batch can create much larger costs through color-paste waste, machine downtime, screen cleaning, reprinting, extra washing, rejected fabric and customer claims.
A useful model is:
Quality Cost = Incoming Control + Prevention + Failure Cost
The objective is a justified control effort that detects relevant batch variation before use. Compare the same production boundary and currency, and assign each charge to only one category. Count sampling and testing as appraisal, separate process-improvement work as prevention, and distinct rework, disposal or complaint charges as failure costs. Do not repeat material or downtime charges already allocated elsewhere. For different output levels, also compare cost per accepted finished-fabric area. No finite incoming panel guarantees that production failures will be prevented.
What Should Be Agreed with the Supplier Before the First Bulk Order?
Exact product / grade code
Поточний TDS
SDS
Proposed COA format
Viscosity range and complete method
pH range
Moisture / solids range
Other product-specific parameters
Packaging and storage
Batch traceability
Change-notification expectations
For a matching project, FSX Chemical can review a current sample, TDS or test condition through Зразки та підбір before a commercial specification is finalized.
What Should a Mill Test on Every Incoming Thickener Batch?
A practical decision chain is:
Identify Product → Sample the Lot → Review COA → Test Tier A → Trend Results → Release or Quarantine → Periodically Verify Tier B → Requalify with Tier C When Risk Changes
Every-batch QC should focus on a small number of critical, repeatable parameters.
Viscosity must always be tied to a complete test method.
COA review supports incoming QC but does not automatically replace buyer verification.
DS, purity, particle size and full application testing can be periodic unless contractually required on every batch.
Trend data is often more useful than a simple pass/fail record.
Incoming QC confirms batch conformance; finished printing still depends on formulation and process control.
Поширені запитання
1. What should be tested on every batch of textile printing thickener?
A practical every-batch panel often includes identity/batch documents, appearance, standard viscosity, pH and moisture or solids. Add filtration or another parameter if it is critical to the approved process.
2. Is viscosity alone enough for incoming QC?
No. Viscosity is important, but identity, pH, moisture/solids and product-specific risks should also be controlled.
3. Should degree of substitution be tested on every CMC batch?
Not necessarily by every buyer. DS can be controlled in the commercial specification and supplier COA with periodic independent verification unless the mill’s risk requires every-lot testing.
4. Should purity be checked on every sodium alginate shipment?
It depends on the agreed specification and risk. Many mills use supplier batch data plus periodic verification while independently checking faster critical items every lot.
5. Does a supplier COA mean incoming inspection is unnecessary?
No. The COA is supplier-reported batch evidence. The buyer should independently verify selected critical acceptance parameters according to its quality plan.
6. Why must the viscosity test method be fixed?
Concentration, water, hydration time, temperature, spindle and RPM can all change the reported viscosity. Limits are meaningless without a consistent method.
7. Should every batch be printed in the laboratory before release?
Usually not for a stable approved supplier. Full application testing is more efficient as periodic or risk-triggered verification unless the product is highly critical.
8. What should happen if incoming viscosity fails?
Quarantine the lot, confirm sampling and test method, repeat according to the SOP, compare with COA/reference data and agree the disposition before production use.
9. Why keep a retained sample?
It provides material for complaint investigation, repeat testing and comparison with future batches or supplier retains.
10. Why trend data if every batch already passes?
Trend data can reveal gradual supplier or method drift before the product crosses a formal rejection limit.
11. Can incoming QC be reduced for a long-term reliable supplier?
Selected verification can be reduced using risk and performance history, but critical controls and supplier monitoring should remain defined.
12. What should I send FSX Chemical to build an incoming QC specification?
Send the current product or TDS, approved viscosity method, application, dosage, key quality concerns and current supplier specification so the relevant control parameters can be reviewed.
Build an Incoming QC Specification That Protects Production
If your mill is purchasing sodium alginate, CMC, CMS or formulated printing thickeners, FSX Chemical can help align product specifications, viscosity methods and application requirements before repeat bulk supply.
Щоб отримати корисний технічний огляд, надішліть:
Ваш поточний зразок згущувача, TDS або COA
Current supplier specification
В'язкість та повна методика випробувань
Поточна доза
Printing route
Fabric and colorant system
Known salt / alkali / filtration risks
Current incoming QC items
Main batch-consistency problem
Почніть з Зразки та підбір when a current grade or specification needs to be compared.
Огляд Альгінат натрію, CMC та CMS щодо інформації про продукцію для конкретного маршруту.
The best incoming QC plan is not the one with the most tests. It is the one that detects meaningful batch variation before the thickener reaches the printing machine.
Дізнайтеся, чому показники в’язкості загущувачів для текстильного друку не можна порівнювати без урахування таких параметрів, як концентрація, температура, прилад, шпиндель, швидкість, метод підготовки та тривалість випробування.
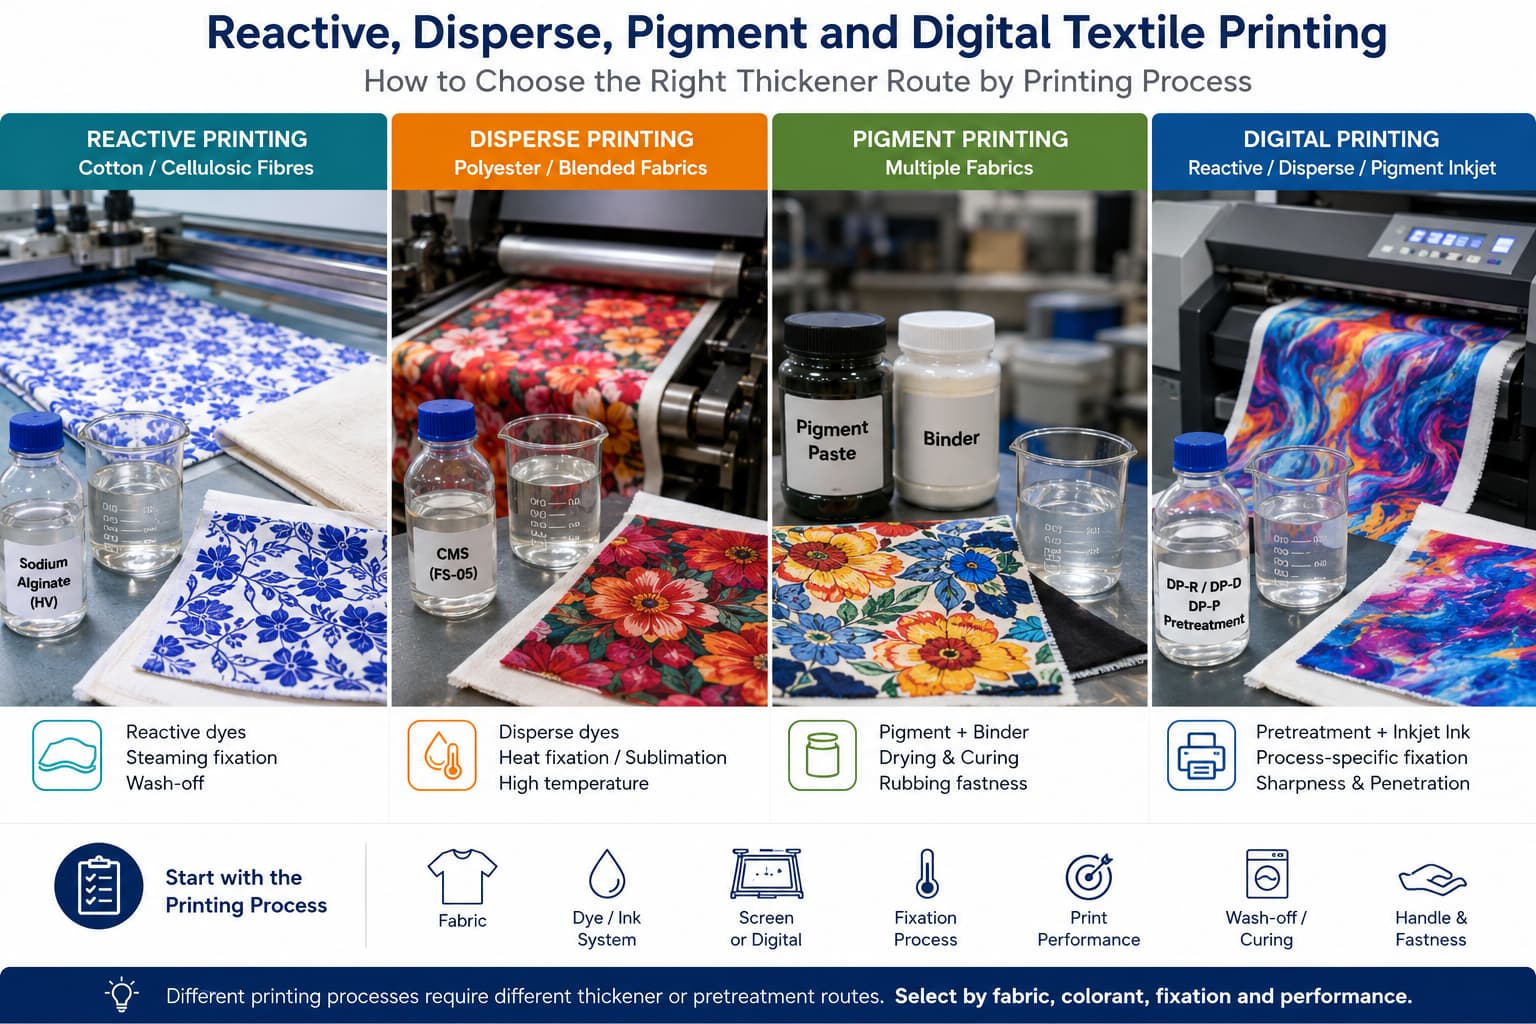
Дізнайтеся, як підібрати загущувач та методи попередньої обробки для реактивного, дисперсного, пігментного та цифрового друку на текстилі з урахуванням вимог до тканини, барвника або чорнила, фіксації, змивання та якості друку.
Дізнайтеся, у чому полягає різниця між документами TDS, SDS та COA, що саме повинні перевіряти покупці текстильних виробів із друком, а також як перевіряти технічні характеристики, дані щодо безпеки, методи випробувань, результати випробувань партій продукції та інформацію про емітентів документів.
Дізнайтеся, як оцінити виробника загущувачів для текстильного друку, перевіривши ідентифікаційні дані компанії, виробничі потужності, методи випробувань, простежуваність партій продукції, технічну документацію, можливість надання зразків та можливості експортних поставок.
Порівняйте CMC, CMS, альгінат натрію та пасту для цифрового друку на текстилі. Дізнайтеся, як кожен із цих матеріалів підходить для реактивних, дисперсних, пігментних та цифрових технологій друку, а також на що покупцям слід звернути увагу перед тестуванням зразків, підбором сорту та оптовою закупівлею.
Альгінат натрію широко використовується у текстильному друці як стабільний та стійкий до прання загущувач для реактивних друкарських паст. Дізнайтеся, як перед придбанням оцінити клас в’язкості, ступінь чистоти та придатність продукту для конкретного застосування, а також як компанія FSX Chemical надає підтримку покупцям з усього світу, надаючи технічні дані та зразки.
Choose CMC for textile printing by application, DS, viscosity method and formulation trials. Use a practical checklist to compare grades before bulk purchase.
Карбоксиметилцелюлоза використовується як загущувач і стабілізатор у водорозчинних чорнилах, глибокому друці та підготуванні до струменевого друку. Цей посібник містить інформацію про основні параметри сортів та рекомендації щодо вибору постачальників для відділів закупівель.
І альгінат натрію, і КМК використовуються як загусники в текстильному друку, але вони підходять для різних систем фарбування та умов виробництва. У цьому посібнику пояснюються основні відмінності та випадки, коли слід застосовувати кожну з цих речовин.
Цифровий струменевий друк на текстилі має інші вимоги до пасти та попередньої обробки, ніж трафаретний друк. У цьому посібнику пояснюється, як альгінат натрію використовується в цифровому текстильному друці та які параметри якості повинні вказувати фахівці з закупівель.
CMC харчового та промислового призначення мають однакову хімічну основу, але суттєво відрізняються за рівнем чистоти, діапазоном DS та нормативними вимогами. У цьому посібнику пояснюються основні відмінності та причини, через які використання неправильного сорту може спричинити проблеми у виробництві.
Prepare sodium alginate printing paste with a grade-specific concentration and controlled powder dispersion. Validate hydration, viscosity, filtration, air removal and holding time before production.
Надайте назву продукту, сферу застосування, кількість, місце призначення, а також будь-які технічні специфікації (TDS),
зразки фотографій або документів, які у вас вже є. Компанія FSX Chemical розгляне цю
інформацію та надасть рекомендації щодо подальших кроків: підготовки комерційної пропозиції, підбору зразків
або вибору продукту.
Інформація про товарНазва товару, сорт, модель, фото етикетки або код постачальника.
Доступні документиTDS, SDS, COA, фото зразка, перелік продукції або дані випробувань.
Деталі замовленняОрієнтовна кількість, упаковка, країна призначення, порт або умови торгівлі.
Заявка чи проблемаПроцес друку на текстилі, вимоги до складу, поточні проблеми або цільові показники ефективності.