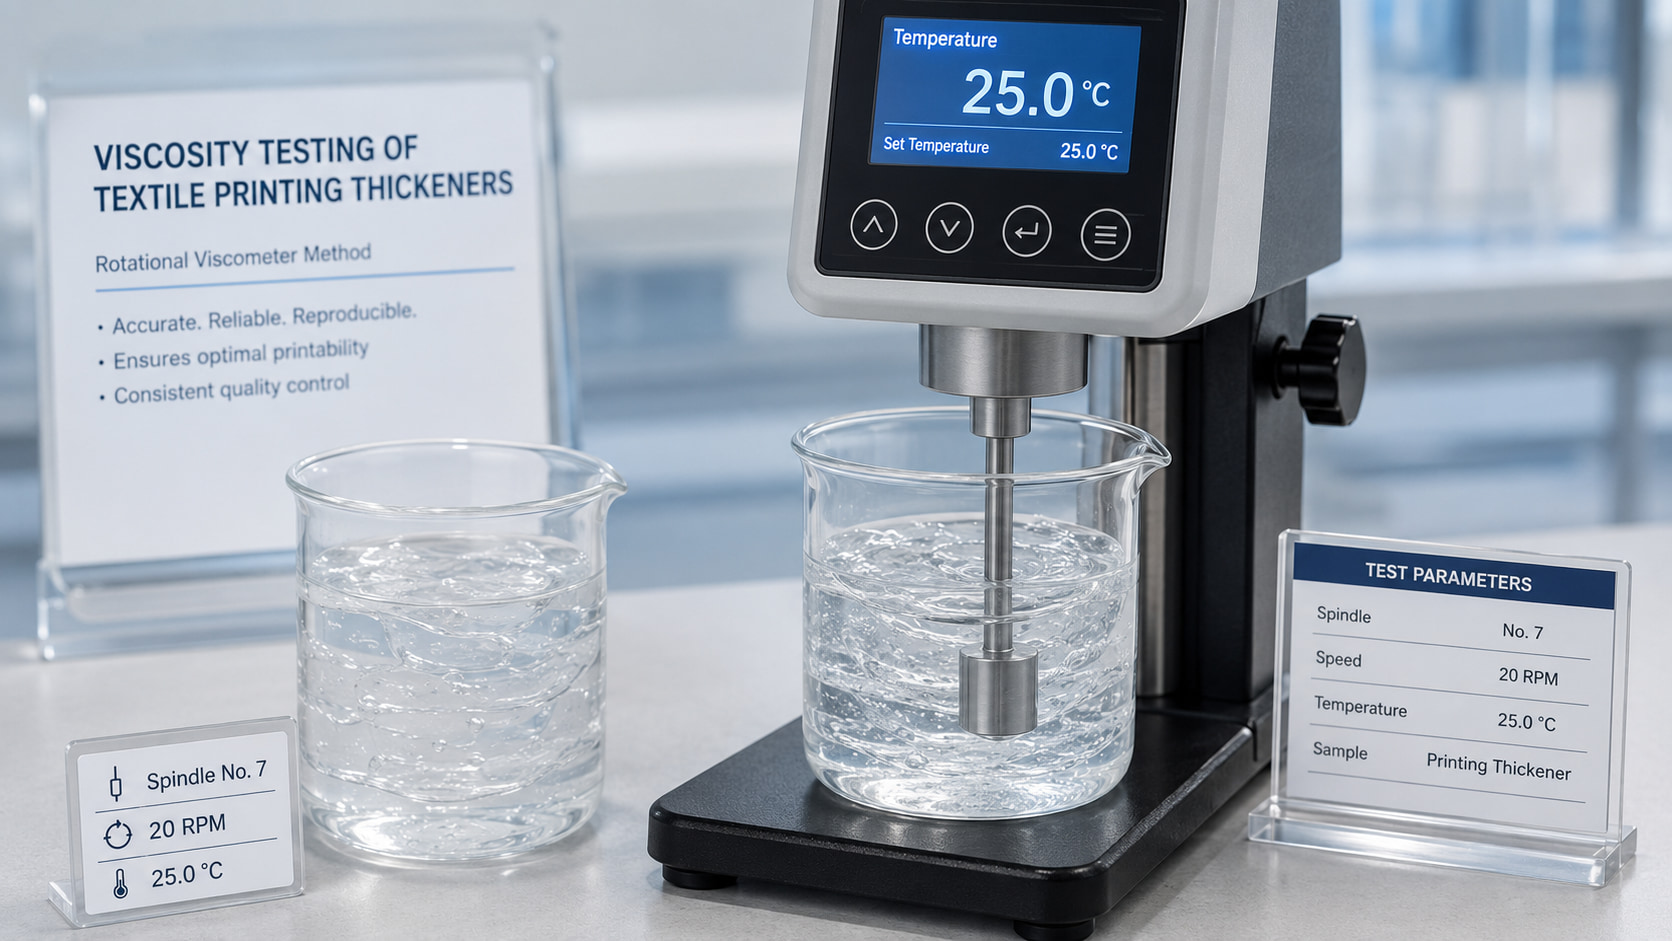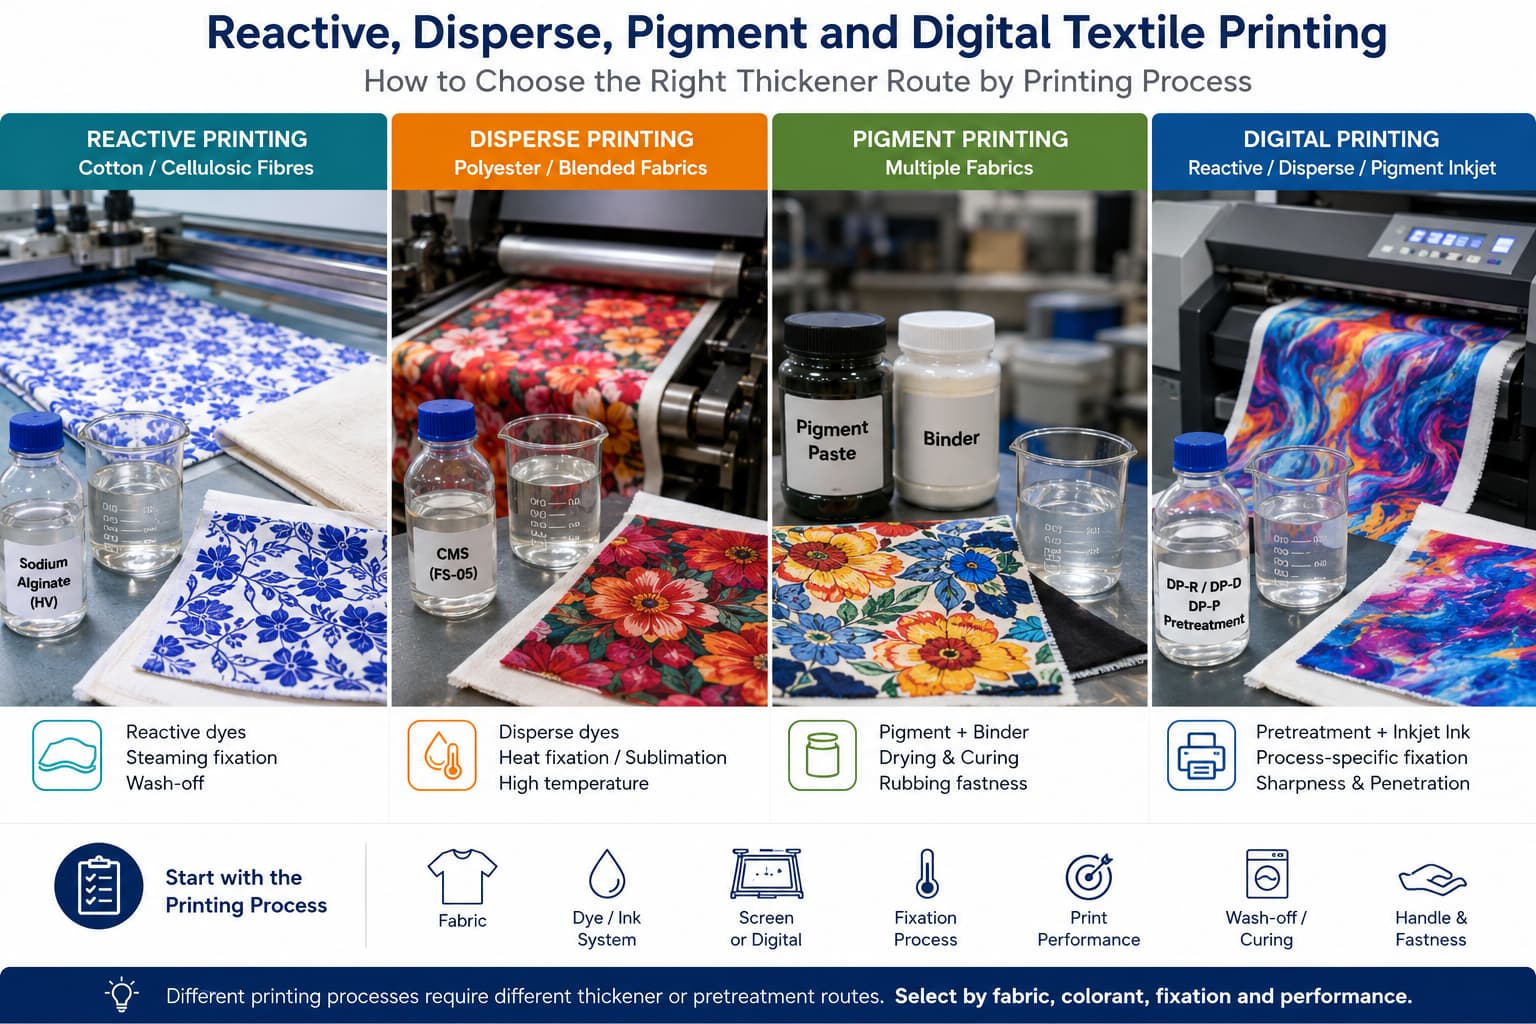
Sodium alginate paste can change viscosity as temperature, hydration, concentration, water quality and paste age change. To diagnose drift in reactive screen printing, compare timed readings under the same test conditions before adjusting the formulation. A viscosity reading alone cannot predict dye deposition or final color yield.
Viscosity Stability Diagnostic Matrix
| Observed change | First checks | Confirm with |
|---|---|---|
| Viscosity falls after preparation | Temperature, shear, dilution, pH, ions, contamination and paste age | Timed method-controlled readings and reference paste |
| Viscosity rises during holding | Incomplete hydration, evaporation, cooling and additive interaction | Covered-vessel comparison and solids check |
| Gel particles appear | Hardness or multivalent ions, local chemical shock, poor dispersion | Water analysis, addition-order trial and filtration |
| New lot reads differently | Sample preparation, moisture, instrument and batch variation | Retained sample, COA and side-by-side test |
| Print changes while viscosity appears stable | Rheology, pickup, screen, fabric, fixation or wash-off | Production trial and final fabric evaluation |
Why Viscosity Stability Matters in Reactive Dye Printing
How Viscosity Variation Affects Print Quality
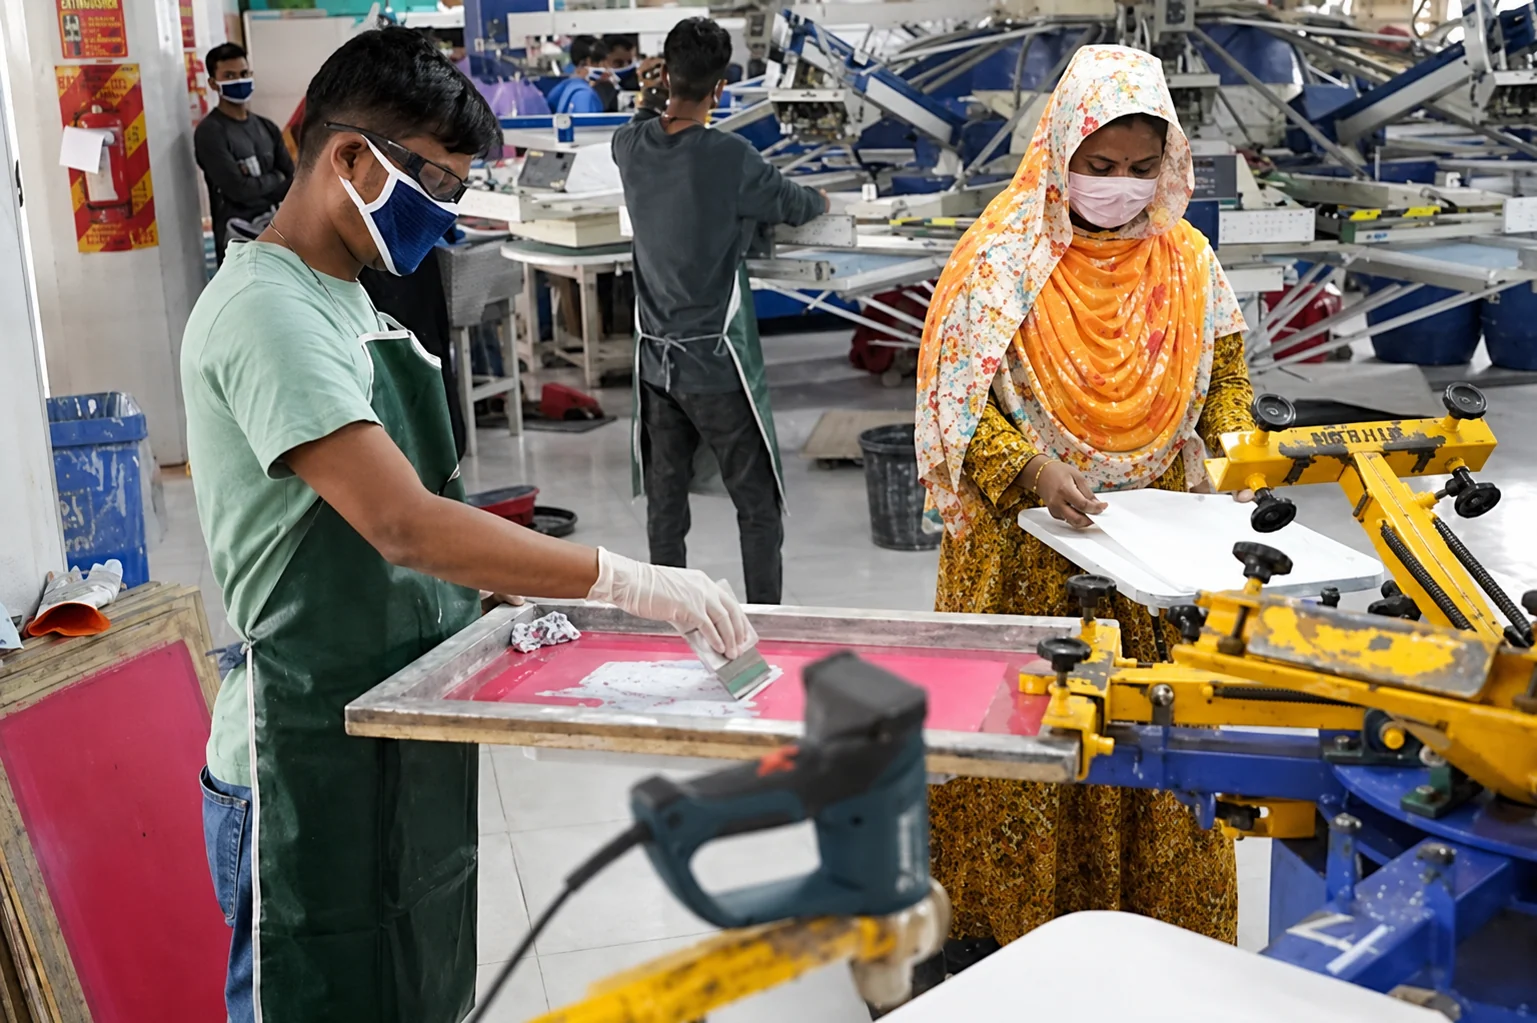
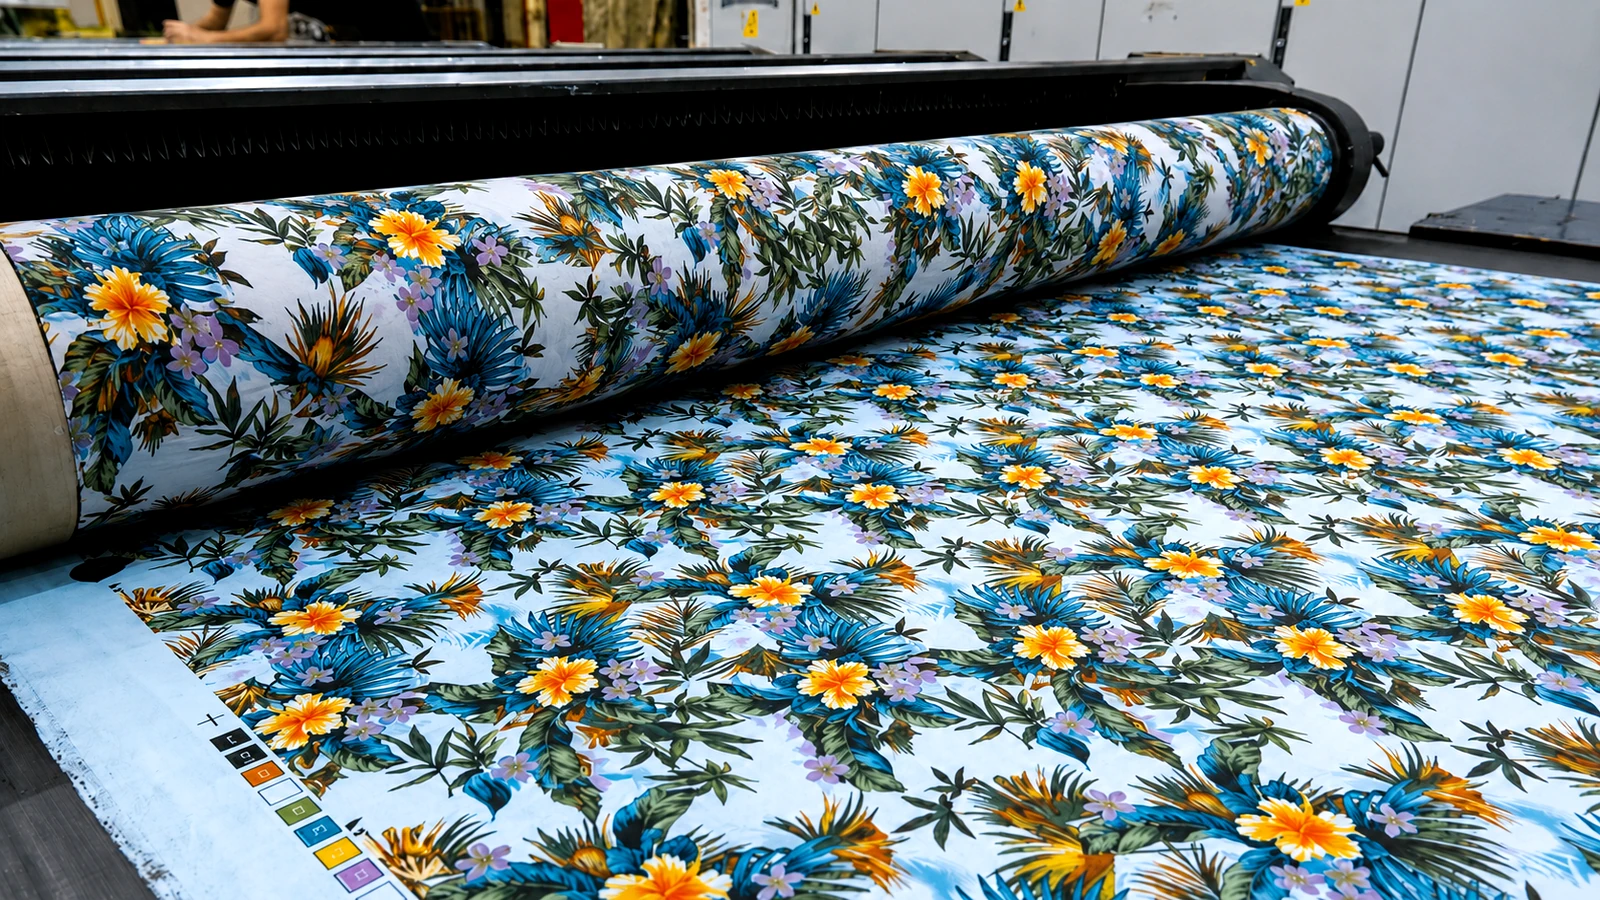
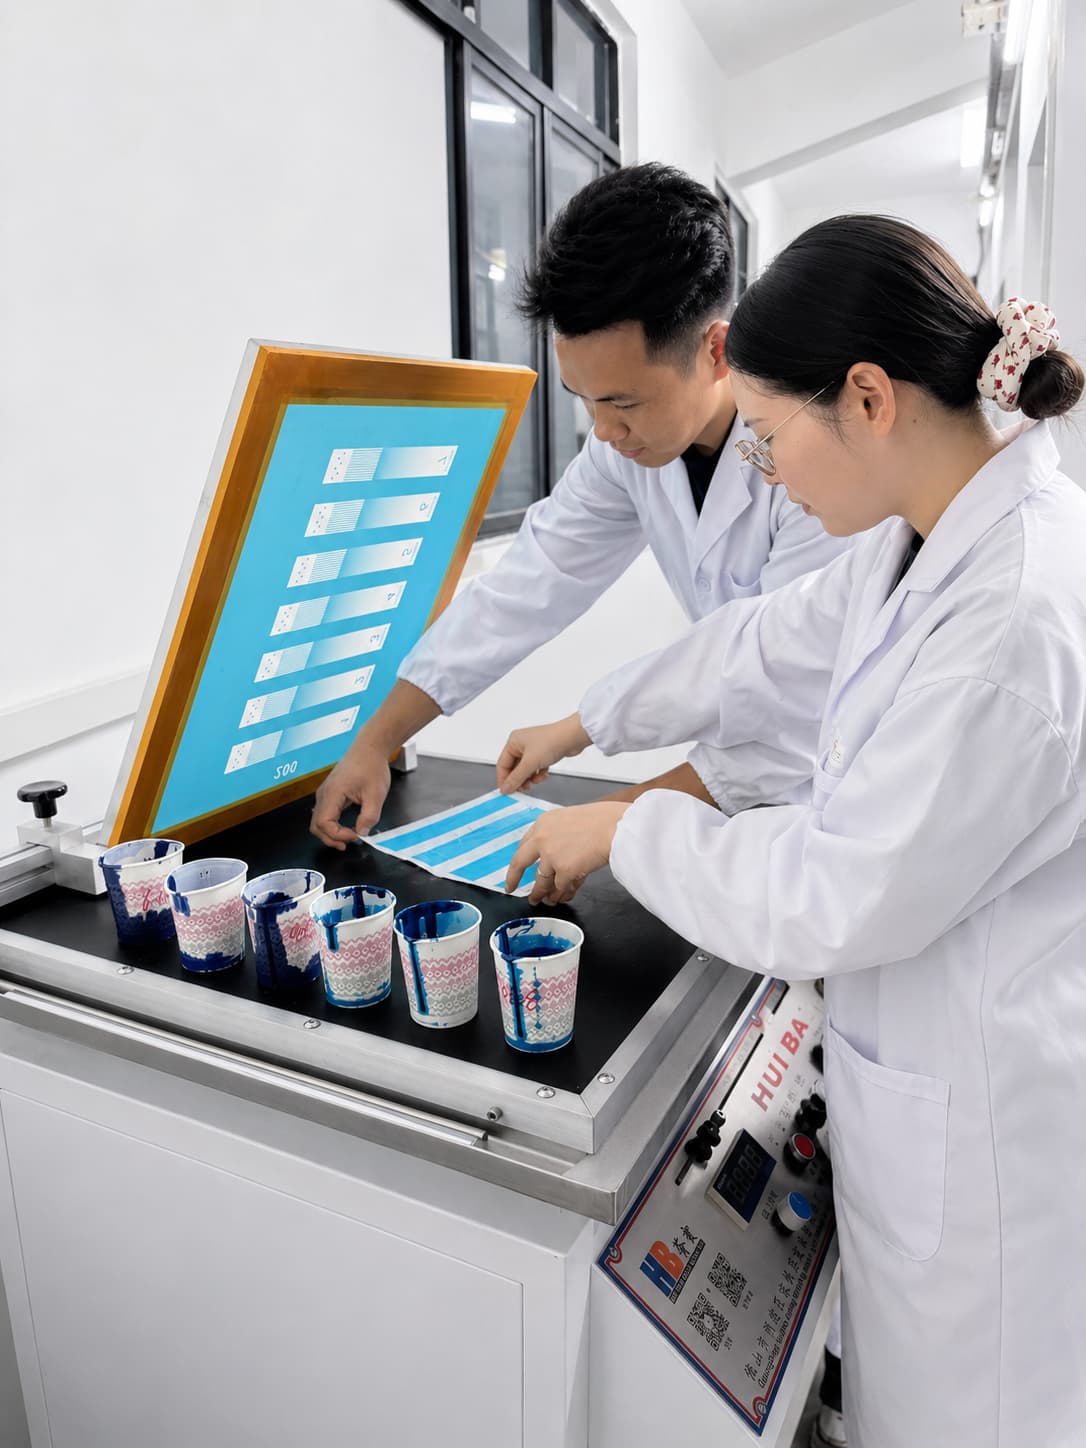
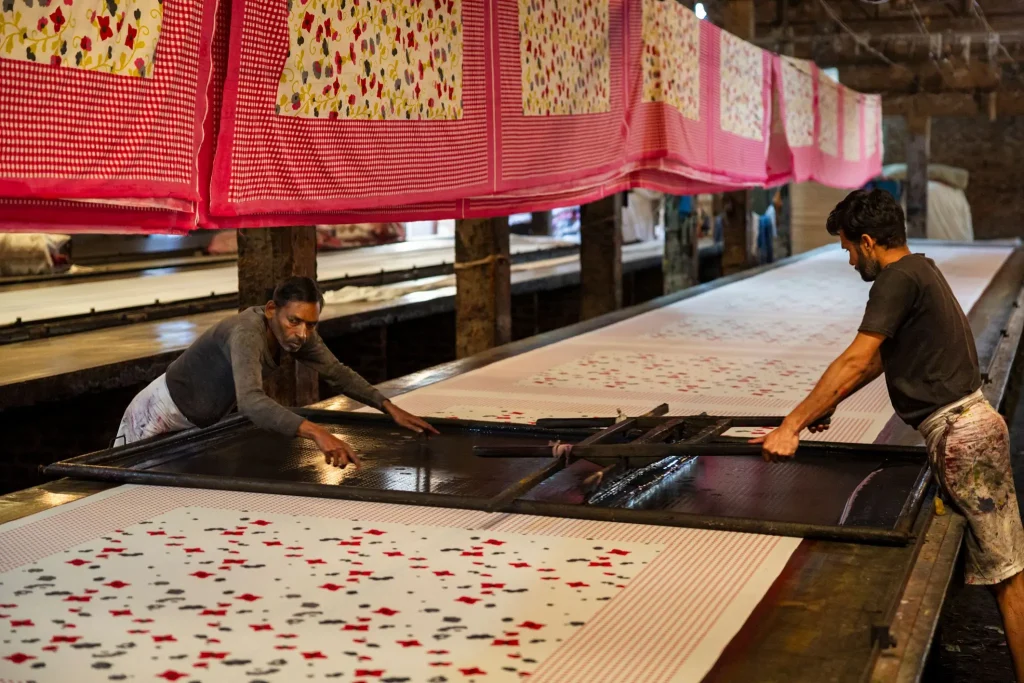
In screen printing, paste transfer depends on flow under shear, recovery, screen geometry, squeegee settings, printing speed and fabric absorption. A higher viscosity reading does not necessarily mean more dye is deposited. Compare paste add-on, penetration, outline sharpness and final shade under controlled printing and fixation conditions.
Viscosity drift can accompany changes in color depth or definition across a production lot. Record where the defect appears and whether it follows paste age, a new batch, a screen change or a process adjustment before assigning a cause.
The Link Between Viscosity and Color Consistency
Stable readings under a defined method improve process control, but do not establish identical rheology or remove all paste-related variability. Dye concentration, fabric preparation, steaming and washing also affect the final shade.
Factors That Cause Viscosity Change in Sodium Alginate Paste
Temperature Effects
Apparent viscosity usually decreases as sample temperature increases, but the measured response depends on the grade, concentration, ions and complete recipe. A reversible temperature effect and persistent change after a defined heat history are different observations. Condition fresh and aged samples to the same agreed temperature before judging paste stability; a warm floor sample cannot be compared directly with a cooler laboratory reference.
Record the actual sample temperature and allow the same conditioning period before each reading. Use one concentration basis, instrument, spindle, speed, container and reading time, with a documented sample history. If the floor temperature differs from the QC temperature, retain both results under their own conditions rather than calling either one the true ambient viscosity.
Mechanical Shear During Mixing and Printing
Many sodium alginate systems are shear thinning: their apparent viscosity decreases as shear rate increases under defined conditions. This does not establish how quickly structure or viscosity returns after a high-shear stage. Flow-curve response and time-dependent recovery must be measured separately. A reactive screen-printing study of alginate and xanthan pastes used steady, transient and dynamic methods to distinguish these responses; its results are not a performance specification for an FSX grade.
For a proposed mixing-history comparison, split a uniformly hydrated stock into matched portions. Apply the normal and extended mixing histories while controlling evaporation and temperature. Return each sample to the agreed measurement temperature and compare at the same low-shear condition and elapsed times. Record mixer geometry, speed, duration, final mass and rest history; RPM alone is not a transferable shear rate. If recovery matters, use a defined low/high/low-shear sequence and report the recovery time and reference reading. A persistent viscosity difference warrants investigation, but does not by itself prove chain scission; chemical exposure, dilution, ions, contamination and measurement history remain possible causes.
pH and Alkali Concentration
Extreme pH and prolonged warm storage can change alginate paste viscosity. Acidification can promote thickening or precipitation; sufficiently alkaline conditions can promote degradation during storage. Evaluate the complete recipe over its intended holding period instead of applying a single pH rule to every grade.
In reactive dye printing paste, alkali (typically sodium carbonate or bicarbonate) is added to the paste to facilitate fixation. If alkali concentration is higher than necessary, or if the paste is stored at elevated temperature after alkali addition, alkali-accelerated degradation can occur. This is one reason why reactive dye printing paste is generally prepared and used within a limited time window after alkali addition.
If you are observing viscosity reduction after alkali addition, review the alkali concentration in your paste recipe and the storage conditions and time between paste preparation and use.
Water Quality and Ionic Content
Calcium contamination can increase alginate viscosity or cause gel formation. Magnesium should not be treated as equivalent to calcium: magnesium alginate is soluble. Measure water hardness and, where needed, calcium separately; compare the working water against a controlled reference in the actual recipe.
Conversely, high monovalent salt content (sodium chloride, sodium sulfate) in the water can suppress the electrostatic repulsion between alginate chains, reducing solution viscosity. If your paste viscosity varies between preparation batches without obvious changes in procedure, water quality is worth investigating. Testing water hardness and total dissolved solids (TDS) at your preparation point is a simple diagnostic step.
Microbial Degradation During Storage
Microbial or enzymatic degradation can contribute to viscosity loss in stored aqueous paste, especially under warm conditions, but it should not be declared the universal or most common cause. Check sanitation, odor or appearance, time trend and retained samples while also controlling temperature, water, pH, additives and shear.
Molecular Weight and Batch Variation
Molecular weight influences alginate solution viscosity, but a routine rotational-viscometer reading is not intrinsic viscosity. Concentration, temperature, ions and the test method also influence the result. Compare supplier lots using identical preparation and measurement conditions.
Request certificates of analysis from several lots and check their viscosity method as well as their values. A difference in apparent viscosity does not by itself prove a molecular-weight change. Confirm powder concentration, moisture basis, hydration, temperature and instrument settings before attributing the difference to manufacturing variation.
How Grade Selection Affects Viscosity Stability
Molecular Weight Distribution
Molecular-weight distribution may help explain differences between grades, but a narrow distribution alone does not demonstrate better production stability. Qualify the complete paste using time-dependent viscosity measurements and print trials under the intended process conditions.
Suppliers do not always specify molecular weight distribution in standard product datasheets, but it can be requested as additional technical information. If viscosity stability is critical to your application, discuss molecular weight distribution with your supplier.
Alginate Composition and Molecular Structure
Sodium alginate does not use the CMC degree-of-substitution specification. Its viscosity and stability reflect molecular-weight distribution, alginate composition, ions, moisture, insoluble matter and manufacturing consistency. Compare grades using defined analytical and application methods.
Alkaline paste stability must be tested in the complete dye, alkali, electrolyte and auxiliary system. A supplier grade label cannot predict holding stability without the actual formulation, temperature and time window.
Purity and Impurity Levels
High residual salt content in sodium alginate — particularly calcium salts from incomplete purification — can cause viscosity variation by introducing divalent cations into the paste system. Specifying a grade with lower calcium content reduces the risk of ionic-driven viscosity variation.
Request calcium content data from your supplier if you are experiencing unexplained viscosity variation, particularly if the variation appears to be batch-dependent rather than preparation-dependent.
Practical Steps to Improve Paste Viscosity Stability
Consistent Paste Preparation Conditions
Standardize the paste preparation procedure to eliminate variation in water temperature, mixing time, addition rate of sodium alginate powder, and alkali addition sequence. Document the standard procedure and train all preparation staff to follow it consistently.
Establish the initial QC reading after the defined hydration, mixing, temperature-conditioning and rest procedure. Record the elapsed time rather than using an undefined reading immediately after preparation. Repeat that procedure at the planned holding checkpoints and compare with a covered reference so continued hydration, evaporation or sample handling is not mistaken for ageing.
Monitoring Viscosity During Production
In production runs of more than a few hours, periodic viscosity measurement during the run allows you to track viscosity drift before it becomes severe enough to affect print quality. A simple rotational viscometer is adequate for this purpose.
Establish acceptable viscosity drift from trials that meet the mill’s print-quality requirements. Do not apply a universal percentage tolerance. Define a hold-and-investigate procedure for out-of-limit paste; any dilution or replenishment must account for the resulting dye, alkali and auxiliary concentrations and be rechecked before use.
Storage Conditions and Shelf Life Management
Store prepared paste in clean, covered containers under the temperature and holding limits qualified for the complete recipe. Do not assume refrigeration extends usable life: evaluate cooling, return to the use temperature, homogeneity and print quality before including it in the procedure. Label preparation and alkali-addition times, and do not use paste beyond its approved holding window.
Clean paste storage containers and mixing equipment regularly to reduce microbial contamination. Even in temperate climates, residual paste in imperfectly cleaned equipment can introduce microbial load into fresh batches.
Troubleshooting Viscosity Instability in Production
Viscosity Drops During a Production Run
If viscosity falls during a run, first check measurement temperature, concentration, accidental dilution, formulation additions and sample handling. Investigate prolonged shear, chemical degradation or microbial activity when the time trend and controlled comparison support those possibilities.
Check whether the viscosity drop correlates with time, temperature, or the addition of a specific paste component. Eliminating variables one at a time will identify the cause more reliably than making multiple changes simultaneously.
Batch-to-Batch Viscosity Variation
If viscosity differs between paste batches prepared by the same procedure, the cause is either in the sodium alginate itself (batch variation from the supplier) or in the preparation inputs (water quality, powder weight accuracy, mixing time consistency).
Verify preparation inputs first — weigh the sodium alginate powder on a calibrated scale for each batch, check water temperature, and confirm mixing time. If inputs are consistent and viscosity still varies, request CoA data from the sodium alginate batches in question and compare viscosity values. If supplier batch variation is confirmed, this is a supplier quality conversation.
Paste Thickening or Gelling After Preparation
If paste thickens during storage, check continued hydration, cooling, evaporation and calcium or other formulation interactions. Compare a covered reference sample under the same measurement conditions before changing the grade.
Cooling can increase the apparent viscosity of the paste. If chilled or freeze-thawed paste shows persistent gel particles, investigate calcium content and the formulation rather than a supposed alginate DS value. Bring the sample to the agreed test temperature and assess homogeneity, filtration and print performance before reuse.
Поширені запитання
Does sodium alginate have a DS value?
No. Degree of substitution is a cellulose-derivative parameter used for products such as CMC, not sodium alginate.
Why can viscosity drop during a printing shift?
Possible causes include paste temperature, shear, dilution, pH or ion interaction, contamination and paste age. Change one controlled variable at a time.
Why does paste thicken after mixing?
Hydration may still be developing, the paste may cool, water may evaporate or additives may interact. Measure at fixed intervals and conditions.
Can equal Brookfield readings guarantee equal printing performance?
No. Rheology, filtration, transfer, penetration, fixation and wash-off may differ. Compare the complete paste and printed fabric.
What should a mill send for stability troubleshooting?
Send timed viscosity results with the full method, water data, formula and addition order, temperature, holding time, batch code and defect evidence through Зразки та підбір.
How FSX Chemical Supports Viscosity-Sensitive Applications
For a grade evaluation, request the current technical data sheet and available batch-specific certificates of analysis from FSX Chemical. Agree on the test method and acceptance criteria before comparing lots or starting a production trial.
Наступні кроки:
Зверніться до нашої технічної служби — share the observed defect and controlled test results for viscosity troubleshooting.
Request a TDS — review viscosity specification and batch tolerance data
Замовити зразок — discuss a viscosity-stability trial under your production conditions.
Record the Viscosity Test Conditions
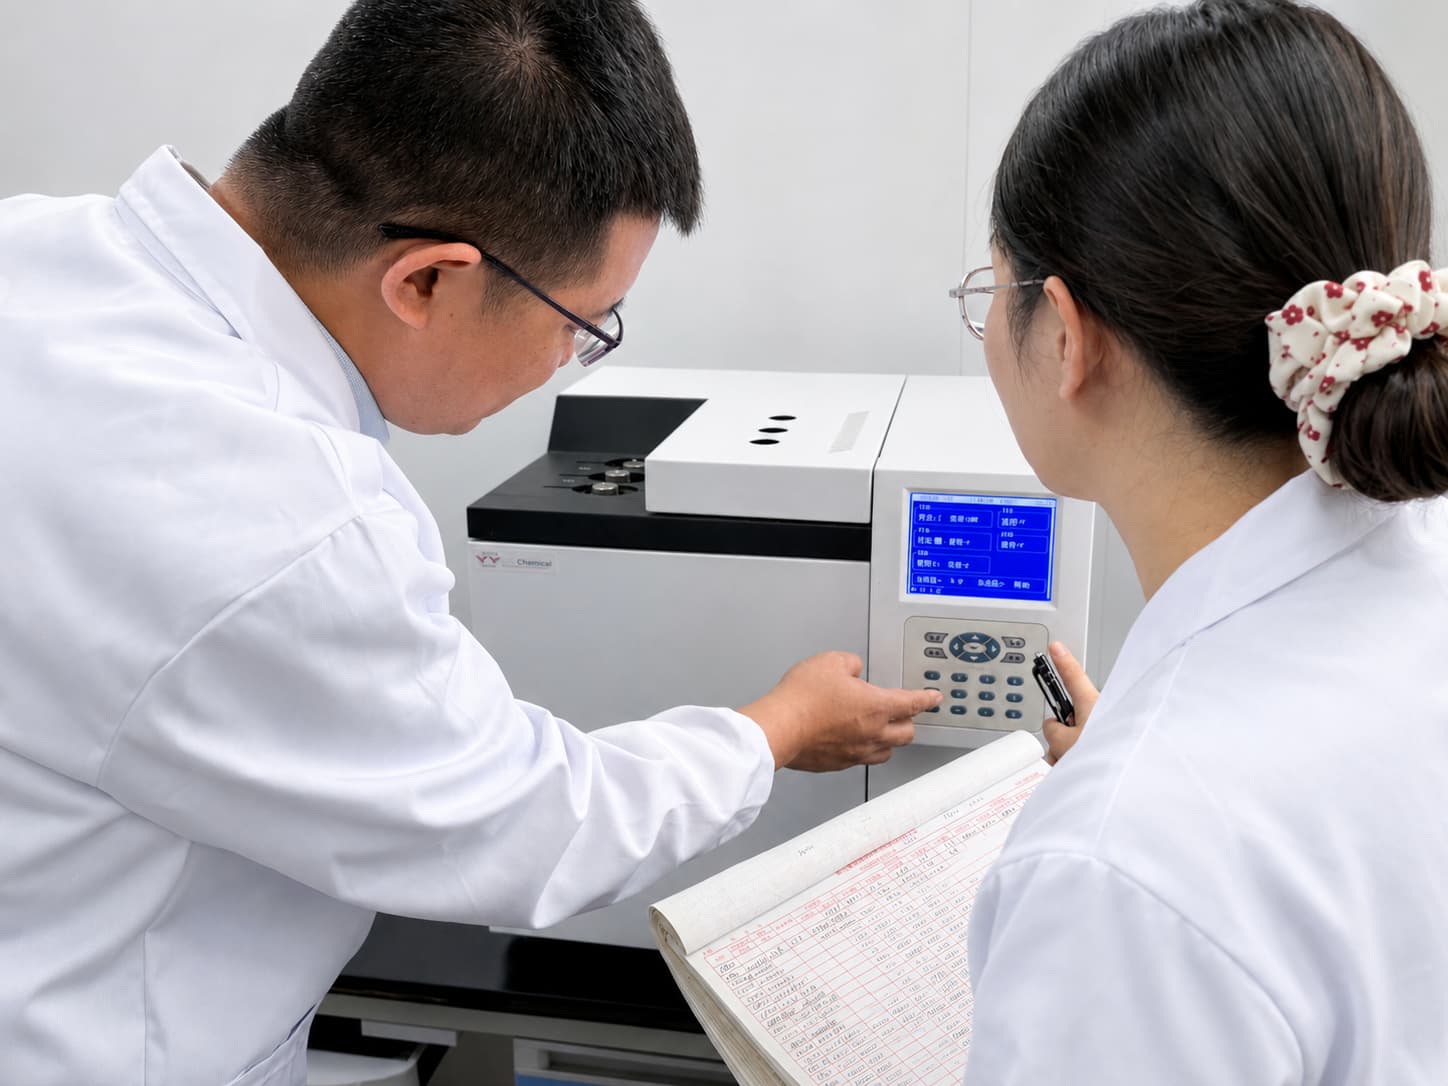
For each reading, record the grade and batch, powder concentration and mass basis, water source, recipe, addition order, hydration and holding time, sample temperature, instrument, spindle, speed and reading time. Use the same sampling and mixing procedure at each checkpoint. This is a suggested comparison protocol, not an FSX product specification.
Background reference: FAO: Production, Properties and Uses of Alginates. General polymer behavior does not replace testing of the selected textile grade and complete printing recipe.