Khắc phục sự cố liên quan đến bột in trên vải: Nguyên nhân, phương pháp kiểm tra và biện pháp khắc phục
Textile printing paste problems rarely have only one cause. This troubleshooting guide explains how to...
Textile printing paste problems rarely have one cause. Diagnose the symptom by checking product identity, preparation, temperature, viscosity method, formulation additions, holding time, machine conditions, fabric and post-treatment. Change one controlled variable at a time before replacing the thickener.
Identify the material being diagnosed: a dye-screen paste, a pigment-binder screen paste, or a fabric-applied digital pretreatment. Their chemistry, application and after-treatment differ. Record the dye or ink system, fibre and product-addition position before testing. A fabric pretreatment or conventional screen thickener is not automatically suitable for addition to printhead ink; diagnose that ink system under its own supplier-approved requirements.
This is why textile printing problems should not be corrected by changing the thickener immediately. A paste that appears too thin may be caused by incorrect concentration, high temperature, incomplete hydration, electrolyte interaction or an incorrect viscosity test method. A blurred print may come from paste rheology, but it may also come from excessive application, absorbent fabric or unsuitable machine settings.
Effective troubleshooting begins by defining the symptom, collecting process data and changing one variable at a time. The objective is to identify the real root cause before modifying the formulation.
The following guide provides a practical troubleshooting framework for reactive, disperse, pigment and digital textile printing paste systems.
Textile printing paste performance is affected by several groups of variables at the same time. A visible defect on the fabric is often the final result of interactions that started much earlier in the process.
Raw-material variables
Thickener grade, polymer concentration, moisture, particle profile, batch variation and storage conditions can influence paste preparation and rheology.
Preparation variables
Water quality, powder-addition rate, mixer geometry, mixing speed, hydration time, temperature and order of chemical addition can all change the final paste.
Formulation variables
Dyes, pigments, salts, alkalis, binders, crosslinkers, humectants, surfactants and other polymers can change viscosity and physical stability.
Machine variables
Pumping, circulation, screen condition, squeegee pressure, printing speed, coating gap and application quantity influence how the paste reaches the textile.
Fabric variables
Fibre composition, fabric weight, construction, absorbency and previous finishing treatments influence spreading and penetration.
Post-treatment variables
Drying, steaming, thermofixation, curing and washing can change shade, definition and fabric handle after printing.
Troubleshooting should therefore begin with the complete process rather than with one material in isolation.
Start with Five Basic Checks
Locate the first point where the questioned material differs from a retained approved control: prepared thickener base/stock, complete paste, freshly printed fabric, or finished fabric. Compare under the same preparation, measurement and machine conditions. For dye printing, retain checkpoints after the specified fixation and wash-off; for pigment printing, evaluate after the validated cure and conditioning. For digital fabric pretreatment, hold ink and print settings fixed when comparing treated fabrics. Use the five checks below to isolate the difference, then change only a variable compatible with that route.
1. Confirm the correct product
Check the commercial product code, batch number, package label and current TDS. Make sure the material used in production is the same grade that was approved during testing.
2. Confirm the preparation method
Check concentration, water quantity, powder addition, mixing speed, hydration time and order of chemical addition.
3. Confirm temperature
A viscosity difference may be caused by sample temperature rather than a real formulation change.
4. Confirm the viscosity test method
Record instrument model and torque range, spindle or geometry, speed, container/sample volume, concentration basis, temperature, preparation/rest history and reading time before comparing results. Record torque as well as viscosity, and follow the instrument’s valid range. Brookfield’s viscosity guidance explains why spindle and speed selection matter; changing either can change the apparent viscosity of a non-Newtonian paste.
5. Compare with a retained reference
Where available, prepare a retained sample of the approved product using exactly the same method as the current batch.
1. Lumps and Fish Eyes in the Printing Paste
Lumps are common when powdered thickeners hydrate rapidly at the surface before water reaches the inside of the particle cluster.
Possible causes
Powder added too quickly
Insufficient water circulation before addition
Powder added into one location
Unsuitable mixer or impeller position
Incorrect water temperature
Insufficient hydration time
Moisture-damaged or compacted powder
Recommended checks
Prepare a fresh laboratory batch while recording powder-addition time and mixing conditions. Add the thickener gradually into a properly circulating water phase and inspect the paste before and after the defined hydration period.
Do not simply increase mixing time
Persistent lumps may contain dry polymer surrounded by a hydrated outer layer. Additional mixing does not always eliminate them efficiently.
When comparing alginat natri, CMC hoặc CMS, the preparation method should be appropriate for the specific grade.
2. Printing Paste Viscosity Is Too Low
Low viscosity does not automatically mean that more thickener should be added.
Possible causes
Incorrect weighing or excessive water
Incomplete polymer hydration
Sample temperature above the reference condition
Incorrect product grade
Different viscosity measurement method
Salt, alkali or another electrolyte reducing viscosity
Prolonged shear in a sensitive system
Microbiological or chemical degradation in stored paste
Recommended checks
Verify batch weights first. Then confirm temperature, hydration time and viscosity method. If the stock paste is correct but the complete color paste becomes thin, investigate the formulation rather than immediately increasing polymer dosage.
Correct carefully
Adding dry thickener directly to a completed color paste can create lumps and local concentration differences. Any correction procedure should be validated for the specific product and formulation.
3. Printing Paste Viscosity Is Too High
Excessive viscosity can reduce screen transfer, create pumping resistance and produce uneven solid areas.
Possible causes
Excess thickener dosage
Incorrect total batch weight
Water evaporation
Lower measurement temperature
Continued hydration after the first test
Incorrect grade used in production
Different measurement speed or spindle
Check before adding water
Confirm the sample temperature and test method. If evaporation is the cause, identify why the tank or container is losing water.
Why uncontrolled dilution is risky
Adding water changes not only viscosity but also the concentration of dyes, salts, binders, alkalis and other auxiliaries. The corrected paste may reach the target viscosity while no longer matching the approved formulation.
4. Viscosity Changes During Holding
A paste may be within specification immediately after preparation and move outside the operating window several hours later.
Viscosity increases may be caused by
Continued polymer hydration
Evaporation
Temperature decrease
Delayed interaction between formulation components
Viscosity decreases may be caused by
Temperature increase
Electrolyte interaction
pH change
Prolonged mechanical shear
Polymer incompatibility
Contamination or degradation
Recommended approach
Take representative aliquots at defined production checkpoints and keep them covered to limit evaporation. Condition each to the same test temperature and apply the same rest and reading sequence. Record apparent viscosity, pH, sample temperature, preparation time, appearance and separation together. If a circulating paste reads lower, compare it after a defined recovery period with a matched held control before calling the loss permanent degradation. Recovery of one reading does not prove the paste is suitable for continued production.
A numerical change is most important when it also changes machine behavior or finished-fabric performance.
5. Viscosity Changes After Adding Salt, Alkali or Auxiliaries
Many printing thickeners are sensitive to ionic strength, pH and local chemical concentration.
Possible causes
Electrolyte interaction with the polymer
Rapid local pH change
Highly concentrated chemical added directly
Incorrect addition sequence
Incompatible polymers or auxiliaries
Use staged testing
Prepare the thickener paste first, then add formulation components one at a time while measuring viscosity and observing appearance.
Identify the critical addition
When the viscosity changes sharply after one component is introduced, investigate its concentration, dilution and addition sequence before changing the thickener.
Application chemistry matters
A product suitable for one reactive, disperse or pigment formula may behave differently under another chemical load.
6. Excessive Filter Residue or Poor Screen Passage
Filter residue can interfere with screens, pumps and continuous production. However, its origin should be identified before blaming raw material purity.
Possible sources of residue
Incompletely hydrated thickener
Powder lumps
Hydrated gel particles
Chemical precipitation
Polymer incompatibility
Fibres from bags or fabric
Dirty tanks or pipelines
Foreign particles from production equipment
Test the stock paste first
If the stock thickener paste filters well but the complete formulation does not, the problem probably develops after another chemical is added.
Inspect the residue
Dry or examine the retained material where practical. The appearance of the residue can help distinguish polymer gel from foreign contamination or chemical precipitation.
Standardize filtration
Record filter material, opening size, sample quantity, pressure condition and time so that results remain comparable.
7. Excessive Foam and Entrapped Air
Foam can produce inaccurate viscosity readings, poor transfer, pinholes and uneven printed areas.
Possible causes
Mixer pulling air into the batch
Excessive mixing speed
Surfactant-containing auxiliaries
Air entering through pump seals or return lines
Incorrect tank level or circulation pattern
Observe when foam begins
If foam starts during water and thickener preparation, review mixing. If it appears only after an auxiliary is added, review that component.
Measure foam decay
Initial foam volume and the time required for bubbles to disappear can both be useful.
Do not automatically increase defoamer
Defoamer can influence wetting, coating and printing behavior. Correct the mechanical cause first where possible.
8. Paste Separation, Settling or Syneresis
A printing paste should remain sufficiently uniform during its approved holding and production period.
Possible causes
Insufficient rheological structure
Incompatible thickener and formulation components
Incorrect pH
High electrolyte load
Poor pigment or dye dispersion
Incorrect solids concentration
Storage beyond the validated holding period
Inspect the type of separation
Clear liquid at the surface, dense sediment at the bottom and visible gel phases can indicate different mechanisms.
Do not rely only on remixing
A paste that temporarily returns to a uniform appearance after stirring may still be fundamentally unstable.
Print fresh and stored paste
Compare fabric results to determine whether the physical change affects application quality.
9. Poor Paste Transfer
A paste may have acceptable standing viscosity but fail to transfer completely through the printing equipment.
Possible causes
Viscosity too high
Unsuitable shear-thinning behavior
Excessive structural recovery
Screen or mesh too restrictive
Low squeegee pressure
Insufficient paste supply
Filter or screen contamination
Do not judge from standing viscosity alone
Compare viscosity at multiple speeds or use application-relevant rheology data when possible.
Check the machine before reformulating
Screen condition, squeegee settings and paste level can create symptoms that resemble excessive viscosity.
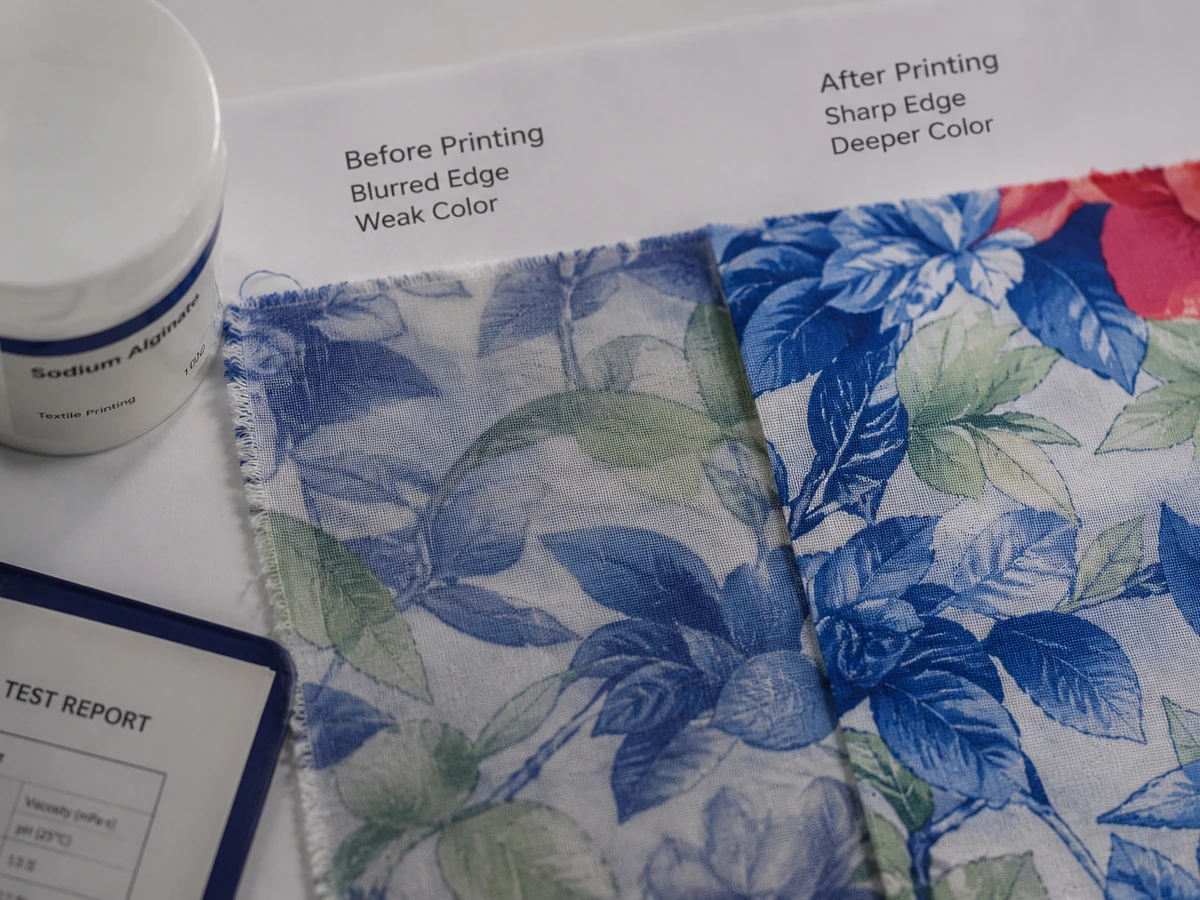
10. Printed Edges Spread or Lose Definition
Edge spreading is one of the most common reasons printing mills consider changing their thickener.
Possible paste-related causes
Viscosity below the practical operating range
Weak structural recovery after shear
Excessive water or humectant
Excessive paste application
Possible fabric-related causes
High absorbency
Open fabric construction
Inconsistent pretreatment
Residual wetting or finishing chemicals
Possible process-related causes
Excessive pressure
Slow drying
Incorrect screen conditions
Uncontrolled moisture before fixation
Increasing viscosity may reduce spreading in some cases, but excessive viscosity can create poor transfer and broken fine lines. Rheology, application quantity and fabric absorbency should be reviewed together.
11. Fine Lines Break or Small Details Disappear
Broken lines are not always the opposite of edge spreading. The paste can be too structured to transfer through fine design elements.
Possible causes
Viscosity too high
Poor flow under shear
Filter residue or gel particles
Tình trạng màn hình bị che khuất
Insufficient application pressure
Insufficient paste supply
Unsuitable fabric surface
Use a diagnostic test pattern
Include several line widths, small text and dots. This makes it easier to determine the point at which detail begins to fail.
Compare screen and paste together
If the same paste works through a more open screen, investigate filtration and rheology before changing total viscosity.
12. Large Solid Areas Print Unevenly
A formulation can reproduce fine lines but still perform poorly in large solid areas.
Possible causes
Poor leveling
Excessive paste structure
Foam or entrapped air
Uneven screen transfer
Variable fabric absorbency
Insufficient paste supply
Uneven squeegee or roller pressure
Check dark shades
Black, navy and other deep shades often reveal levelness and transfer differences more clearly than light colors.
Check across the fabric width
A left-to-right difference may indicate mechanical or fabric variation rather than the thickener itself.
13. Excessive Fabric Penetration or Strike-Through
Too much paste moving through the fabric can reduce surface color concentration and create reverse-side contamination.
Possible causes
Low paste structure
Excessive application quantity
High machine pressure
Lightweight or open fabric
High fabric absorbency
Unsuitable wetting behavior
Inspect both sides of the textile
Compare surface coverage and back penetration using the same fabric lot and print conditions.
Avoid correcting fabric problems only with viscosity
Extremely high viscosity may reduce penetration but create poor transfer. Application quantity and machine settings should also be optimized.
14. Color Becomes Weak After Fixation or Washing
When the wet or dried print looks strong but color becomes weak after fixation or washing, the thickener may not be the primary cause.
Possible causes
Incorrect dye or pigment concentration
Excessive penetration into the fabric
Insufficient alkali or fixation chemistry
Incorrect steaming or curing conditions
Reactive dye hydrolysis
Binder-film failure in pigment printing
An after-treatment route that does not match the dye, fibre or binder specification
Check fixation before changing the thickener
Temperature, moisture, dwell time and chemical conditions should be recorded.
Compare identical post-treatment
Candidate and reference thickener systems must use the same fixation and washing conditions.
15. Difficult Wash-Off or Stiff Fabric Handle
First separate a removable dye-printing paste residue from the binder film intended to remain in a pigment print. Stiff hand can occur in both routes, but the corrective actions differ. Do not use stronger washing as a general remedy for a pigment film or reduce dye-print wash-off solely to retain shade.
Possible causes
Excessive thickener dosage
High paste pickup
Thickener route with unsuitable removal behavior
Insufficient washing
Excessive binder deposition
Incorrect curing conditions
Evaluate after complete finishing
Fabric handle should not be judged from the freshly printed material.
Compare printed and unprinted areas
This helps determine whether stiffness is related to paste deposition or the fabric finishing process.
Consider total polymer solids
For a dye-printing route, compare residual paste after the specified fixation and wash-off; investigate grade suitability, add-on and washing together. For pigment printing, compare cured hand at recorded paste deposit, binder dose and documented nonvolatile addition, then check the approved cure and fastness. A heavier cured deposit does not identify which polymer caused stiffness, and nonvolatile content does not selectively measure active thickener polymer.
16. Laboratory Results Are Good but Production Fails
Scale-up differences are one of the most important causes of failed thickener evaluations.
Laboratory and production differ in
Tank geometry
Impeller design
Batch volume
Mixing circulation
Heat generation
Thời gian bù nước
Pump and pipeline shear
Thời gian giữ
Fabric quantity and variation
Do not copy mixer RPM directly
The same rotational speed in a small laboratory mixer and a production tank does not create the same flow pattern.
Conduct a controlled scale-up
Preserve concentration, addition sequence and QC method while adjusting mixing parameters appropriately for production equipment.
Monitor the entire production run
Compare fabric from the beginning, middle and end rather than approving only the first metres.
17. Approved Sample and Bulk Batch Perform Differently
A successful laboratory sample must be connected to a controlled commercial product and manufacturing batch.
Check product identity
Compare the sample code, commercial grade, purchase order, package label and batch COA.
Check incoming test conditions
Verify whether the original sample and bulk product were prepared using the same concentration, water, hydration and viscosity method.
Check storage and transport
Moisture exposure, damaged packaging or inappropriate storage can change the condition of some thickener products.
Use retained samples
Prepare the approved retained sample and the questioned production batch side by side under identical conditions.
Verify the first commercial batch
First-batch verification reduces the risk of moving directly from a small sample to unrestricted production.
Troubleshooting by Printing Route
Lộ trình in ấn
Common Paste Issues
Priority Checks
In lụa phản ứng
Viscosity drift, spreading, filtration, weak color after wash-off
Thickener hydration, alkali and salt compatibility, fabric, steaming and wash-off
Thickener route, dye dispersion, rheology, polyester surface and fixation
Pigment printing
Binder instability, poor definition, stiff handle and weak rubbing performance
Thickener-binder compatibility, solids, curing and film formation
Reactive digital pretreatment
Uneven pickup, ink spreading, viscosity drift and difficult wash-off
Pretreatment rheology, fabric absorbency, chemical distribution and fixation
Disperse digital pretreatment
Uneven application, filtration problems and inconsistent color
Polyester preparation, paste stability, coating uniformity and thermal process
Pigment digital pretreatment
Spreading, binder interaction, stiff handle and uneven solids
Binder compatibility, pickup, rheology, drying and curing
Digital printing should use an application-specific hỗn hợp in kỹ thuật số or validated pretreatment route rather than transferring a conventional screen-printing paste directly.
A Practical Root-Cause Troubleshooting Workflow
Step 1: Describe the symptom precisely
Replace general statements such as “the paste is bad” with measurable observations such as “viscosity decreases after alkali addition” or “black fine lines spread after 30 minutes of holding.”
Step 2: Identify when the problem first appears
Determine whether the problem starts during powder preparation, chemical addition, holding, circulation, printing, fixation or washing.
Step 3: Compare with the approved reference
Prepare current and reference products side by side using identical conditions.
Step 4: Separate material and process variables
Use the same batch of fabric and chemicals where possible while changing only one suspected variable.
Step 5: Test the stock paste
Check hydration, viscosity, filtration, foam and appearance before adding dyes or other chemicals.
Step 6: Add formulation components in stages
This helps identify whether the problem begins after salt, alkali, binder or another auxiliary is introduced.
Step 7: Test fresh and held paste
Compare immediately after preparation and after a production-relevant holding period.
Step 8: Complete the fabric test
Evaluate definition, penetration, color uniformity and surface condition.
Step 9: Complete fixation and post-treatment
Do not make the final decision from the wet print alone.
Step 10: Conduct a limited production trial
Confirm performance under realistic tank size, circulation, speed and production time before changing bulk supply.
What Data Should Be Recorded Before Adjusting the Paste?
Good troubleshooting depends on good records. Before changing the formulation, collect enough information to reconstruct the batch.
Thickener information
Product and grade
Batch number
TDS and recent COA where available
Liều lượng
Powder or liquid condition
Preparation information
Total batch size
Nguồn nước
Water temperature
Mixing equipment
Powder-addition time
Mixing duration
Thời gian bù nước
Thứ tự cộng
QC information
Viscosity and complete measurement method
pH
Lọc
Hình thức
Bọt
Holding-time results
Printing information
Fabric composition and weight
Printing equipment
Screen or application conditions
Tốc độ sản xuất
Paste application quantity where available
Fixation or curing conditions
Wash-off process
Defect information
Photographs
Printed fabric sample
Paste sample
Time when the defect first appeared
Whether the defect is continuous or intermittent
When Should You Change the Thickener?
Changing the thickener is appropriate when controlled testing shows that the current polymer route cannot meet the required combination of viscosity, rheology, stability, filtration and finished-fabric quality.
Consider a different grade when
The current viscosity range is unsuitable for the equipment
Hydration is consistently incompatible with the production process
Filtration remains unacceptable under controlled preparation
Chemical compatibility is insufficient
Rheology produces poor transfer or excessive spreading
Holding stability does not meet production requirements
Batch consistency cannot be controlled satisfactorily
Consider a different thickener family when
The application chemistry itself is better suited to another polymer route. For example, conventional reactive printing may begin with alginat natri , while selected disperse or compound systems may evaluate CMS , and selected printing or rheology applications may evaluate CMC .
Do not change products without a reference trial
A candidate product should be compared with the current grade under the same laboratory and production conditions before commercial conversion. For a conventional pigment-screen paste, use staged synthetic thickener production approval tests after the cause is isolated, rather than treating a viscosity correction as full product approval.
Các câu hỏi thường gặp
What should be checked first when a printing paste suddenly changes?
Confirm the product and batch, preparation record, water, temperature, hydration time, viscosity method and addition sequence. Compare the result with an identified retained sample before changing the formula.
Why can viscosity be correct while print definition is poor?
One viscosity number does not describe shear response, recovery, paste transfer, fabric absorbency or pickup. Review multi-speed behavior and the complete printing process.
How should lumps or fish eyes be investigated?
Check powder-addition rate, agitation pattern, wetting, hydration time, water quality and filtration residue. Excess mixing after lumps form may introduce air without correcting the wetting failure.
What causes viscosity to change after salt, alkali or auxiliaries are added?
Electrolytes, pH, addition order, local concentration and polymer compatibility can alter thickener structure. Add components in controlled stages and measure after each stage.
When should a mill test a different thickener grade?
Test an alternative only after the method and root-cause checks are controlled, or when the existing grade cannot meet the complete-paste, machine and finished-fabric requirements within a practical operating window.
How FSX Chemical Supports Printing Paste Troubleshooting
FSX Chemical supplies sodium alginate, CMC, CMS, digital printing paste and related textile thickener routes for printing mills, formulators, importers and distributors.
Troubleshooting begins with the customer’s actual process rather than with an assumption that the thickener must be replaced.
Buyers can provide
Current thickener or printing paste name and grade
TDS, SDS hoặc COA hiện tại
Physical powder or paste sample
Độ nhớt và phương pháp thử nghiệm toàn diện
Công thức hoàn chỉnh
Quy trình chuẩn bị và cấp nước
Fabric composition and construction
Reactive, disperse, pigment or digital route
Printing equipment and production speed
Filtration or stability records
Defect photographs or printed fabric samples
Technical review may include
Review of the existing product and test method
Identification of likely root-cause categories
Alignment of viscosity and preparation procedures
Review of chemical compatibility
Selection of an appropriate candidate product family
A candidate product remains subject to controlled laboratory and production evaluation. Final suitability depends on the complete formulation, fabric, equipment and post-treatment process.
Natri alginat được sử dụng rộng rãi trong in ấn dệt may với vai trò là chất làm đặc ổn định và có thể giặt được cho hỗn hợp in phản ứng. Tìm hiểu cách đánh giá cấp độ độ nhớt, độ tinh khiết và tính phù hợp trong ứng dụng trước khi mua hàng, cũng như cách FSX Chemical hỗ trợ người mua trên toàn cầu thông qua dữ liệu kỹ thuật và mẫu sản phẩm.
Việc lựa chọn nhà cung cấp CMC phù hợp không chỉ đơn thuần là so sánh giá cả. Hướng dẫn này trình bày các tiêu chí đánh giá, danh sách kiểm tra tài liệu và quy trình dùng thử mà các đội ngũ mua sắm cần tuân thủ trước khi quyết định đặt hàng số lượng lớn.
Hỗn hợp in dựa trên CMC được sử dụng rộng rãi trong in vải bằng bột màu, in phản ứng và in kỹ thuật số. Hướng dẫn này giải thích các thông số quan trọng, cách so sánh các nhà cung cấp và những yêu cầu cần đưa ra trước khi đặt hàng số lượng lớn.
Việc bảo quản không đúng cách là một trong những nguyên nhân phổ biến nhất dẫn đến các vấn đề về hiệu suất của natri alginat trong in ấn dệt may. Hướng dẫn này đề cập đến các điều kiện bảo quản dạng bột và dạng bột nhão, thời hạn sử dụng dự kiến, các dấu hiệu suy giảm chất lượng, cũng như những điều cần kiểm tra khi nhận hàng mới.
Chất điều chỉnh độ nhớt (CMS) dành cho mực in dệt may có thể giúp điều chỉnh độ nhớt, cải thiện khả năng thao tác với mực in và đảm bảo hiệu suất ổn định của công thức. Hướng dẫn này giải thích cách người mua có thể đánh giá các loại CMS dựa trên các tiêu chí như độ nhớt, DS, độ hòa tan, pH, độ ẩm và thử nghiệm mẫu trước khi mua số lượng lớn.
Nhiều nhà cung cấp quảng cáo sản phẩm "alginat natri tùy chỉnh", nhưng trên thực tế, thuật ngữ này lại bao hàm những khái niệm rất khác nhau. Hướng dẫn này sẽ giải thích những thông số nào thực sự có thể điều chỉnh, những thông số nào bị giới hạn bởi các quy luật hóa học cơ bản, và cách đánh giá các tuyên bố về khả năng tùy chỉnh của nhà cung cấp.
Natri alginat có thể được xem xét sử dụng cho một số hệ thống tẩm sợi dọc hoặc công thức dệt may cụ thể, nhưng không nên lựa chọn chỉ dựa trên tên sản phẩm hay những tuyên bố chung chung về hiệu suất. Hướng dẫn này giải thích cách các nhà máy dệt may có thể đánh giá các yếu tố như độ nhớt, tính chất màng, khả năng tương thích với sợi, quá trình tẩy tẩm, ảnh hưởng của nước cứng, TDS, COA, thử nghiệm mẫu và tính ổn định giữa các lô trước khi mua số lượng lớn.
Trước khi mua số lượng lớn, cần đánh giá chất in có độ bám dính cao dựa trên các yếu tố như loại vải, quy trình in, độ nhớt và tính lưu biến, thử nghiệm độ bám dính, thử nghiệm giặt hoặc thử nghiệm xử lý, tính tương thích của công thức, TDS, COA, SDS, thử nghiệm mẫu và tính nhất quán giữa các lô sản phẩm.
Giá alginat natri có sự chênh lệch đáng kể giữa các nhà cung cấp và các loại sản phẩm, nhưng không phải mọi sự chênh lệch về giá đều phản ánh sự khác biệt thực sự về chất lượng. Hướng dẫn này giải thích các yếu tố ảnh hưởng đến chi phí, cách so sánh báo giá trên cơ sở tương đương và những dấu hiệu cảnh báo cần lưu ý khi đánh giá các đề xuất của nhà cung cấp.
Bột alginat natri có thể hỗ trợ việc kiểm soát độ nhớt trong hỗn hợp in dệt phản ứng, nhưng hiệu quả đáng tin cậy phụ thuộc vào việc phân tán, ngâm nước, chất lượng nước, quá trình lọc, bảo quản và kiểm soát từng mẻ sản xuất đúng cách.
Việc so sánh các loại bột mực không chỉ đơn thuần là tìm một sản phẩm có độ nhớt tương tự. Hướng dẫn này giải thích cách các nhà máy in dệt may có thể so sánh các loại bột mực thông qua việc đánh giá quy trình ứng dụng, chuẩn bị mẫu trong điều kiện kiểm soát, thử nghiệm in và kiểm tra sự tương đồng giữa mẫu và lô hàng lớn.
Việc so sánh cấp độ tùy chỉnh giúp các nhà in dệt may so sánh một chất làm đặc hoặc hỗn hợp in mới với một mẫu tham chiếu đã được phê duyệt trong các điều kiện thử nghiệm được xác định rõ. Hướng dẫn này giải thích các thông tin cần thiết, các giai đoạn xác nhận trong phòng thí nghiệm và trong sản xuất, cũng như cách người mua có thể chuyển từ mẫu ban đầu sang thông số kỹ thuật thương mại đã được thống nhất.
Vui lòng cung cấp tên sản phẩm, ứng dụng, số lượng, điểm đến và bất kỳ tài liệu kỹ thuật (TDS),
hình ảnh mẫu hoặc tài liệu nào mà quý khách đã có. FSX Chemical sẽ xem xét
thông tin này và đề xuất bước tiếp theo liên quan đến báo giá, đối chiếu mẫu
hoặc lựa chọn sản phẩm.
Thông tin sản phẩmTên sản phẩm, cấp loại, mẫu mã, ảnh nhãn mác hoặc mã tham chiếu của nhà cung cấp.
Các tài liệu có sẵnTDS, SDS, COA, ảnh mẫu, danh mục sản phẩm hoặc dữ liệu thử nghiệm.
Chi tiết đơn hàngSố lượng dự kiến, hình thức đóng gói, nước nhập khẩu, cảng hoặc điều kiện thương mại.
Yêu cầu hoặc Vấn đềQuy trình in trên vải, yêu cầu về công thức, vấn đề hiện tại hoặc chỉ tiêu hiệu suất.