Digital Printing Pretreatment Batch-to-Batch Consistency: Which QC Parameters Best Predict Print Performance?
Matching viscosity and pH does not guarantee consistent digital textile printing. Learn how to connect...
Matching viscosity and pH does not guarantee consistent digital textile printing. Learn which pretreatment QC parameters are useful release checks, which need validation as performance predictors, and how to connect incoming batches with application uniformity, color, definition, fastness and total cost.
Two deliveries of digital printing pretreatment can meet the same viscosity specification and still behave differently on the line. One may require longer preparation, leave more filter residue or produce a wider range of color across the fabric. Another may look satisfactory immediately after printing but fail the finished-fabric requirement after fixation and washing.
The most useful predictor is a validated combination of measurements that represents the actual process—not a single universal QC number. A controlled reference print is the most direct check of print performance under its test conditions. Faster measurements such as rheology, solids, pH, filtration and application behavior become reliable release tools only when their relationship to acceptable printing has been demonstrated for the relevant product and process.
This guide explains how to build that relationship. It covers supplied powders, concentrates and ready-to-use pretreatments, with separate priorities for reactive, direct disperse and pigment inkjet workflows. The objective is a practical batch-control program that detects meaningful changes without turning every delivery into an unnecessarily large research project.
Which QC Parameters Best Predict Print Performance?
Start by distinguishing direct performance evidence from indirect indicators. A finished reference print measures the outcome you care about, but only for the selected fabric, ink, application and finishing conditions. A quick liquid test can be easier to run on every batch, yet its ability to predict that outcome must be established.
Kiểm tra
Main value
Important limitation
Controlled finished reference print
Directly evaluates color, detail and required finished properties.
Does not automatically represent every production substrate or process.
Application uniformity and deposition
Shows how consistently the treatment reaches the fabric.
Cannot establish chemical compatibility or final fixation alone.
Process-relevant rheology and holding behavior
Detects flow and stability changes affecting preparation and application.
Must be connected to the actual application method.
Preparation and filtration performance
Reveals incomplete hydration, gels or operationally relevant residue.
A passing result does not establish shade or fastness.
Solids or moisture, pH and applicable chemical checks
Provides fast screening for composition or preparation differences.
Matching numbers can conceal differences in functional behavior.
Identity, appearance and traceability
Confirms the correct material and detects obvious abnormalities.
Necessary for control, but weak as standalone performance predictors.
This is a starting hierarchy for designing a program, not a statistically proven ranking for every pretreatment. A factory with spray-application interruptions may find filtration highly predictive of downtime. Another with unstable pickup may gain more from rheology and application mapping. Select the measurements that address the actual failure modes.
A strong specification therefore uses several layers: identity and composition screening, process-readiness checks, and a validated connection to finished fabric. Keep the number of routine tests manageable, but retain the critical ones even when a supplier’s certificate of analysis appears satisfactory.
Define the Product, Batch and Printing Route Before Comparing Results
Clarify what the supplied material is expected to do
A powdered polymer, a concentrated formulated pretreatment and a ready-to-use liquid need different preparation and release methods. A powder may depend on controlled hydration; a formulated liquid may require approved homogenization; a concentrate may need a precisely defined dilution.
Confirm whether the product is a rheology component or a complete treatment containing other functional ingredients. Do not infer its composition from the trade name. A complete-bath performance problem may arise from other additions even when the supplied polymer is unchanged.
Keep reactive, disperse and pigment requirements distinct
Printing route
Pretreatment evaluation priorities
Finished assessment
In phun phản ứng
Uniform application, compatibility with the intended alkali and auxiliaries, controlled ink movement
Color and detail after the approved fixation and wash-off route, plus required fastness and hand
Direct disperse inkjet
Ink localization on the specified polyester or blend and compatibility with the intended thermal process
Color, penetration, definition and required fastness after the specified finishing sequence
Mực in phun dạng bột màu
Ink reception, system compatibility, deposit distribution and binder-system performance
Color, dry and wet rubbing, required laundering, hand and layer integrity
Direct disperse printing on fabric is not the same evaluation as transfer printing onto paper. Likewise, pigment pretreatment should not be assessed by automatically importing reactive wash-off requirements. Use the intended route, including any required washing or clearing, rather than a generic finishing sequence.
Distinguish supplier batches from factory preparation batches
One supplier lot may be used in several factory mixes. Those mixes can differ because of water, weighing, mixing, holding or application. Record both identifiers. Otherwise, a preparation error may be reported as inconsistent manufacturing, or a real material shift may be hidden inside a single production-batch label.
Retain the commercial grade, supplier lot, package identifiers, document versions and sampling details. If a sample-stage product is later renamed or reformulated, require a documented link to the approved commercial material rather than assuming continuity from appearance alone.
Viscosity Is Useful Only When the Method and Process Are Defined
Make a single-point result reproducible
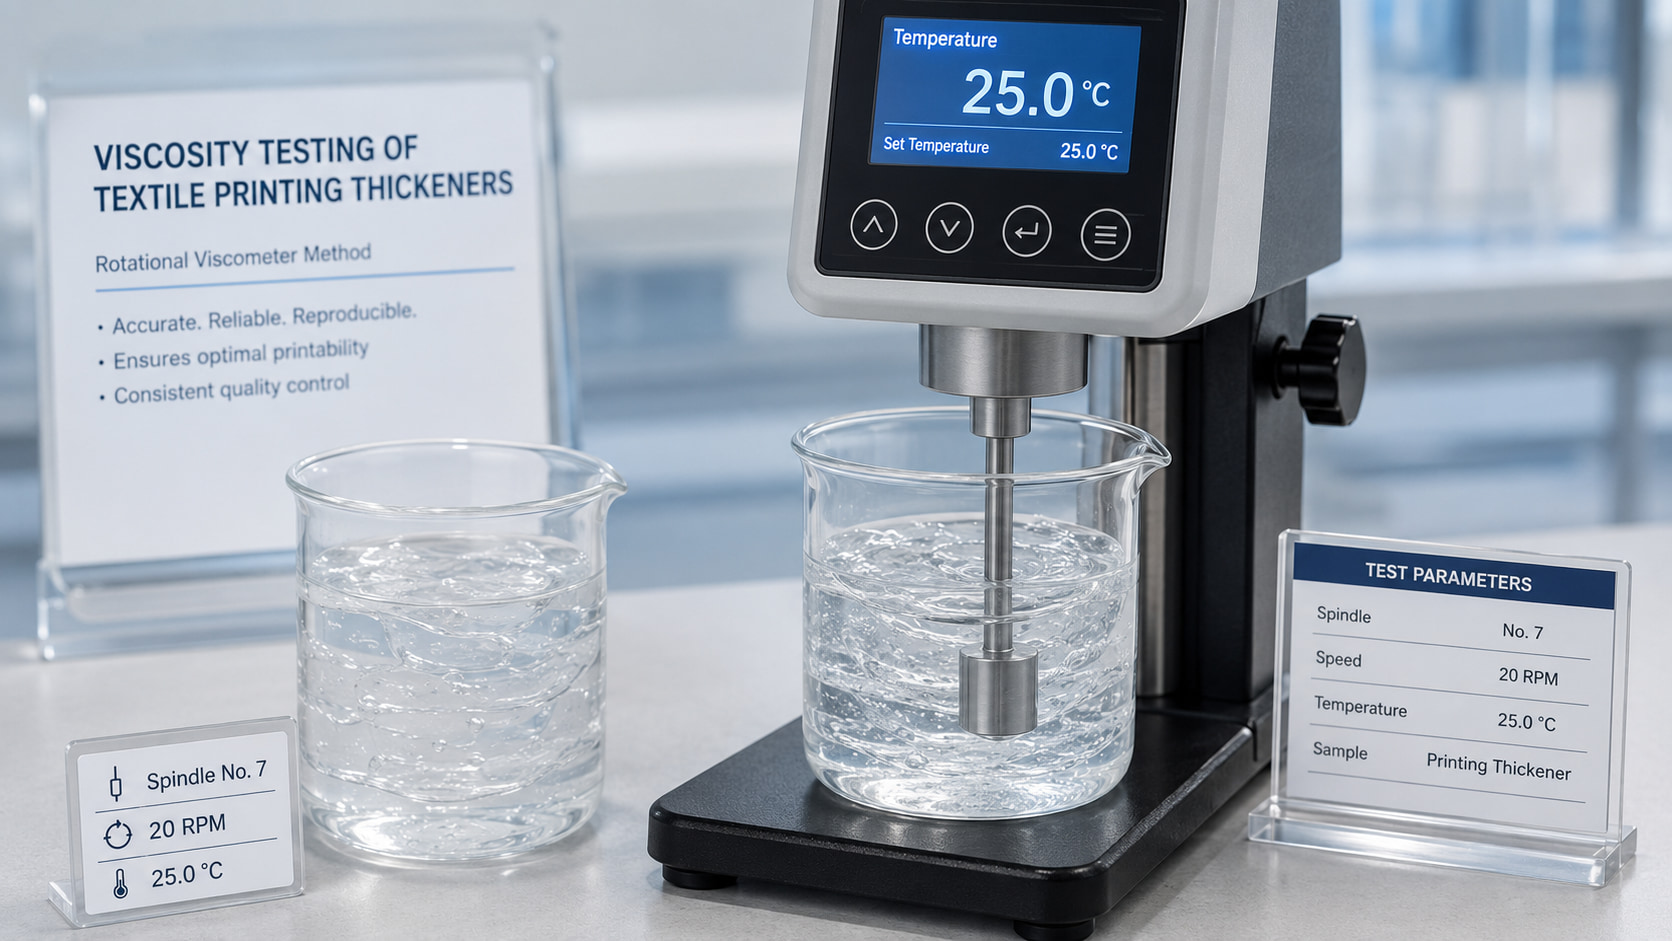
For a non-Newtonian sample, the measured apparent viscosity depends on the test conditions. Brookfield emphasizes matching conditions such as spindle, speed and temperature when comparing results. A viscosity number without those conditions is not a complete material specification. [1]
Define concentration and its calculation basis, water source, preparation order, mixing procedure, hydration time, sample temperature, instrument, geometry or spindle, container, immersion and reading time. Record the applicable instrument operating range and avoid accepting results obtained outside it.
Use the same sample history for each batch. A freshly mixed sample, a rested sample and a circulated sample may give different readings. Prevent evaporation during holding and allow appropriate temperature equilibration before measurement.
Use multiple conditions only when they answer a process question
Two materials can share the same apparent viscosity at one speed yet behave differently at another. A small, repeatable multi-speed sequence can help detect such differences. For time-dependent systems, a defined recovery or holding comparison may be more useful than adding many unrelated readings.
A viscosity ratio, including an internally defined PVI, must state the numerator and denominator, speeds, geometry, concentration, temperature and sequence. An inverted ratio is not comparable to the original convention. Different ratio definitions cannot be reconciled by comparing the label “PVI” alone.
Do not interpret rotational speed as a universally known shear rate for every spindle arrangement. Use geometry-appropriate methods if quantitative flow curves or yield behavior are needed. Routine comparative readings can still be useful when their limitations are understood.
Test the working bath as well as the supplied material
A clean-water polymer solution may be consistent while the completed pretreatment changes after required ingredients are added. Compare the working formulation at its intended dilution and holding condition. Record approved additives and their lots so that a batch effect can be distinguished from formulation drift.
Same viscosity does not mean same performance. Rheology can support control of application, but it does not prove equivalent wetting, residue, fixation, color yield or hand. For the broader measurement framework, see textile printing thickener testing parameters.
Solids, Moisture, pH and Conductivity: Fast Checks with Specific Limits
Solids or moisture helps control the delivered quantity
At a fixed supplied-product dosage, a concentration difference can change how much nonvolatile material reaches the fabric. For powders, moisture can affect the dry material delivered per kilogram. These checks are useful, but the reporting basis must match the intended interpretation.
Total solids, active polymer, binder content and loss on drying are not interchangeable terms. A drying method may remove substances other than water, while retained residue can include several ingredients. Define sample size, temperature, duration or endpoint and calculation method.
Compare lots first at the actual purchasing and dosing basis. If needed, a secondary solids-normalized trial can help investigate the source of a difference. Do not silently normalize every sample before testing, because that can hide a supplied-concentration problem that production would encounter.
pH is a useful process indicator, not a composition fingerprint
Specify whether pH is measured in the supplied liquid, a defined dilution or the completed bath. Use suitable calibrated equipment and consistent preparation. Different concentrations or water sources can make nominally similar measurements incomparable.
A pH shift may flag a preparation or material change. However, identical pH does not prove identical buffering, ionic composition or compatibility. Where buffering or another chemical function is important, a separately validated test may be needed rather than a tighter pH limit alone.
Conductivity is conditional, not universal
Conductivity can help detect ionic differences in a defined solution or working bath. Record concentration, temperature and water quality, and use the result only where it has a meaningful relationship to the formulation. A high value is not inherently worse than a low value.
Conductivity does not identify which ions are present or replace a specific chemical assay. A correlation established for one grade may not apply to a reformulated grade with a different ionic composition. Do not impose a universal conductivity target across reactive, disperse and pigment products.
Parameter
Can help detect
Does not prove alone
Moisture or solids
Delivered concentration differences
Functional polymer identity or location on fabric
pH
Acidity or alkalinity changes under a defined method
Complete formulation equivalence
Conductivity
Ionic changes in a comparable matrix
Specific salt identity or printing suitability
Density, where applicable
Some composition or dilution changes
Equivalent active content without calibration
Product-specific assay
The defined functional component or property
All downstream application and print outcomes
Preparation, Filtration and Holding Tests Often Reveal Hidden Batch Differences
Measure readiness at the time production needs it
A powder that reaches the required viscosity eventually may still be unsuitable if it does not prepare reliably within the factory’s normal schedule. Record dispersion, hydration, lump formation and the time at which the working bath becomes usable.
Follow the approved preparation sequence rather than forcing every product through an inappropriate method. For comparison within one grade, keep that sequence fixed. For a replacement grade needing a different method, document the difference and include its operational cost.
Filtration must represent the relevant equipment
Define filter material, opening, area, sample amount, driving pressure or gravity condition, temperature and endpoint. Record both throughput and retained material where useful. A fast pass through a coarse filter does not establish compatibility with a finer production application system.
Inspect the residue. Hydrated gel, undispersed powder, fibers and precipitated material suggest different investigations. A dry-residue mass alone can conceal those distinctions, while a visual description without a standardized sample amount is difficult to compare.
Keep the pretreatment route separate from the ink circuit. An offline padding bath is not necessarily required to meet the same filtration conditions as an inkjet ink. If pretreatment is itself jetted, use the relevant equipment supplier’s requirements; do not assume that a general paste is suitable for that delivery system.
Evaluate the permitted production holding period
Compare the prepared bath after full readiness and after a representative permitted hold or circulation period. Check flow behavior, separation, residue, foam and subsequent application. A stable fresh sample does not establish stable end-of-shift behavior.
Distinguish unopened product shelf life from prepared-bath working life. Accelerated storage can be a screening tool, but its connection to real storage must be validated before it supports a shelf-life claim. Do not infer microbial status from odor or viscosity loss alone.
Foam belongs in the application test when it affects delivery
Use a mixing or circulation condition relevant to the factory. Record both foam generation and persistence rather than a single visual observation. Trapped air can interfere with measurements and deposition, but adding defoamer without identifying the cause introduces another variable.
These readiness checks deserve routine priority when historical failures involve filters, delayed preparation or uneven coating. Their value is strongest when the records connect them with actual downtime or print defects.
Application Uniformity Connects Liquid QC with the Printed Surface
A passing liquid sample can still produce a failing textile if application varies. Include a controlled laboratory application or a verified production check in the validation program. Record applied quantity and spatial uniformity, not only the bath concentration.
Use a deposition measure suited to the route
For padding, wet pickup is often useful when measured against a consistent dry reference. For spraying, liquid delivered per known area may be more relevant. A validated dry-add-on method can provide another view, although it usually measures total retained material rather than a specific active component.
Keep fabric mass, face and orientation consistent. Across different fabric weights, percentage add-on and grams per square meter answer different questions. Record both where they help interpret deposition and cost.
Assess wetting on the intended substrate
A repeatable drop or spreading comparison can help screen receiving-surface behavior. Specify the liquid, volume, timing and conditioning. Water is useful for some comparisons but does not reproduce every property of the actual ink.
Surface tension measured in the bath also cannot, by itself, predict the complete fabric response. Porosity, finishes and yarn construction affect transport. Research on polyester pigment printing has demonstrated the relevance of pretreatment and fabric surface characteristics, supporting control of the substrate in batch comparisons. [2]
Watch the width and the run
Map relevant width positions and production times. An average pickup can hide a poorly treated edge, and a center cutting can miss a spray-overlap defect. Record locations so the application map can be compared with shade and fastness results.
When the control lot and candidate lot both fail in the same lane, investigate shared application or drying conditions before blaming the new batch. When only the candidate shows a reproducible change under the same controlled route, the material difference deserves closer examination.
Build a Reference Print That Is Sensitive and Repeatable
Choose a stable reference system
Retain an approved pretreatment lot within its validated storage period and use a characterized reference fabric. Record ink identity, printer condition, artwork version, application level and processing sequence. Run the control beside the candidate where practical to expose day-to-day process variation.
A reference chemical or fabric is not permanent. Plan replacement before stocks are exhausted or aged. Bridge old and new references through overlapping comparisons, and investigate any step change instead of treating a new reference as automatically equivalent.
Use a compact test image with relevant challenges
Include solid colors, representative dark combinations, fine positive lines, negative gaps and adjacent color boundaries. Add white-underbase areas only where the intended system uses them. Select features that reveal known failure modes rather than relying on a visually attractive photograph alone.
Measure finished color using a consistent instrument setup, backing, orientation and conditioning. Specify the color-difference formula and viewing conditions where relevant. Reflectance-based color strength is useful under controlled comparisons, but it is not a direct chemical fixation measurement across unrelated fabrics.
Finish the sample through the intended route
For reactive printing, approval should reflect the specified fixation and wash-off. For direct disperse printing, follow the intended thermal and aftertreatment sequence. For pigment printing, verify the binder system’s curing and required durability tests. A favorable pre-fixation appearance is not sufficient.
Pigment research has shown that stronger surface color and rubbing performance need not move together. Ding and colleagues associated low crockfastness in investigated pretreated samples with higher surface pigment levels. This supports separate color and durability endpoints rather than one combined appearance score. [3]
Output
Record
Color and uniformity
Defined patches, instrumental setup, location and comparison with the reference
Definition
Line growth, open gaps, boundary spread and consistent image capture
Fastness
Agreed methods, specimen condition and individual results
Hand and appearance
Approved comparison, treatment marks and printed-area feel
Processing
Preparation, application, thermal or steaming records and relevant washing
Operational behavior
Filter changes, interruptions, foam and other production-relevant observations
Dry and wet rubbing are distinct checks, and neither substitutes for laundering. AATCC TM8 provides controlled rubbing procedures and recognizes the influence of subsequent treatments. Use the agreed complete method rather than copying a few settings into an informal test and calling it equivalent. [4]
How to Determine Which Quick Tests Actually Predict Performance
First establish that the measurements can detect meaningful differences
Repeat testing on the same material and compare operators or days where relevant. If measurement variation is similar to the difference being used for release, the decision will be unreliable. Instrument calibration alone does not eliminate sample-preparation or operator variation.
NIST’s measurement-process guidance treats repeatability, reproducibility, stability and uncertainty as distinct considerations. Use that framework to assess the complete method, including sampling and preparation, rather than relying only on the instrument’s stated precision. [5]
Build paired lot and performance records
For each independent material lot, connect QC results with a controlled print result and relevant production observations. Keep factory mix identifiers beneath the supplier-lot identifier. Several cuttings from one lot are useful replicates, but they are not several independent manufacturing batches.
Include normal commercial variation and relevant borderline cases when available. A dataset containing only narrowly similar passing batches may show little relationship simply because it lacks informative variation. Do not deliberately release suspect material to production to create failure data; use controlled evaluation.
Separate confounding factors
If every new material lot is printed on a different fabric or after a printer adjustment, batch and process effects are tangled. Pair candidates with a reference under comparable conditions. Record unavoidable differences so they are not mistaken for a material relationship.
Analyze reactive, disperse and pigment routes separately unless there is a defensible reason to combine them. The same applies to substantially different substrates and application methods. A useful relationship within one process can disappear or become misleading when incompatible datasets are pooled.
Validate on Later Independent Lots Before Reducing Print Tests
Choose the proposed QC rule using a development set, then keep later independent lots for confirmation. Cuttings, repeat readings or several factory mixes from one supplier lot should not be counted as independent manufacturing lots. Keep all results from one lot together when assessing a rule; otherwise nearly identical material can appear on both sides of the validation.
QC decision
Finished-print outcome
What to investigate
Pass
Pass
Evidence supporting the rule within the tested process scope
Pass
Fail
A missed failure: investigate the missing predictor or a process confounder
Hold
Pass in controlled evaluation
A possible unnecessarily restrictive rule or measurement problem
Hold
Fail
Whether the same failure mechanism repeats on independent lots
Define finished-print acceptance before examining the candidate QC limits. Record the number of lots in each outcome, not just a correlation coefficient. A strong correlation in a narrow dataset does not prove that the rule catches the failure that matters, and a dataset with no relevant failures cannot establish failure-detection performance.
Keep the initial rule and subsequent changes traceable. Investigate false passes before reducing direct application checks; do not change the threshold after each result simply to make the record look better. A change in ink, substrate, deposition method or finishing route can invalidate a previously useful relationship. Continue periodic reference printing after routine release has been simplified.
Set Release Rules That Connect the COA with Actual Use
Separate qualification, routine release and periodic verification
Qualification establishes suitability across representative conditions and independent batches. Routine release uses the agreed critical checks for each incoming lot. Periodic verification confirms that the relationship between those checks and printing remains valid.
Increase verification after a supplier change, reformulation, new substrate, new application route or unexplained failure. A stable history may support a reduced routine panel, but the change should be documented and backed by evidence rather than cost pressure alone.
Do not confuse specification limits with control limits
Specification limits define agreed acceptance requirements. Statistical control limits describe expected behavior of a monitored process under the chosen chart assumptions. NIST explains control charts as tools for detecting changes in process behavior; they are not interchangeable with customer tolerances. [6]
A lot can be within specification while part of an unusual trend that deserves investigation. A stable process can also consistently produce material outside a customer’s requirement. Do not calculate a control band and automatically adopt it as the purchasing specification.
Use clear hold and investigation rules
Check identity and sample integrity. Confirm the lot, preparation and test method.
Verify the measurement. Follow a predefined repeat procedure without selectively discarding unfavorable results.
Compare the retained reference. Determine whether the test system itself has shifted.
Investigate the relevant failure mode. Use application or print checks to resolve the uncertainty.
Record the disposition. Release, hold or reject according to the agreed decision authority and evidence.
Close the cause. Update controls when a recurring issue shows a gap in the existing program.
A strong average score should not cancel a critical failure such as unacceptable fastness or serious application instability. Use hard acceptance gates for essential requirements; use weighted comparisons only among candidates that meet those gates.
Make the COA useful
Request actual batch results for agreed parameters, units, limits and method identifiers. Distinguish measured batch values from typical TDS values. Where the method is held in a separate specification, ensure both parties use the same revision.
Retain representative material according to a documented sampling and storage plan. Avoid a composite sample that conceals package-to-package variation when that variation is the concern. Agree how damaged packages or separated liquids are sampled rather than homogenizing away evidence before investigation.
Connect Batch Consistency with Total Cost in Use
Consistency has commercial value when it reduces adjustments, interruptions, rework and rejected output. Track those outcomes alongside the chemical specification. A low-priced material that repeatedly needs emergency dosing changes may not provide a low production cost.
Cost per accepted meter = consistently defined production costs ÷ meters meeting the complete specification. Use accepted garments where appropriate. Include relevant pretreatment and ink consumption, energy, labor, testing, downtime, rework and reject costs without double-counting.
Compare lots at the same finished requirements. A deeper shade obtained through more ink, or a passing rubbing grade obtained through a slower thermal process, should carry the associated consumption and throughput consequences in the comparison.
The goal is a small, effective QC panel supported by periodic direct evidence. Remove tests that add no useful decision information only after validation, and add tests when documented failures expose an unmonitored risk. This makes QC a production-control tool rather than a collection of numbers on a certificate.
Các câu hỏi thường gặp
1. What is the single best QC test for digital printing pretreatment?
No single quick test predicts every outcome. A controlled finished reference print provides the most direct evidence for its defined conditions. Routine release should combine validated process indicators with the checks needed for critical failure modes.
2. Can matching viscosity guarantee batch consistency?
No. Similar viscosity can coexist with differences in wetting, residue, composition or holding behavior. The method must be identical, and the result must be connected to application and finished-fabric performance.
3. Should viscosity be measured in water or in the working bath?
Both can be useful. A defined water preparation supports material comparison, while the working bath tests behavior with the actual permitted additions. State which result appears on the specification and why.
4. Is total solids the same as active polymer content?
No. Total solids can include several nonvolatile ingredients. Use the correct assay and reporting basis if a specific active component is the intended control parameter.
5. Does conductivity predict print quality?
Only where a validated relationship exists for the defined formulation and method. It can reveal ionic differences but does not identify the ions or establish universal printing suitability.
6. Should every batch receive a full printing trial?
That depends on the maturity of the control program and the consequences of failure. Qualification and uncertain situations need stronger direct verification. A reduced routine panel requires evidence and ongoing periodic confirmation.
7. How many batches are needed to validate consistency?
There is no universal number. Use independent lots representing relevant variation and verify performance on later lots. Repeated specimens from one batch improve repeatability estimates but do not demonstrate manufacturing consistency across batches.
8. Why can a COA-passing batch still print poorly?
The tested parameters may not cover the failure, the methods may differ, or the factory process may have changed. Compare the lot with a retained reference under controlled preparation, application and finishing conditions.
9. Should reactive and pigment pretreatments share QC limits?
Not automatically. They serve different ink chemistries and finishing routes. Share a general control framework, but establish product- and process-specific methods, limits and finished endpoints.
10. Can a retained reference batch be used indefinitely?
No. Its storage stability and usable life must remain valid. Replace it through an overlapping comparison so a change in reference does not create an unexplained shift in acceptance.
11. Should an out-of-specification result simply be retested?
Follow an agreed investigation procedure. Check sampling, preparation and measurement, retain all relevant results, and avoid repeated testing until a passing number appears.
12. What should a buyer request before first bulk supply?
Request the agreed grade, method-linked specification, representative batch COA, preparation instructions and a sample-to-production validation plan. Begin with the actual ink, fabric and application route so the requirements remain relevant.
Agree a Useful Pretreatment QC Package with FSX Chemical
FSX Chemical’s digital printing pretreatment range can be evaluated against the intended ink chemistry, fabric and application method. A useful supplier comparison begins with agreed methods and finished-performance targets, then connects those targets with practical batch controls.
Through the sample matching service, share your current TDS or QC specification and the main consistency problem. Start with the ink system, fabric and application route; the trial can then focus on the measurements most likely to explain the difference.
Liên hệ với FSX Chemical to discuss sample evaluation, method alignment and batch documentation. Confirm the selected product through laboratory comparison and representative production, assessing color, definition, fastness, hand and Total Cost in Use together.📧 Email: Service@fsxchemical.com
Tìm hiểu lý do tại sao không thể so sánh các giá trị độ nhớt của chất làm đặc trong in ấn dệt may nếu không đảm bảo các yếu tố như nồng độ, nhiệt độ, thiết bị, trục quay, tốc độ, phương pháp chuẩn bị và thời gian thử nghiệm đều giống nhau.
Tìm hiểu cách đánh giá một nhà sản xuất chất làm đặc dùng trong in ấn dệt may bằng cách kiểm tra thông tin nhận diện doanh nghiệp, năng lực sản xuất, phương pháp thử nghiệm, khả năng truy xuất nguồn gốc lô hàng, tài liệu kỹ thuật, hỗ trợ mẫu thử và khả năng cung ứng xuất khẩu.
Việc hiểu rõ nguồn gốc nguyên liệu và quy trình sản xuất natri alginat sẽ giúp các đội ngũ mua hàng đặt ra những câu hỏi phù hợp hơn và đánh giá nhà cung cấp hiệu quả hơn. Cẩm nang này đề cập đến các loài tảo biển, các bước chiết xuất, nguồn gốc của tạp chất, cũng như những tiêu chí về quy trình sản xuất nhất quán cần có trong hồ sơ của nhà cung cấp.
Việc bảo quản không đúng cách là một trong những nguyên nhân phổ biến nhất dẫn đến các vấn đề về hiệu suất của natri alginat trong in ấn dệt may. Hướng dẫn này đề cập đến các điều kiện bảo quản dạng bột và dạng bột nhão, thời hạn sử dụng dự kiến, các dấu hiệu suy giảm chất lượng, cũng như những điều cần kiểm tra khi nhận hàng mới.
Các bảng dữ liệu kỹ thuật (TDS) có sự khác biệt về định dạng và mức độ đầy đủ giữa các nhà cung cấp, và không phải mọi trường thông tin đều có tầm quan trọng như nhau đối với mọi ứng dụng. Hướng dẫn này sẽ phân tích chi tiết từng phần của một bảng dữ liệu kỹ thuật (TDS) điển hình về natri alginat, giải thích ý nghĩa của từng thông số và cách nhận diện những thiếu sót hoặc dấu hiệu cảnh báo.
Nhiều nhà cung cấp quảng cáo sản phẩm "alginat natri tùy chỉnh", nhưng trên thực tế, thuật ngữ này lại bao hàm những khái niệm rất khác nhau. Hướng dẫn này sẽ giải thích những thông số nào thực sự có thể điều chỉnh, những thông số nào bị giới hạn bởi các quy luật hóa học cơ bản, và cách đánh giá các tuyên bố về khả năng tùy chỉnh của nhà cung cấp.
Khi xuất hiện lỗi in trên sàn, thách thức đặt ra là phải nhanh chóng xác định nguyên nhân. Cẩm nang tham khảo này phân loại các lỗi thường gặp liên quan đến hỗn hợp natri alginat theo triệu chứng, trong đó các nguyên nhân có khả năng xảy ra được xếp hạng theo mức độ khả năng và kèm theo các bước kiểm tra ban đầu thực tế cho từng trường hợp.
Việc mua sỉ natri alginat không chỉ đơn thuần là so sánh giá đơn vị. Hướng dẫn này giải thích cách các nhà mua hàng trong lĩnh vực in ấn dệt may có thể xác minh độ nhớt, kích thước mắt lưới, cấp độ tinh khiết, bao bì, chứng nhận phân tích (COA), kiểm tra mẫu và tính đồng nhất giữa các lô hàng trước khi đặt hàng số lượng lớn.
Giá alginat natri có sự chênh lệch đáng kể giữa các nhà cung cấp và các loại sản phẩm, nhưng không phải mọi sự chênh lệch về giá đều phản ánh sự khác biệt thực sự về chất lượng. Hướng dẫn này giải thích các yếu tố ảnh hưởng đến chi phí, cách so sánh báo giá trên cơ sở tương đương và những dấu hiệu cảnh báo cần lưu ý khi đánh giá các đề xuất của nhà cung cấp.
Một bản báo giá alginat natri hữu ích cần bao gồm các nội dung sau: ứng dụng, phương pháp kiểm tra độ nhớt, phê duyệt mẫu, tính nhất quán giữa các lô hàng, đóng gói, tài liệu, Incoterms và các điều khoản thương mại. Danh sách kiểm tra này giúp người mua trong lĩnh vực in ấn dệt may chuẩn bị một yêu cầu báo giá (RFQ) đầy đủ trước khi so sánh các nhà cung cấp.
Chất lượng ổn định của hóa chất dệt may phụ thuộc vào việc kiểm soát nguyên liệu thô, quy trình sản xuất có thể lặp lại, các phương pháp thử nghiệm được quy định rõ ràng, việc kiểm tra lô thành phẩm, khả năng truy xuất nguồn gốc và quá trình xác minh của khách hàng. Hướng dẫn này giải thích cách FSX Chemical kết nối các biện pháp kiểm soát này từ khâu lựa chọn mẫu đến khâu vận chuyển số lượng lớn.
Để quản lý độ nhớt hiệu quả, không chỉ đơn thuần là đạt được một con số mục tiêu. Hướng dẫn này giải thích cách các phương pháp thử nghiệm, nhiệt độ, nồng độ, độ ngậm nước, lực cắt, hóa chất, điều kiện bảo quản và sản xuất ảnh hưởng đến hiệu suất của bột in dệt.
Vui lòng cung cấp tên sản phẩm, ứng dụng, số lượng, điểm đến và bất kỳ tài liệu kỹ thuật (TDS),
hình ảnh mẫu hoặc tài liệu nào mà quý khách đã có. FSX Chemical sẽ xem xét
thông tin này và đề xuất bước tiếp theo liên quan đến báo giá, đối chiếu mẫu
hoặc lựa chọn sản phẩm.
Thông tin sản phẩmTên sản phẩm, cấp loại, mẫu mã, ảnh nhãn mác hoặc mã tham chiếu của nhà cung cấp.
Các tài liệu có sẵnTDS, SDS, COA, ảnh mẫu, danh mục sản phẩm hoặc dữ liệu thử nghiệm.
Chi tiết đơn hàngSố lượng dự kiến, hình thức đóng gói, nước nhập khẩu, cảng hoặc điều kiện thương mại.
Yêu cầu hoặc Vấn đềQuy trình in trên vải, yêu cầu về công thức, vấn đề hiện tại hoặc chỉ tiêu hiệu suất.