Synthetic Thickener Rheology for Textile Screen Printing: Shear Thinning, Recovery and Print Definition
Synthetic thickener performance in screen printing depends on more than static viscosity. The useful rheology...
Synthetic thickener selection for textile screen printing should be based on rheology, not on one viscosity number. A printing paste is almost stationary in the color kitchen, experiences moderate shear during pumping, much higher shear under the squeegee and through the screen, then returns to low shear after it reaches the fabric. The thickener therefore needs enough low-shear body to control spreading, enough shear thinning to pass through the screen, and enough structural recovery to rebuild the pattern after transfer. If recovery is too slow, the print can bleed or lose definition; if recovery is too fast or elasticity is too high, poor leveling, stringing or mesh marks can appear. This guide explains how to evaluate synthetic-thickener rheology for textile flat and rotary screen printing and connect laboratory measurements with actual print definition.
What Rheology Should a Synthetic Thickener Provide?
A useful synthetic thickener for textile screen printing should generally provide three linked behaviors:
High Enough Structure at Low Shear → Lower Apparent Viscosity Under Printing Shear → Controlled Structural Recovery After Transfer
These three behaviors help the paste:
Remain stable in the tank
Move through pumps and pipes
Pass through the screen under squeegee force
Deposit evenly on the fabric
Recover enough structure to limit spreading
Maintain edge definition until drying begins
The best grade is therefore not the synthetic thickener with the highest measured viscosity.
It is the grade with the most useful flow-and-recovery profile for the actual screen, machine, fabric and pigment-binder formula.
Why One Viscosity Number Is Not Enough
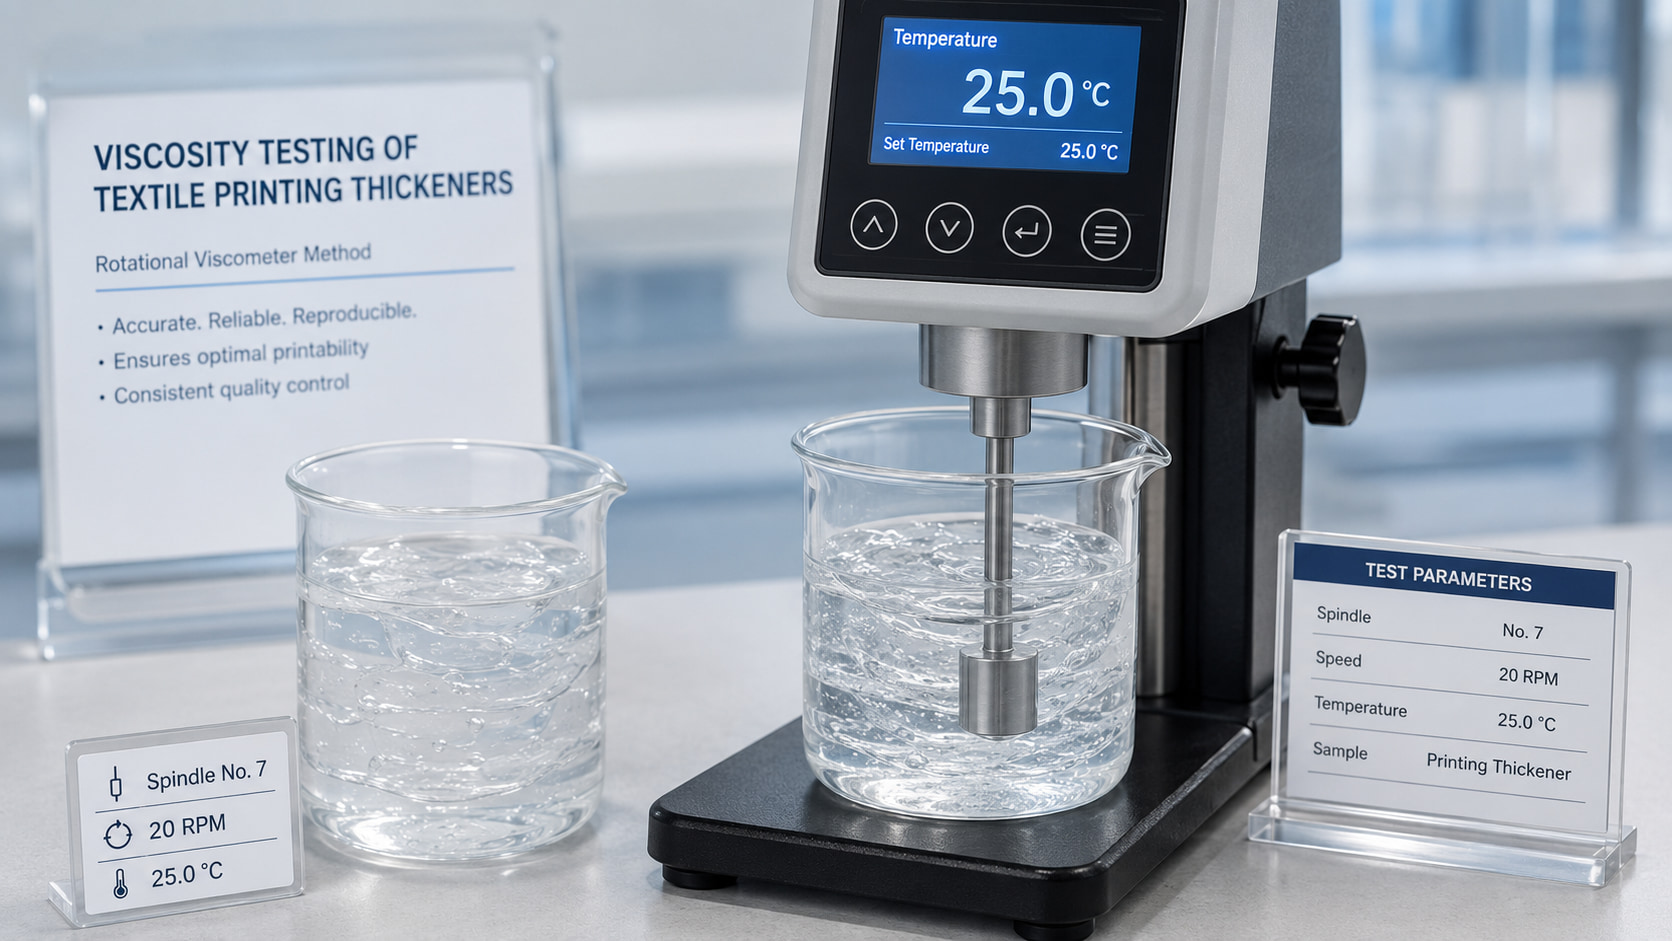
A Brookfield or rotational-viscometer value normally represents one specific measurement condition.
For example:
30,000 mPa·s at one spindle, one RPM and one temperature
does not tell the mill how the paste behaves at much higher shear under the squeegee.
Research on rotary-screen printing parameters examined paste rheology together with screen mesh and machine settings. For a mill trial, assess these jointly rather than assigning every defect to the thickener. Relevant outcomes include:
Screenability
Paste flow through screen openings
Penetration into fabric
Print sharpness
ფერის გამოსავლიანობა
თანაბარობა
Two pastes with the same low-shear viscosity can therefore give different printing results if they differ in:
Shear-thinning rate
Recovery speed
ელასტიურობა
Yield stress
Thixotropy
Same viscosity does not mean same rheology.
The Screen-Printing Shear History Map
The printing paste experiences several mechanical environments during one production cycle.
Process Stage
Relative Shear Condition
Rheology Requirement
Tank / Rest
Low
Body, stability, anti-settling
Pumping / Circulation
Low to medium
Easy flow without permanent breakdown
Squeegee Movement
Medium to high
Strong shear thinning
Screen Opening
High
Low enough apparent viscosity for transfer
Fabric Deposit
Rapidly falling
Controlled recovery
Before Drying
Low
Enough structure to limit spreading
The map is a qualitative process guide, not a measured shear-rate profile for a machine. Speed-dependent flow and time-dependent rebuilding need separate tests; an instantaneous viscosity rise after speed reduction alone does not prove thixotropic recovery.
This is why rheology must be evaluated as a curve and a recovery process rather than one point.
1. Low-Shear Body: Holding the Paste Before and After Printing
At low shear, the printing paste needs enough structure to remain stable and resist uncontrolled flow.
Low-shear body helps control:
Pigment distribution
Binder distribution
Spreading after printing
ნაკვთში შეღწევა
ზუსტი განსაზღვრა
If low-shear structure is too weak, possible symptoms include:
Bleeding
Haloing
Loss of fine detail
Excess penetration
არათანაბარი მყარი ადგილები
But excessive low-shear viscosity can create:
Difficult pumping
Poor screen filling
High squeegee pressure requirement
The target is sufficient structure—not maximum structure.
2. Shear Thinning: Helping Paste Pass the Screen
Most useful screen-printing pastes are pseudoplastic or shear-thinning.
As shear rate increases, apparent viscosity decreases.
This behavior allows the paste to:
Move more easily under the squeegee
Pass through screen openings
Transfer to the textile with lower mechanical resistance
A strongly shear-thinning paste can have high body at rest and still flow efficiently during printing.
This combination is one reason synthetic polyacrylate thickeners are useful in selected textile-printing systems.
If shear thinning is too weak:
Screen passage can be poor.
Pressure may need to increase.
Transfer can become incomplete.
If shear thinning is too strong:
Paste can become excessively fluid under the squeegee.
Penetration can become too deep.
Recovery demand becomes more important.
3. Structural Recovery: Rebuilding After the Screen
When the paste exits the screen, the high shear condition disappears.
The thickener should rebuild enough structure to stabilize the deposit.
This is structural recovery.
Recovery helps control:
Pattern edge sharpness
Dot or fine-line stability
Surface spreading
შპალერის გასწორება
შეღწევა
Polyacrylate-based printing systems can show rapid recovery after shear, but the exact rate depends on the grade and formula.
A useful synthetic thickener should therefore be evaluated for both:
Viscosity Loss Under Shear
and:
Viscosity / Structure Recovery After Shear
What Happens When Recovery Is Too Slow?
Slow recovery leaves the paste too fluid after transfer.
Possible results include:
Bleeding
Edge spreading
Loss of fine lines
Excess fabric penetration
Lower surface color concentration
In this case, simply increasing low-shear viscosity may not be the best correction.
A grade with faster recovery can sometimes improve definition without making pumping or screen transfer excessively difficult.
What Happens When Recovery Is Too Fast?
Very fast recovery can also create problems.
If the paste rebuilds structure immediately after passing the mesh, it may have insufficient time to level.
Possible symptoms include:
Mesh marks
არათანაბარი მყარი ადგილები
Surface texture
Poor leveling
If mesh marks remain, compare leveling with a controlled recovery test and check screen tension, stencil and release settings. The defect alone does not establish that recovery is too fast.
The objective is therefore a controlled recovery window.
4. Elasticity and Stringiness
Synthetic printing pastes are often viscoelastic.
This means they show both liquid-like and elastic behavior.
Elastic deformation and time-dependent structural rebuilding are different phenomena; an elastic response alone does not establish the recovery curve.
A visually thick paste can still release poorly. Record filament or tail defects under fixed lift and screen conditions, but do not report an elastic modulus from that visual observation.
5. Yield Stress and Rest Stability
Some synthetic-thickener systems develop an apparent yield stress.
Below this stress, the paste resists flow.
Above it, the paste begins to move more readily.
A useful yield-stress region can support:
Rest stability
Anti-settling behavior
Pattern control after transfer
But excessive yield stress can make pumping and screen transfer difficult.
Yield stress should therefore be interpreted together with shear-thinning and recovery behavior.
6. Thixotropy and Time-Dependent Rheology
Thixotropy concerns time-dependent structural breakdown under shear and rebuilding afterward. Shear thinning is dependence on shear rate; a two-speed viscosity ratio by itself does not quantify recovery.
A thixotropic paste can become thinner during sustained shear and gradually rebuild when shear stops.
This matters in production because:
High-speed mixing can reduce viscosity temporarily.
Pumping can continue to shear the paste.
Rotary-screen circulation exposes paste to repeated shear.
Rest periods allow recovery.
Therefore, viscosity should be measured after a defined shear history and a defined recovery time.
Otherwise, the same paste can produce different laboratory readings depending on when the sample was taken.
Why Synthetic Thickener Architecture Matters
“Synthetic thickener” includes several polymer architectures.
Therefore, rheology should be measured on the actual commercial grade rather than inferred from the generic word “acrylic.”
Pigment and Binder Can Change the Rheology
Water-only rheology is not the final printing rheology.
Pigment dispersion and binder can change:
pH
Electrolyte level
Surfactant balance
Solids
Polymer interaction
This can alter shear thinning, recovery and elasticity even when the final Brookfield viscosity looks acceptable.
For pigment-printing grades, measure rheology in the complete:
Pigment + Binder + Thickener + Fixer + Auxiliary
სისტემა.
Flat Screen: What Rheology Usually Matters Most?
Flat-screen printing exposes the paste to intermittent squeegee strokes and dwell periods.
Important properties include:
Low-shear hold during pauses
Flow during the squeegee stroke
Recovery after transfer
Resistance to screen drying
Repeatable behavior after restart
A paste that recovers too slowly may spread during the dwell period.
A paste that becomes too structured during pauses may require increased pressure on restart.
Flat-screen qualification should therefore include pause/restart testing.
Rotary Screen: What Rheology Usually Matters Most?
Rotary-screen printing is continuous and places stronger emphasis on repeated shear and long-run stability.
Important properties include:
Pumpability
Continuous-shear viscosity
Recovery after screen transfer
Foam control
Mid-run stability
End-run stability
A paste that prints well for the first few meters but progressively thins during circulation has not passed rotary production qualification.
Screen Mesh and Open Area
Finer screen openings increase sensitivity to:
High-shear viscosity
Gel particles
Elastic stringing
Filtration quality
A more open screen can increase paste deposit and penetration.
ამიტომ:
Fine Mesh ≠ Automatically Lower Viscosity
and:
Open Mesh ≠ Automatically Higher Viscosity
The complete rheological profile must be matched to screen geometry.
Squeegee Pressure, Speed and Angle
Squeegee settings change both mechanical force and shear history.
Higher pressure or faster movement can increase the shear applied to the paste and change:
Apparent viscosity during transfer
Paste deposit
შეღწევა
ნიმუშის განმარტება
If a paste requires unusually high squeegee pressure to transfer, the problem may be insufficient high-shear flow rather than inadequate low-shear viscosity.
Machine settings and rheology should therefore be diagnosed together.
Penetration vs. Surface Color
Rheology controls where the paste goes after it reaches the fabric.
Too little penetration can produce:
Surface-heavy print
Uneven coverage on some fabrics
Too much penetration can produce:
Lower surface color concentration
Reduced edge sharpness
Higher reverse-side show-through
The optimum penetration depends on:
Fabric weight
Construction
შთამნთქმელობა
Print design
Pigment / binder system
The thickener should therefore control both screen transfer and post-transfer penetration.
A decrease in apparent viscosity with speed is consistent with shear thinning under that method. Control the dwell time and shear history: time-dependent drift during the speed sequence can also change the readings.
Keep one defined geometry where practical and use valid torque readings. For standard spindles without a specified shear-rate conversion, label the horizontal axis RPM; do not invent shear rates or combine different spindle geometries as one absolute flow curve.
The method must remain repeatable.
Run a Simple Shear-Recovery Test
A practical laboratory test can compare:
Initial viscosity after standard rest.
Viscosity immediately after a controlled high-shear mixing step.
Viscosity after a short recovery period.
Viscosity after a longer recovery period.
ჩანაწერი:
Apparent-Viscosity Recovery at Time t (%) = Viscosity at t after the defined shear step ÷ Initial Viscosity × 100
Use the same low-speed reading method before and after the shear step. Record the elapsed transfer, instrument-switching and reading times; a first result obtained after a delay cannot be described as immediate recovery.
The useful recovery profile is the one that gives good screen transfer and print definition.
Separate Speed Dependence from Time Dependence in the Test Record
A normal mill viscometer can support useful comparisons if the question is narrow. The following is a proposed test-design card, not a standard method or a measured FSX performance claim. Select speeds, durations and acceptance windows from instrument capability and the approved paste, then keep them fixed.
Question
Controlled comparison
What the result does not establish
Does apparent viscosity change with rotational speed?
Use the same full paste, temperature and geometry at defined speeds and dwell times; log each reading, elapsed time and torque
An exact machine shear rate, yield stress, or time-dependent recovery
Is the paste drifting while the test runs?
Use a matched aliquot held at the original low-speed conditions for the same elapsed time, without the high-speed challenge
That any drift must be a polymer-batch problem; check temperature, evaporation, air and preparation history
How does the paste return after the challenge?
Record a low-speed baseline, a defined high-speed interval and return to the original low-speed conditions; log elapsed time from the end of the challenge
Recovery before the instrument’s first valid reading, or a universal percentage needed on every screen
Why does the paste string during release?
Compare registered lift or screen-release observations using fixed gap, motion, paste age and surface conditions
A measured elastic modulus or a specific molecular cause
Keep the raw record. Include the formulation and solids basis, water, preparation/rest history, container and immersion conditions, instrument/spindle, speed sequence, torque, temperatures and actual timestamps. A low/high-speed viscosity ratio is a method-specific speed-response index. It should not be relabeled as proof of thixotropy.
Check recovery against a time control. A paste that stays thin after a challenge may have slow rebuilding, irreversible change or another uncontrolled variable. Extend the observation only within the qualified sample-storage window and investigate the controls before naming a mechanism. If geometry, slip or instrument timing limits the result, report that limit and use a suitable rheometer or a controlled print trial for the unresolved question.
Connect the measurement card to the print: use the same fabric, screen and application settings, record deposited mass, edge definition and restart behavior, then compare finished hand and fastness. A laboratory curve alone does not approve a production route. See synthetic printing thickener grade selection and use sample matching with the current TDS, test record and observed defect.
What a Rheometer Can Add
A rheometer can provide deeper information such as:
Flow curve
Yield stress
Up/down flow-loop response, interpreted with the ramp and hold times; this alone does not quantify recovery
Storage modulus (G′)
Loss modulus (G″)
Recovery after controlled shear
These measurements can help distinguish two pastes that look identical in a single-viscosity test.
However, rheometer data should still be connected to actual screen printing.
The most sophisticated rheology curve has little production value if it is not correlated with transfer, penetration and definition.
Define an Approved Rheology Window
Do not approve one perfect laboratory value.
Define a working window that includes:
Low-shear viscosity range
High-shear response
Recovery behavior
Holding-time stability
Screen-transfer result
Print-definition result
The working window should remain acceptable across:
Normal temperature variation
Expected pigment loading
Approved binder level
Expected production holding time
This makes the specification useful for actual manufacturing rather than one ideal lab condition.
წარმოების საცდელი დამტკიცება
Laboratory rheology is only the screening stage.
During a controlled production trial, record:
Thickener grade and batch
დოზირება
Complete paste formula
Start viscosity
Mid-run viscosity
End-run viscosity
Machine speed
Screen / squeegee settings
ნიმუშის განმარტება
შეღწევა
Beginning-to-end shade
Finished hand and fastness
A candidate should pass a production window, not one short print swatch.
პრობლემების აღმოფხვრა
დაფიქსირებული პრობლემა
First Rheology Check
ნუ ივარაუდებ
Paste spreads after printing
Low-shear body and recovery
Only the Brookfield viscosity is too low
Paste is difficult to push through screen
High-shear flow / shear thinning
More squeegee pressure is the only fix
Fine lines blur
Recovery, deposit, penetration
Higher viscosity always improves sharpness
Mesh marks remain visible
Leveling and timed recovery, plus screen tension, stencil and release settings
Fast recovery is always better
Stringing during screen release
Registered filament test and screen-release conditions; separate rheometer tests if elasticity is claimed
Viscosity alone explains the defect
Rotary run thins over time
Thixotropy, continuous shear, temperature
Initial lab viscosity proves long-run stability
Same viscosity, different print definition
Full shear/recovery profile
The two grades are equivalent
More thickener improves body but hand worsens
Polymer solids and paste deposit
Maximum viscosity is the target
საერთო ღირებულება გამოყენებისას
Rheology affects cost through:
სათხელებლის დოზირება
Pumping energy
Squeegee pressure
Machine speed
Screen cleaning
Rework
ქსოვილის ხელი
სასარგებლო მოდელია:
Total cost per accepted m² = all allocated batch costs (currency) ÷ accepted fabric area (m²). Calculate thickener material cost as delivered price (currency/kg of product as received) multiplied by product consumed (kg). Use one currency and the same accounting boundary for preparation, processing, downtime, post-treatment, rework and disposal.
Compare only recipes that meet the same finished-print requirements, using measured consumption and accepted output. Record machine efficiency and bottleneck capacity separately; convert a change into cost only under a stated allocation method. Avoid counting the same consumed material again as both ingredient cost and a second material-loss charge.
A cheaper product can be more expensive if it causes poor screen transfer, excessive corrections or unstable long runs.
What Information Should You Send to a Thickener Supplier?
For useful rheology matching, provide:
Current thickener name, sample or TDS
მიმდინარე დოზირება
Viscosity and complete test method
Pigment dispersion
Binder / fixer system
Final paste pH
Flat or rotary screen
Screen mesh / engraving
Squeegee settings
ქსოვილი
Machine speed
დროის გაჭიანურება
Main defect: transfer, spreading, stringing, penetration, definition or long-run drift
FSX Chemical-ს შეუძლია ამ ინფორმაციის გამოყენება მეშვეობით ნიმუშები და შესაბამისობა to compare current and candidate thickener rheology under controlled printing conditions.
Useful screen-printing paste normally needs higher structure at low shear and easier flow at high shear.
Recovery should be fast enough to limit spreading but not so fast that leveling becomes poor.
Elasticity and thixotropy can affect screen release and long-run stability even when viscosity looks normal.
Flat and rotary screen machines expose the paste to different shear histories.
The final rheology specification must be validated by actual print definition and production stability.
ხშირად დასმული კითხვები
1. What rheology is best for textile screen printing?
A useful paste normally has enough low-shear structure to control spreading, shear-thins under the squeegee and then recovers enough structure after transfer.
2. Is higher viscosity always better for print definition?
No. Excess low-shear viscosity or elasticity can reduce screen transfer, while poor recovery can cause spreading. The complete rheological profile matters.
3. What is shear thinning?
Shear thinning means apparent viscosity decreases as shear rate increases. This helps printing paste move through the screen under squeegee force.
4. What is structural recovery?
Structural recovery is the rebuilding of paste viscosity or internal structure after high shear is removed.
5. What happens if recovery is too slow?
The paste can remain too fluid after printing, causing bleeding, loss of fine detail or excessive penetration.
6. Can recovery be too fast?
Yes. Excessively rapid recovery can reduce leveling and contribute to mesh marks or uneven solid areas.
7. Why can two synthetic thickeners with the same Brookfield viscosity print differently?
They can have different shear-thinning, elasticity, yield stress, thixotropy and recovery behavior.
8. How can I measure shear thinning without a rheometer?
Use a fixed-geometry multi-speed apparent-viscosity profile with controlled dwell time, temperature and valid torque. It screens speed dependence; it does not by itself establish thixotropy, yield stress or elasticity.
9. How can I test recovery in a normal laboratory?
Measure at a defined low speed, apply a controlled shear step, then return to the same reading conditions and record timed recovery. Log transfer and switching delays and compare an unchallenged time control; do not label a delayed reading immediate.
10. Does rotary screen require lower-viscosity paste than flat screen?
Not as a universal rule. Rotary printing places more emphasis on continuous shear and long-run stability, while flat screen includes repeated strokes and dwell periods.
11. Should pigment and binder be included in rheology testing?
Yes. They can change pH, electrolyte level, solids and polymer interactions, so final rheology should be measured in the complete pigment paste.
12. What should I send FSX Chemical for rheology troubleshooting?
Send the current thickener or TDS, dosage, viscosity method, pigment, binder, pH, machine, screen, squeegee conditions and the observed transfer or print-definition problem.
Match Synthetic-Thickener Rheology to Your Screen Printing Process
If your synthetic thickener reaches the target viscosity but still gives spreading, poor transfer, stringing, excess penetration or unstable long runs, FSX Chemical can help separate low-shear viscosity from shear-thinning and recovery behavior.
For a useful technical review, send:
Your current synthetic thickener sample, TDS or COA
მიმდინარე დოზირება
Viscosity and complete test method
Pigment dispersion
Binder / fixer system
Final paste pH
Flat or rotary screen
Screen mesh / engraving
Squeegee settings
Fabric and machine speed
დროის გაჭიანურება
Current transfer, definition, penetration or stability problem
Select a synthetic thickener for the required transfer, definition and production stability under the actual process. Confirm the complete rheology profile together with deposit, fabric and the required drying and post-treatment sequence.
გაიგეთ, რატომ არ შეიძლება ტექსტილის ბეჭდვის გასასქელებლის სიმჭიდროვის მნიშვნელობების შედარება კონცენტრაციის, ტემპერატურის, ხელსაწყოს, ღერძის, სიჩქარის, მომზადების მეთოდისა და გამოცდის დროის შესაბამისობის გარეშე.
Choose CMC for textile printing by application, DS, viscosity method and formulation trials. Use a practical checklist to compare grades before bulk purchase.
Mesh size describes sodium alginate powder particle size, not final viscosity or print quality. Compare dispersion, hydration, retained matter and complete-paste performance under a defined method.
Sodium alginate purity specifications cover more than a single number. This guide explains what active content, NaCl, insoluble matter, and heavy metal data mean for textile printing paste performance — and when higher purity is worth specifying over a standard industrial grade.
Reactive dye screen printing with sodium alginate requires correct paste formulation, viscosity control, and steaming conditions. This guide covers flat and rotary screen paste requirements, alkali timing, common production defects, and how to diagnose paste-related causes.
ტექსტილის ბეჭდვისთვის განკუთვნილი გამკვრივებლები განსხვავდება ქიმიური შემადგენლობით, რეოლოგიით, საღებავებთან თავსებადობითა და გარეცხვისადმი მდგრადობით. ეს სახელმძღვანელო ადარებს გამკვრივებლების ძირითად ჯგუფებს, მათი გამოყენების საერთო მიმართულებებსა და იმ პარამეტრებს, რომლებიც მყიდველებმა წარმოებაში გამოცდის დაწყებამდე უნდა შეამოწმონ.
Improving textile print definition with CMC requires more than increasing viscosity. This step-by-step guide explains how grade selection, rheology, hydration, filtration, formulation compatibility, fabric preparation and machine settings influence edge sharpness and pattern detail.
Reliable textile printing thickener evaluation requires more than checking viscosity. This guide explains the essential raw-material, solution, paste, stability, application and finished-fabric testing parameters.
Textile printing paste problems rarely have only one cause. This troubleshooting guide explains how to diagnose viscosity drift, lumps, filtration residue, foam, separation, poor transfer, spreading, uneven color and finished-fabric defects.
High-performance textile thickeners should support both production speed and print precision. Learn how rheology, filtration, hydration, paste stability and application matching influence high-speed textile printing.
Textile printing thickening agents control much more than viscosity. This 2026 guide explains sodium alginate, CMC, CMS, compound thickeners and digital printing paste, with practical guidance on rheology, testing, application matching and supplier qualification.
Improving viscosity control in textile printing pastes requires more than adjusting a final cP or mPa·s value. Reliable control starts with standardized testing and continues through hydration, temperature, mixing, formulation sequence and printing performance.
გაგვიზიარეთ პროდუქტის დასახელება, გამოყენების სფერო, რაოდენობა, დანიშნულების ადგილი და ნებისმიერი TDS, ნიმუშის ფოტო ან დოკუმენტი, რომელიც უკვე გაქვთ. FSX Chemical შეისწავლის ინფორმაციას და გირჩევთ შემდეგ ნაბიჯს ფასის შეთავაზების, ნიმუშთან შესაბამისობის ან პროდუქტის შერჩევისთვის.
პროდუქტის ინფორმაციაპროდუქტის დასახელება, მარკა, მოდელი, ეტიკეტის ფოტო ან მომწოდებლის სარეფერენსო.
ხელმისაწვდომი დოკუმენტებიTDS, SDS, COA, ნიმუშის ფოტო, პროდუქციის სია ან სატესტო მონაცემები.
შეკვეთის დეტალებიშეფასებული რაოდენობა, შეფუთვა, დანიშნულების ქვეყანა, პორტი ან სავაჭრო პირობა.
განაცხადი ან საკითხიტექსტილის ბეჭდვის პროცესი, ფორმულირების საჭიროება, მიმდინარე პრობლემა ან სამიზნე მახასიათებელი.