Textile Printing Thickener Testing: Methods and Buyer-Defined Acceptance Criteria
Reliable textile printing thickener evaluation requires more than checking viscosity. This guide explains the essential...
The essential tests for a textile printing thickener are identity and traceability, moisture or solids, pH, method-controlled viscosity, rheology, hydration, filtration, complete-paste compatibility, print performance and batch consistency. No single viscosity result can predict screen passage, print definition, holding stability or finished-fabric quality.
A thickener that passes a clean-water viscosity test may lose structure after dyes, salts, alkalis or binders are added. Another product may produce the correct initial viscosity but create excessive filter residue, foam, poor paste transfer or difficult wash-off.
A reliable testing program should therefore move through several levels: incoming raw-material inspection, solution or stock-paste testing, complete formulation testing, printing-machine evaluation and finished-fabric assessment.
This guide lists the essential testing parameters and explains what each result can and cannot prove. Specific methods and acceptance limits should be defined for the selected thickener, printing route, equipment and fabric.
Why One Test Result Is Not Enough
Textile printing is a dynamic process. The thickener experiences water, mixing, hydration, chemical additions, pumping, filtration, screen or coating shear, contact with fabric, drying, fixation and washing.
No single laboratory number represents all of these conditions.
Viscosity does not fully describe rheology
Two products may have the same apparent viscosity at one rotational speed but flow differently during pumping or screen passage.
Raw-material testing does not prove formula compatibility
A thickener may perform well in clean water and then change after salt, alkali, dye, pigment or binder is added.
Paste testing does not replace fabric testing
A smooth and stable paste can still produce poor definition, excessive penetration, weak wash-off or an unacceptable fabric handle.
One batch does not prove commercial consistency
Sample approval should be connected with a permanent commercial grade, specification, batch documentation and first-shipment verification.
Is the correct commercial product suitable for laboratory use?
Solution or stock paste
Dispersion, hydration, viscosity, rheology, filtration, foam and physical stability
Can the product be prepared consistently?
Complete printing paste
Chemical compatibility, viscosity retention, filtration, holding stability and application behavior
Does the thickener remain suitable in the real formula?
Printed and finished fabric
Definition, penetration, shade, levelness, fixation, wash-off, handle and required fastness
Does the product meet the final manufacturing requirement?
1. Product Identity and Batch Traceability
Testing begins by confirming exactly which product has been received. Samples, production material and documents should use consistent identification.
Record the following information
Pangalan ng tagapagtustos
Commercial product and grade code
Batch or lot number
Production or retest date where applicable
Package number and package condition
Sample source
Applicable TDS, SDS and COA version
An unlabelled or temporary sample may be useful for early screening, but it should not be approved for purchasing until it is connected with a repeatable commercial grade.
2. Appearance and Physical Condition
Appearance is a basic incoming check that can reveal contamination, moisture exposure, separation or packaging damage.
For powder thickeners, inspect
Color and general uniformity
Free-flowing condition
Hard lumps or compacted areas
Visible fibres or foreign particles
Evidence of moisture exposure
Unusual odor
For liquid or pre-formulated thickeners, inspect
Separation or settling
Surface skin
Gel particles
Color variation
Gas formation or swollen packaging
Unusual odor
Appearance cannot prove application performance, but abnormal physical condition should be investigated before the material enters production.
3. Moisture, Solids or Active Content
Moisture and solids affect the effective quantity of thickening material added to the formulation.
Powder products
Moisture variation can influence flowability, storage behavior and the amount of dry polymer delivered at a fixed addition weight.
Liquid products
Solids or active content helps distinguish whether viscosity differences result from polymer performance or simply from a different supplied concentration.
Why the test method matters
Drying temperature, sample size, duration and calculation basis should be defined. Some formulations may contain volatile materials that influence a simple loss-on-drying result.
Buyers should clarify whether the reported value represents moisture, total solids, active polymer or another defined parameter.
4. pH
pH can provide useful information about product consistency and potential compatibility, but the result is meaningful only when the sample concentration and preparation method are defined.
Possible pH checkpoints
Raw liquid product
Defined powder solution
Stock paste
Completed printing paste
Paste after the normal holding period
Why pH matters
pH can influence polymer hydration, synthetic-thickener activation, binder stability, dye chemistry, preservation and holding behavior.
One acceptable pH value does not prove that the thickener is compatible with the complete printing formulation.
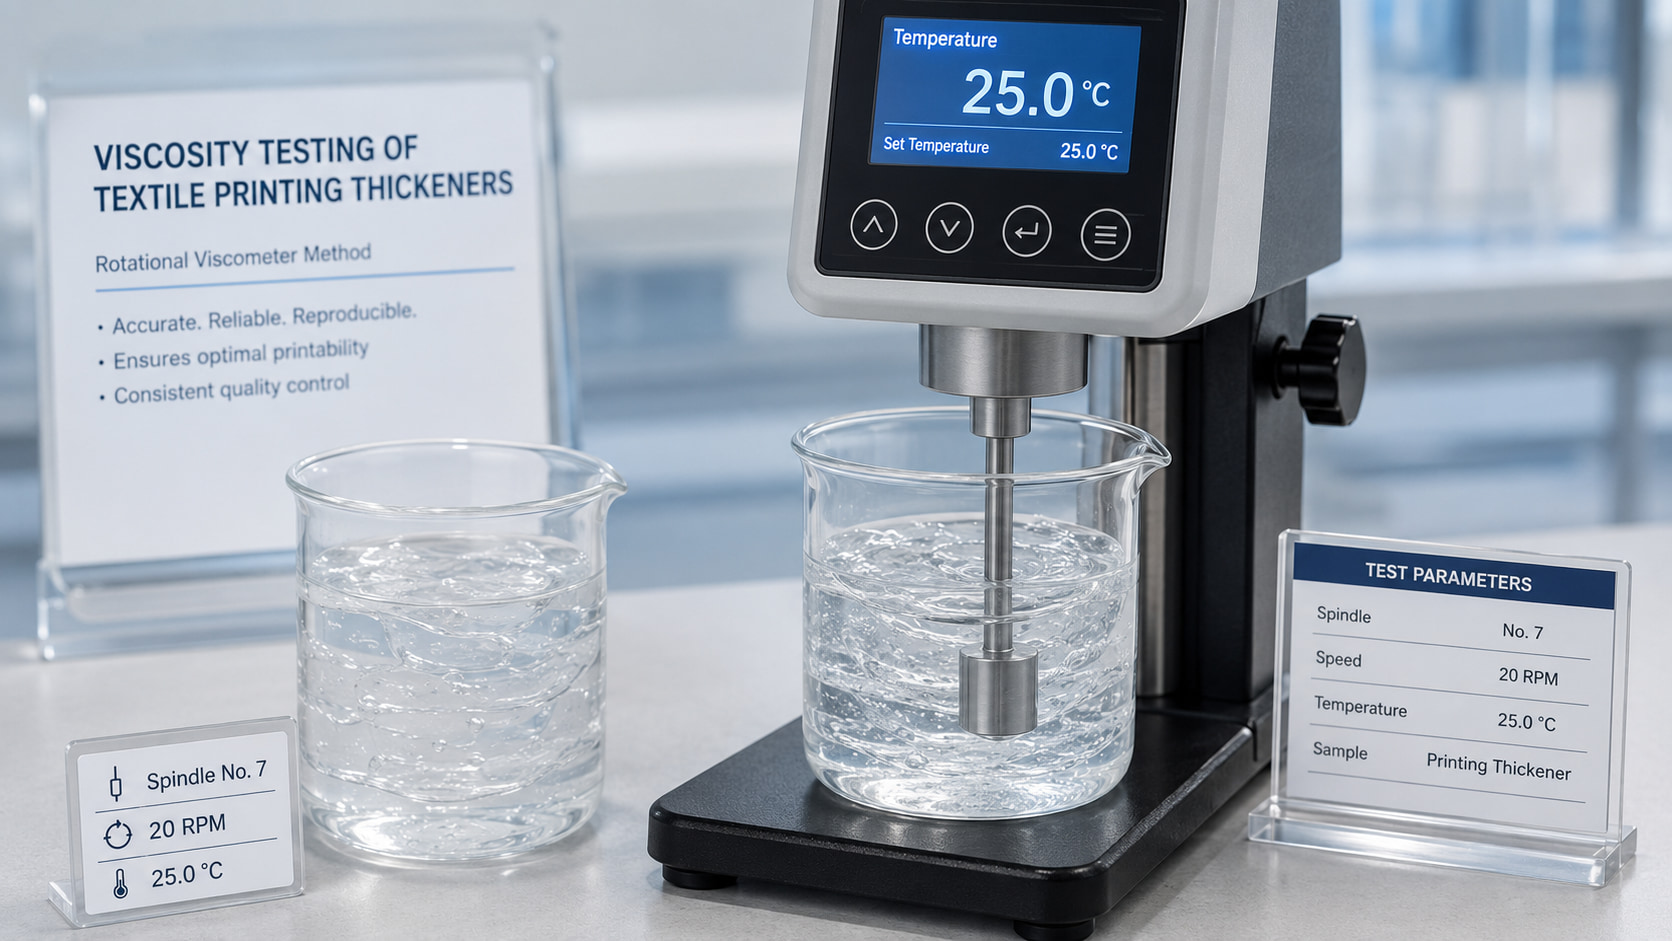
5. Viscosity
Viscosity is one of the most common thickener specifications and one of the most frequently misinterpreted.
A complete viscosity method should record
Product or paste concentration
Batayan ng pagkalkula ng konsentrasyon
Pinagmumulan ng tubig
Preparation and powder-addition procedure
Mixer type, speed and duration
Panahon ng pag-hydrate o pahinga
Temperatura ng pagsukat
Viscometer model or measurement principle
Spindle, rotor o geometriya
Bilisan ng pag-ikot
Oras ng pagbabasa
Unit
Test the same sample at the same temperature
Mixing-generated heat or seasonal laboratory variation can create an apparent difference that is unrelated to product quality.
Do not compare unlike concentrations
A viscosity result from a one-percent solution should not be compared directly with a result obtained at another concentration.
Test both stock and complete paste
The stock-paste result supports incoming control under its defined preparation method. Test the complete formulation separately after the actual chemical additions and holding period; a passing water-viscosity result cannot establish printing compatibility or finished-fabric quality.
6. Rheology and Shear Response
Rheology describes how the paste changes under different shear and time conditions. It is more informative than one viscosity value when machine behavior and print definition are important.
Multi-speed viscosity
A defined multi-speed sequence can screen for shear-thinning behavior: apparent viscosity decreases as rotational speed increases under controlled conditions. Record the sequence and dwell times. Speed-dependent thinning alone does not establish thixotropy, which requires assessment of time-dependent change and recovery.
Flow under shear
The paste should move through pumps, pipes, screens, squeegees or coating units without excessive resistance.
Structural recovery
After application, the paste should recover sufficient structure to control spreading and penetration.
Time-dependent behavior
Some pastes change during prolonged mixing, circulation or resting. Separate shear-rate effects from time-dependent recovery, continued hydration, evaporation or chemical degradation. Keep temperature and sample handling controlled and use time points representative of the actual production run.
Advanced rheological data is useful, but it should still be connected with an application trial.
7. Dispersion and Hydration
Dispersion and hydration testing evaluates how easily a thickener can be converted into a uniform solution or paste.
Record during preparation
Oras ng pagdaragdag ng pulbos
Initial wetting behavior
Pagbuo ng bukol
Required mixing time
Panahon ng pag-hydrate o pahinga
Foam development
Top-to-bottom uniformity
Incomplete hydration may cause
Pag-agos ng lapot
Gel particles
Excessive filter residue
Nonrepeatable laboratory results
Screen, filter or application-equipment blockage; evaluate digital ink nozzle behavior separately from fabric pretreatment
Reference and candidate products should be prepared using an identical procedure unless the supplier has clearly specified a different required method.
8. Particle Size and Powder Handling
Particle profile can influence dusting, flowability, wetting, hydration rate and lump formation.
Fine particles
Fine powder may hydrate rapidly but can form surface-wetted lumps when it is added too quickly or into weak liquid circulation.
Coarser particles
Coarser particles may disperse more gradually but require a longer hydration period.
Powder handling checks
Flow through the feeding system
Dust generation
Compaction during storage
Bag-to-bag uniformity
Ease of manual or automatic dosing
Particle size should not be judged as good or bad in isolation. The preferred profile depends on the factory’s mixing and dosing equipment.
9. Filtration, Insolubles and Gel Content
Filtration testing helps identify particles that may affect screens, filters, pumps, coating equipment or digital pretreatment systems.
A defined filtration method should include
Filter material
Opening or mesh size
Sample quantity
Gravity, vacuum or pressure condition
Filtration time
Residue evaluation method
Suriin ang natirang materyal.
Residue may consist of dry powder, hydrated gel, coarse polymer, precipitated chemicals, fibres or foreign contamination.
Test at more than one stage
A useful program may test the stock solution, completed paste and stored paste because residue can form after chemical addition or holding.
Filtration can remove particles, but it cannot permanently correct an incompatible formulation.
10. Chemical Compatibility
Chemical compatibility testing determines whether the thickener remains suitable after the actual printing ingredients are added.
Reactive printing checks
Evaluate the candidate with representative reactive dyes, alkali, salt, humectant and other auxiliaries.
Pigment printing checks
Evaluate compatibility with pigment dispersion, binder, crosslinker, catalyst and curing system.
Disperse printing checks
Evaluate dye distribution, paste stability, filtration and fixation behavior on polyester.
Compound thickener checks
When several polymers are combined, inspect blend viscosity, separation, gel formation and performance after storage.
Useful compatibility measurements
Viscosity before and after chemical addition
pH
Mukha
Separation or sedimentation
Pagsasala
Print performance after holding
11. Holding and Storage Stability
Printing pastes may remain in a tank for several hours before use or circulate through the machine during long production runs.
Define representative time points
Immediately after preparation
After full hydration
After completion of the formula
After the normal production holding period
After extended circulation where relevant
Check for
Pag-agos ng lapot
Pagkakahiwalay
Pag-aayos
Pagbuo ng balat
Pag-unlad ng gel
Pagpapanatili ng bula
Odor change
Filtration change
Samples should be stored in comparable closed containers to prevent evaporation from creating false viscosity differences.
12. Foam and Air Entrapment
Foam can interfere with mixing, viscosity measurement, filtration, coating uniformity and printed solid areas.
Evaluate foam during
Powder or liquid addition
High-speed mixing
Chemical addition
Pumping and circulation
Application to the fabric
Record both formation and decay
A paste may create high initial foam that disappears quickly, or lower foam that remains trapped for a long period.
Defoamer should not be added automatically before identifying whether the foam is caused by the thickener, mixer position, contaminated equipment or another auxiliary.
13. Color, Clarity and Odor
Solution color, clarity and odor can support product comparison and help detect contamination or degradation.
Kulay
A strongly colored thickener solution may influence light shades or optical evaluation, although acceptable color depends on the application.
Clarity
Clarity can help reveal insolubles or incomplete hydration, but a naturally hazy formulation is not automatically unsuitable.
Amoy
Unusual odor in a water-based liquid or stored paste may indicate contamination, degradation or unsuitable storage.
These checks should be recorded under consistent lighting, concentration and preparation conditions.
14. Microbiological Stability
Water-based liquid thickeners and prepared pastes may be vulnerable to microbiological contamination depending on their composition, storage and preservation system.
Possible warning signs
Odor change
Gas formation
Package swelling
Unexpected viscosity loss
Pagbabago ng kulay
Surface growth
Control factors
Kalidad ng tubig
Tank and line hygiene
Container closure
Storage temperature
Pagpapanatili ng oras
Approved preservation system
Microbiological limits and test methods should be selected according to the supplied product, local requirements and the factory’s risk level.
15. Paste Transfer and Machine Performance
Laboratory properties should be connected with the equipment used in actual textile manufacturing.
Check pumping, circulation, repeated shear, screen passage and consistency from the beginning to the end of the run.
Coating or padding
Check wet pickup, leveling, width uniformity, foam marks and transfer to rollers or equipment.
Digital pretreatment
A digital na pastang pang-imprenta should be tested for application uniformity, filtration, drying and compatibility with the actual ink and fabric route.
Record machine interruptions, filter changes, corrective additions and cleaning requirements during every production-relevant trial.
16. Print Definition and Penetration
Print definition is one of the most important application tests because it connects paste rheology with the visible textile result.
Use a controlled test pattern containing
Fine lines
Small text
Dots and corners
Closely spaced colors
Large solid areas
Evaluate
Talas ng gilid
Fine-line continuity
Pagkalat ng kulay
Pagkakapatag ng solidong lugar
Face-to-back penetration
Reverse-side strike-through
Definition should be inspected after the complete fixation and post-treatment process, not only while the print is wet.
17. Fixation, Wash-Off and Fabric Handle
A thickener can influence the final textile even when the initial print appears acceptable.
Fixation or curing
Evaluate the candidate using the normal steaming, thermofixation or curing conditions.
Wash-off or removal
Check whether residual thickener, unfixed dye and auxiliaries can be removed under the approved factory process.
Tela na hawakan
Compare stiffness, stickiness, surface buildup and the difference between printed and unprinted areas.
Final color and durability
Evaluate shade, color strength, levelness and the fastness or durability tests required for the product.
A candidate should not be approved when it achieves the target viscosity but creates unacceptable washing, handle or final-quality problems.
18. Batch-to-Batch Consistency
Commercial qualification requires more than one successful laboratory sample.
Compare multiple production batches for
Product identity and appearance
Moisture or solids
Viscosity under one standardized method
Hydration and filtration
Complete-paste stability
Representative printing performance
Use agreed acceptance ranges
A realistic specification should control meaningful variation without assuming that every batch will produce one identical single-point result.
Retain samples
Retained samples from approved and commercial batches support later investigation of reported differences.
Verify the first shipment
The first commercial delivery should be checked against the approved sample before routine production use.
Testing Priorities by Thickener Family
Pamilya ng pampalapot
Important Testing Priorities
Application Verification
Sodium alginate
Viscosity method, hydration, filtration, rheology, dye and alkali compatibility
Reactive print definition, fixation, wash-off and fabric handle
CMC
Viscosity, degree of substitution, purity, hydration, electrolyte response and film behavior
Selected printing, compound thickener, coating or sizing trials
FSX CMS commercial synthetic-thickener family
Grade identity, preparation or activation method, viscosity, electrolyte response, stability and filtration; confirm the supplied chemistry
Grade-specific reactive, disperse or selected special-printing trials; do not infer starch chemistry or degree of substitution from CMS
Artipisyal na pampalapot
Solids, pH activation, rheology, electrolyte tolerance and binder compatibility
Pigment printing, curing, rubbing performance and handle
Pinagsamang pampalapot
Product identity, viscosity, blend stability, filtration and batch consistency
Complete application-specific printing trial
Pasta para sa digital na pagpi-print
Solids, viscosity, filtration, storage, application pickup and ink compatibility
Definition, fixation or curing, wash-off and final handle
Use a representative sample of the current product approved in routine production.
Step 2: Confirm product identity
Record supplier, grade, batch number and applicable documents for both the reference and candidate.
Step 3: Align the preparation method
Document the comparison basis before mixing. For a direct method comparison, use the same water, concentration, containers, mixer, addition time, hydration time and measurement temperature. If a candidate requires a different supplier-specified preparation, record that difference and qualify the resulting process separately.
Step 4: Complete raw-material and stock-paste tests
Compare appearance, moisture or solids, pH, hydration, viscosity, rheology, filtration and foam.
Step 5: Prepare the complete printing formula
Use the same colorants, salts, alkalis, binders and auxiliaries in the same addition sequence.
Step 6: Test the normal holding period
Repeat viscosity, pH, appearance, separation and filtration checks.
Step 7: Conduct an application trial
Use representative fabric, screen or equipment, application quantity and production conditions.
Step 8: Complete fixation and post-treatment
Follow the normal drying, steaming, curing and washing process.
Step 9: Compare finished fabric
Evaluate definition, penetration, color, levelness, handle and required durability.
Step 10: Complete a limited production trial
Monitor the candidate throughout a representative operating period before approving a bulk conversion.
How to Define Acceptance Criteria
Acceptance criteria should separate raw-material controls from application-performance requirements.
Use method-linked specifications
For every numerical acceptance range, agree the sample basis, preparation, conditioning, measurement temperature, instrument or geometry, procedure and unit. The buyer should establish the range from the approved reference, method repeatability and production trials; this guide does not prescribe universal pass/fail limits.
Prioritize critical parameters
Parameters that directly affect machine reliability or final fabric quality may require tighter control than descriptive values.
Use ranges rather than unexplained single targets
Commercial processes usually require an acceptable operating window rather than one exact numerical value.
Define application acceptance separately
A product can meet the incoming specification and still fail the complete printing trial.
Record who approves the result
Laboratory, production, quality and purchasing teams should understand which results are required before supplier conversion.
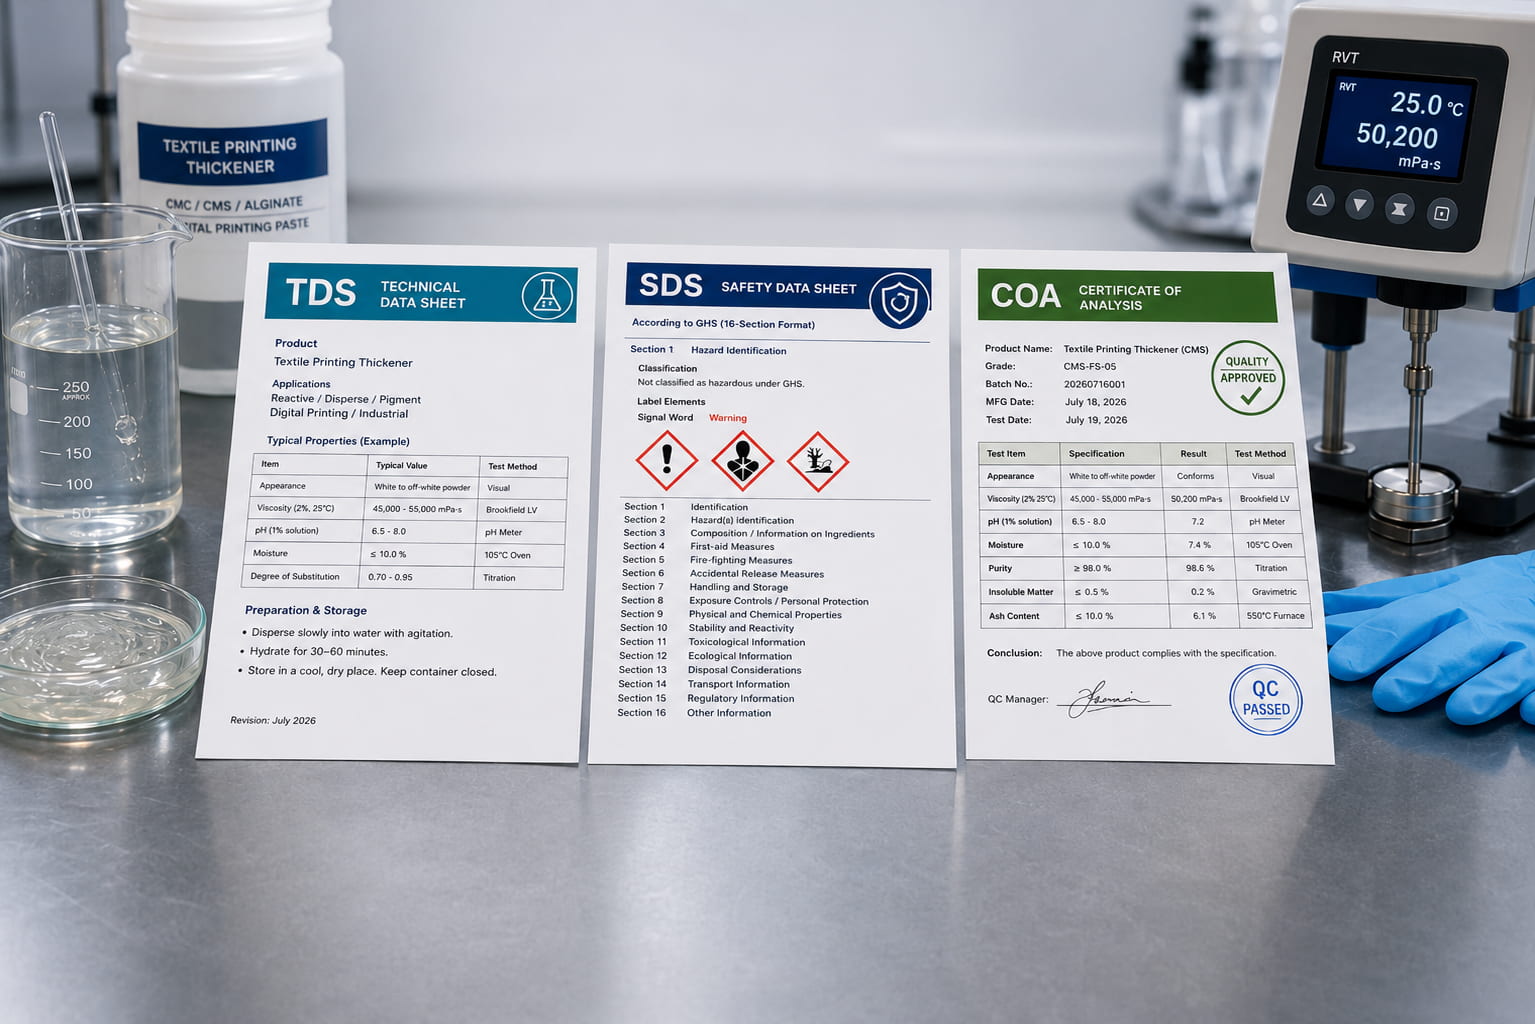
How to Review TDS and COA Data
Talaan ng Teknikal na Datos
The TDS should identify the grade, application direction, typical properties, test methods where available and preparation guidance.
Sertipiko ng Pagsusuri
The COA reports selected results for a specific production batch. Buyers should clarify which parameters will appear on routine batch documents.
Typical value versus specification
A typical value provides reference information. A specification defines the agreed commercial acceptance range.
Document consistency
Product names and grade codes should remain consistent across the sample, TDS, quotation, purchase order, label and COA.
Application data
Laboratory printing results can support grade selection, but they should not be confused with a universal performance guarantee.
Different concentrations, temperatures, spindles or speeds can create results that are not directly comparable.
Measuring before complete hydration
The apparent viscosity may continue changing after the result has been recorded.
Pagsusuri lamang sa malinis na tubig.
Real dyes, salts, alkalis, binders and other polymers may change the thickener’s performance.
Changing several variables simultaneously
Changing the thickener, dosage, auxiliaries and machine settings together prevents clear interpretation.
Ignoring temperature
Temperature variation can be mistaken for product or batch variation.
Using visual smoothness as a filtration test
A paste may look smooth while still containing particles that affect equipment or print quality.
Approving only the wet print
Definition, color, wash-off and handle may change after fixation and washing.
Skipping first-batch verification
The first commercial shipment should be checked against the approved sample and method.
Troubleshooting Unexpected Test Results
Unexpected Result
Possible Causes
Mga Inirerekomendang Pagsusuri
Supplier and buyer viscosity results differ
Different concentration, water, preparation, temperature, instrument or speed
Exchange complete methods and test one shared sample
Viscosity changes between operators
Different powder addition, mixing, resting or reading procedure
Standardize preparation and operator instructions
High filtration residue
Incomplete hydration, gel formation, chemical precipitation or contamination
Inspect residue and test stock and completed paste separately
Stock paste passes but final paste fails
Dye, salt, alkali, binder or polymer incompatibility
Add components in stages and test after each critical addition
Tama ang lapot ngunit mahina ang kahulugan
Unsuitable rheology, fabric absorbency, excessive pickup or machine settings
Review multi-speed behavior, fabric and application conditions
Stable laboratory paste changes in production
Scale, circulation, heat, evaporation, holding time or contamination
Compare laboratory and production preparation records
Bulk product differs from approved sample
Grade identity, batch variation, storage or test-method difference
Review batch codes, COA, retained samples and incoming method
Print is sharp but fabric is stiff
Excessive dosage, high pickup, poor removal or binder-film buildup
Review dosage, wash-off, curing and final surface deposition
Madalas Itanong na Mga Tanong
Which parameters should be tested first for a textile printing thickener?
Start with product identity, package condition, moisture or solids, pH and viscosity using a fully defined method. Then test hydration, filtration and the complete printing paste before printing on the target fabric.
Why can supplier and buyer viscosity results differ?
Concentration, water quality, powder-addition method, hydration time, temperature, instrument, spindle, speed and reading time can all change the result. Exchange the complete method and test a shared sample.
Is a clean-water viscosity test enough?
No. Dyes, salts, alkalis, binders and other auxiliaries can change thickener structure. Test both the stock solution and the complete formulation under the intended holding conditions.
What is an appropriate acceptance limit?
Acceptance limits should be grade-, method- and application-specific. Define them from approved-sample data, repeatability, production trials and the operating window; do not copy an unrelated supplier range.
How should a sample be compared with the first bulk batch?
Use the same preparation and measurement methods, compare retained samples and COA data, run side-by-side complete-paste and printing tests, and confirm package and batch identity.
Buyer Acceptance Record: Agree the Method Before the Limit
Create a short acceptance record for the approved reference and each candidate. It should identify what is measured, how the result is obtained and who can approve a deviation. Leave numerical limits open until your laboratory and production data support them.
Pamagat: Kontrol
Details to agree
Incoming viscosity
Grade, batch, concentration basis, water, preparation, conditioning, temperature, instrument, spindle or geometry, speed, reading time and unit.
Complete-paste stability
Formula identity, addition sequence, holding conditions, sampling times, appearance, viscosity and filtration method.
Fabric result
Fabric lot, application amount, machine settings, fixation, washing and the required definition, shade, handle and fastness assessment.
Desisyon
Buyer-approved range or reference comparison, replicate results, responsible reviewer and actions for an unexpected result.
When reference and candidate results differ, repeat the agreed method before adjusting the limit or adding corrective chemicals. A result outside the agreed range triggers investigation; it does not identify the cause by itself. Keep retained samples and the preparation record so supplier and buyer can examine the same material and method.
How FSX Chemical Supports Thickener Testing
FSX Chemical supplies sodium alginate, CMC, CMS, digital printing paste and related textile thickener routes for printing mills, formulators, distributors and importers.
Product matching begins by aligning the customer’s application, preparation method and testing parameters rather than comparing one isolated viscosity value.
Maaaring magbigay ang mga mamimili
Current thickener name, TDS and physical sample
Current viscosity and complete measurement method
Fabric and printing route
Dye, pigment, binder or ink system
Kasalukuyang dosis at pamamaraan ng paghahanda
Filtration method and residue photographs
Holding time and stability results
Printed-fabric samples or defect photographs
Tinatayang dami, pag-iimpake at destinasyon
Maaaring kabilang sa teknikal na pagsusuri
Pagkilala sa angkop na pamilya ng pampalapot
Pagsusuri ng kasalukuyang espesipikasyon ng produkto
Pag-aangkop ng lagkit at mga pamamaraan ng paghahanda
Rekomendasyon ng isang kandidatong komersyal na grado
Pagbibigay ng kaugnay na impormasyon sa TDS at SDS
A recommended sample remains a candidate for controlled evaluation. Final approval depends on the customer’s complete formulation, fabric, equipment, fixation and finished-textile requirements📧 I-email: Service@fsxchemical.com
Alamin kung bakit hindi maaaring ikumpara ang mga halaga ng viskosidad ng pampapalapot sa pagpi-print ng tela nang hindi tinutugma ang konsentrasyon, temperatura, instrumento, spindle, bilis, paraan ng paghahanda, at oras ng pagsubok.
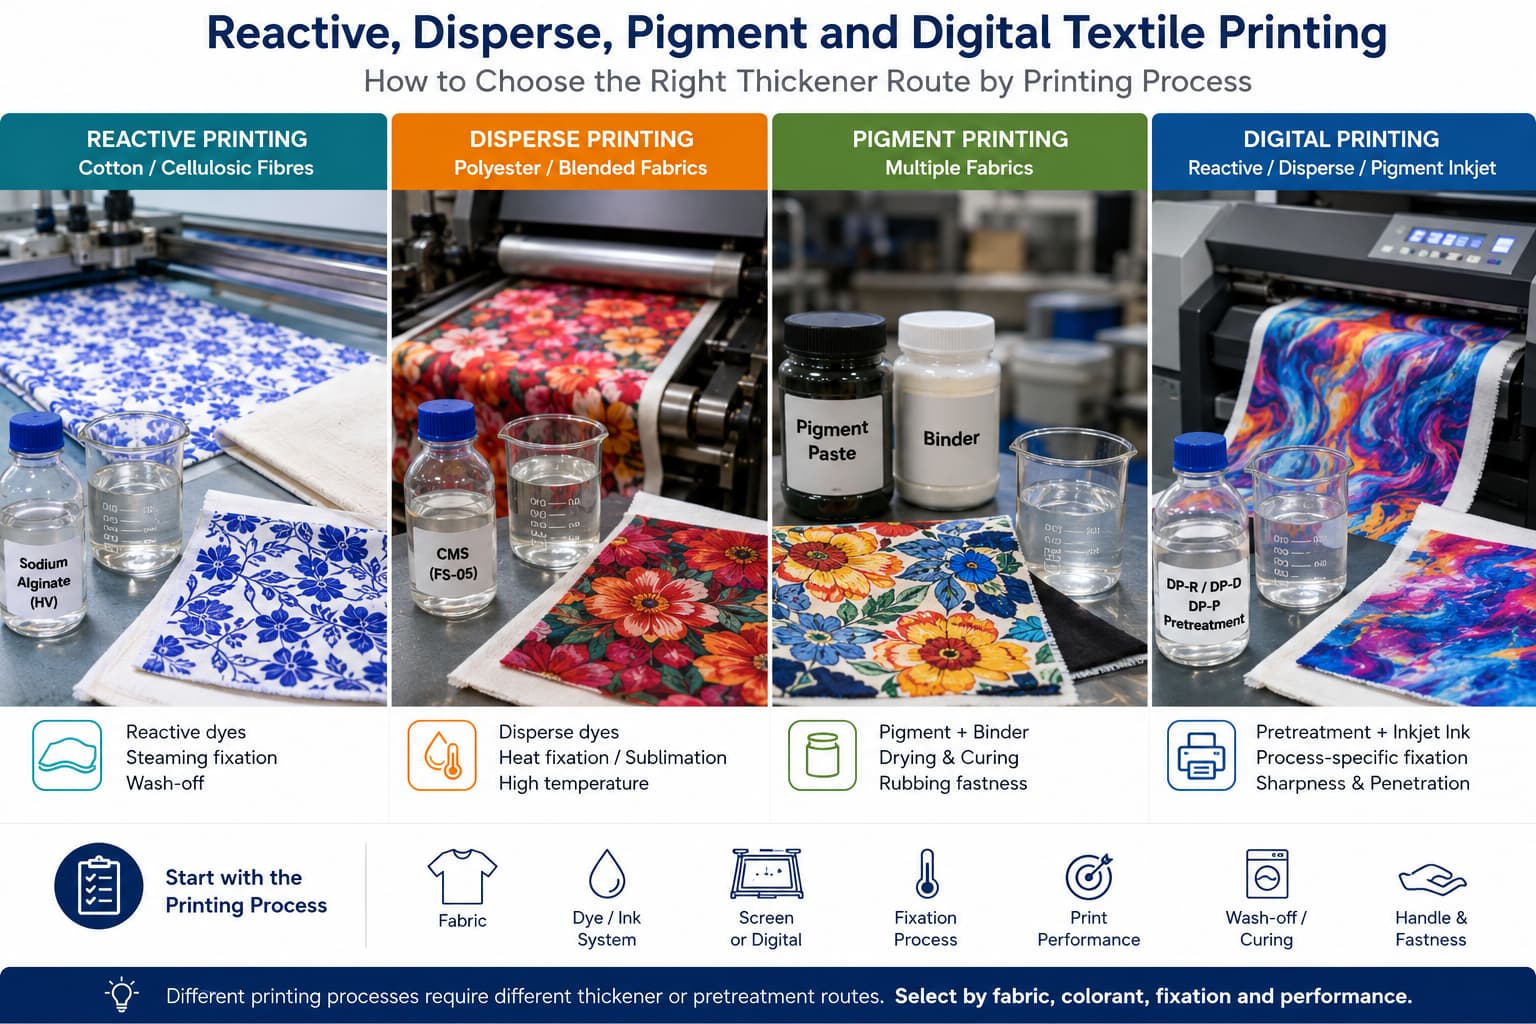
Matutong pumili ng pampatigas at mga paraan ng paunang paggamot para sa reaktibo, disperse, pigment, at digital na pagpi-print sa tela batay sa tela, tina o tinta, fiksasyon, paghuhugas, at mga kinakailangan sa kalidad ng pagpi-print.
Alamin ang pagkakaiba ng mga dokumentong TDS, SDS, at COA, kung ano ang dapat suriin ng mga mamimili ng pagpi-print ng tela, at kung paano suriin ang mga espesipikasyon, datos ng kaligtasan, mga pamamaraan sa pagsubok, mga resulta ng batch, at mga nag-isyu ng dokumento.
Alamin kung paano suriin ang isang tagagawa ng pampalapot para sa pagpi-print ng tela sa pamamagitan ng pag-verify ng pagkakakilanlan ng kumpanya, kakayahan sa produksyon, mga pamamaraan sa pagsubok, pagsubaybay sa batch, mga teknikal na dokumento, suporta sa sample, at suplay sa pag-export.
Ihambing ang CMC, CMS, sodium alginate, at digital printing paste para sa pagpi-print ng tela. Alamin kung paano nababagay ang bawat uri sa mga prosesong reaktibo, disperse, pigment, at digital, at kung ano ang dapat suriin ng mga mamimili bago magsagawa ng pagsubok ng sample, pagtutugma ng grado, at malakihang pagbili.
Malawakang ginagamit ang sodium alginate sa pagpi-print ng tela bilang matatag at maaaring hugasan na pampalapot para sa reaktibong pasta sa pagpi-print. Alamin kung paano suriin ang grado ng viskosidad, kadalisayan, at pagiging angkop sa aplikasyon bago bumili, at kung paano sinusuportahan ng FSX Chemical ang mga mamimili sa buong mundo sa pamamagitan ng teknikal na datos at mga sample.
Choose CMC for textile printing by application, DS, viscosity method and formulation trials. Use a practical checklist to compare grades before bulk purchase.
Ang pagpili ng tamang tagapagtustos ng CMC ay higit pa sa paghahambing ng presyo. Saklaw ng gabay na ito ang mga pamantayan sa pagsusuri, ang listahan ng mga dokumento, at ang proseso ng pagsubok na dapat sundin ng mga koponan sa pagbili bago mag-commit sa maramihang order.
Ang CMC-based printing paste ay ginagamit sa pigment, reactive, at digital na pagpi-print ng tela. Ipinapaliwanag ng gabay na ito kung aling mga parameter ang mahalaga, kung paano ihambing ang mga supplier, at kung ano ang dapat hilingin bago maglagay ng maramihang order.
Parehong ginagamit ang sodium alginate at CMC bilang pampalapot sa pagpi-print ng tela, ngunit angkop ang mga ito sa iba't ibang sistema ng pangkulay at kondisyon ng proseso. Ipinapaliwanag ng gabay na ito ang mga pangunahing pagkakaiba at kung kailan dapat gamitin ang bawat isa.
Direktang nakakaapekto ang bilis ng pagkakabit ng tina sa ani ng kulay, tibay ng kulay sa paghuhugas, at dami ng dumi sa tubig sa pagpi-print gamit ang reaktibong tina. Ipinapaliwanag ng gabay na ito kung paano sinusuportahan ng sodium alginate ang pagkakabit ng tina, kung aling mga parameter ng pasta ang nakakaapekto sa bilis ng pagkakabit, at kung paano ayusin ang mababang pagkakabit sa produksyon.
Mesh size describes sodium alginate powder particle size, not final viscosity or print quality. Compare dispersion, hydration, retained matter and complete-paste performance under a defined method.
Ibahagi ang pangalan ng produkto, aplikasyon, dami, destinasyon, at anumang TDS, larawan ng sample o dokumento na mayroon ka na. Susuriin ng FSX Chemical ang impormasyon at irekomenda ang susunod na hakbang para sa quotation, pagtutugma ng sample, o pagpili ng produkto.
Impormasyon ng ProduktoPangalan ng produkto, grado, modelo, larawan sa etiketa o sanggunian ng tagapagtustos.
Magagamit na mga dokumentoTDS, SDS, COA, larawan ng sample, listahan ng produkto o datos ng pagsubok.
Mga Detalye ng OrderTinatayang dami, pag-iimpake, bansang patutunguhan, pantalan o termino sa kalakalan.
Aplikasyon o IsyuProseso ng pagpi-print sa tela, pangangailangan sa pormulasyon, kasalukuyang isyu o target na pagganap.