CMS for Disperse Printing on Polyester: Paste Stability, Screen Running and Thermal Fixation
CMS can be evaluated as a thickener or compound-thickener component in selected polyester disperse printing...
A documented grade within the FSX CMS range can be considered for a controlled thickener or compound-thickener trial in selected disperse printing systems on polyester, but successful use depends on more than a high stock-paste viscosity. The CMS paste must remain stable after disperse dye and auxiliaries are added, flow through flat or rotary screens under shear, recover enough structure after transfer to maintain pattern definition, and release the disperse dye effectively during thermal fixation. This guide explains how textile mills should evaluate CMS through paste holding stability, screen running, rheology, thermal fixation, wash-off and finished print quality rather than treating one viscosity value as the final specification.
Where Does CMS Fit in Polyester Disperse Printing?
FSX CMS is used here as a commercial product-range label. Confirm the proposed grade’s current composition, preparation instructions and intended application from supplier documentation. Do not infer that every grade has the chemistry of carboxymethyl starch merely from the CMS abbreviation.
In selected polyester disperse printing systems, CMS can be evaluated as a primary thickener in a matched formula, a supporting thickener in a compound system, a rheology-adjustment component, or a cost-performance alternative when technically validated.
Academic results on a chemically identified starch derivative do not establish the composition or performance of an FSX commercial grade. Qualify the actual offered material in the complete disperse-printing formula.
Define the evaluation scope as polyester screen printing with the identified disperse dye and fixation route. Success in that process does not approve the product for sublimation-transfer paper coating or for inkjet ink.
FSX Chemical currently positions its disperse CMS route around paste stability, screen running, pattern definition and final printing performance rather than viscosity alone.
Why Paste Stability, Screen Running and Fixation Must Be Evaluated Together
A thickener can perform well in a beaker and fail on the printing machine. It can also run smoothly through the screen and still reduce color after thermal fixation.
Incorrect rheology can alter the printed paste deposit.
Deposit thickness and thickener-film structure can affect dye release during heat fixation.
Residual thickener can affect wash-off and fabric surface feel.
For this reason, CMS should not be approved from stock-paste viscosity alone.
1. What Does Paste Stability Mean?
Paste stability means the complete disperse printing paste remains sufficiently consistent throughout the realistic preparation, waiting and printing period.
A stable paste should not develop unacceptable viscosity drift, phase separation, gel particles, flocculation, settling, foam increase or skin formation.
The test must use the complete color paste, not only hydrated CMS. Typical components can include disperse dye dispersion, CMS stock paste, acid or pH-control component, dispersing agent, fixation auxiliary where used and other process-specific additives.
A stable CMS stock paste is necessary but not sufficient.
Does the paste remain stable after the actual disperse dye and auxiliaries are added?
2. Why Rheology Matters More Than One Viscosity Number
Viscosity is only one point on a larger rheological profile.
Screen printing exposes the paste to changing shear conditions: low shear while stored, moderate shear during pumping or circulation, high shear under the squeegee or rotary screen, and low shear again after deposition on the fabric.
A useful printing paste therefore needs to change flow behavior appropriately across these stages.
Many starch-derived printing thickeners show pseudoplastic or shear-thinning behavior. This means apparent viscosity decreases as shear increases.
For printing, this can be valuable because the paste can flow during screen transfer while retaining more structure when the shear is removed.
Use measured flow and recovery together with screen-transfer observations. A single low-shear viscosity match is insufficient evidence that two formulated pastes will deposit the same amount or preserve the same detail.
Same Brookfield viscosity does not mean the same screen-printing performance.
3. What Does Good Screen Running Look Like?
Good screen running means the paste remains workable and repeatable during the actual print run.
Operators should evaluate screen passage, squeegee transfer, paste pickup, pattern filling, edge definition, foam, screen drying and deposit consistency.
A CMS paste that is too structured can create poor screen passage, incomplete pattern filling, heavy or uneven transfer and repeated pressure adjustments.
A paste that is too weak can create spreading, loss of fine detail, excess penetration and uneven color boundaries.
The target is not maximum viscosity.
Stable paste body + good shear flow + sufficient recovery after transfer.
Kesme İncelmesi ve Yapısal Geri Kazanım
During the squeegee stroke, the paste experiences high shear. After it passes through the screen, the shear decreases.
The paste should recover enough structure to limit movement before drying and fixation.
Important practical questions include whether the paste becomes excessively watery during long machine runs, whether it recovers after recirculation or high-speed mixing, whether printed detail becomes softer as the run continues, and whether repeated viscosity correction is required.
These questions can reveal rheological differences that a single low-shear viscosity value cannot show.
Screen Mesh, Squeegee and Machine Conditions
The same CMS paste can behave differently on two printing machines.
Important variables include flat screen vs. rotary screen, screen mesh, engraving/open area, squeegee hardness, angle, pressure, machine speed and fabric support.
A paste that runs well through a more open screen may transfer poorly through a finer design.
Likewise, increasing squeegee pressure to compensate for poor rheology can change paste deposit, penetration, color yield and pattern definition.
This is why the buyer should send machine information when asking a CMS supplier for grade matching.
How Disperse Dye and Auxiliaries Can Change CMS Paste
Disperse dyes are supplied as fine insoluble particles stabilized by dispersing agents.
When dye dispersion and auxiliaries are added to CMS, they can change ionic strength, pH, particle-polymer interaction, viscosity, flow and foam.
The response can differ between dye colors and dye suppliers.
Therefore, a CMS grade that is stable with one disperse dye should not automatically be assumed to behave identically with every disperse dye series.
A practical qualification should include representative light, medium and high-dye-load shades where relevant so dye-load sensitivity can be observed.
Water Quality, pH and Electrolytes
Water chemistry and ionic additives can change paste behavior, depending on the documented grade and complete formulation. Establish the response by testing rather than assigning the same charge or polymer structure to every CMS-range product.
Important variables include water hardness, conductivity, pH, calcium, magnesium and electrolyte level.
Disperse printing pastes are often maintained under weakly acidic or otherwise dye-appropriate conditions depending on the specific dye and fixation route.
The correct pH should be defined by the actual disperse dye system rather than copied from a generic CMS specification.
If laboratory trials use deionized water but production uses hard plant water, repeat the complete paste test with plant water before approving the grade.
Paste Age and Holding Time
Printing paste can change while it waits in the color kitchen or machine tank.
A useful CMS holding test records initial viscosity, viscosity after the expected waiting period, viscosity near the end of the planned working period, appearance, foam, separation and gel particles.
Do not use one universal holding time. Build the test around the factory’s real workflow.
A paste that looks stable for a short laboratory period may not remain stable over a full production shift.
Likewise, a paste that drifts slightly may still be acceptable if the change remains inside a validated process window.
4. Why Thermal Fixation Changes the Thickener Requirement
Disperse printing on polyester is not finished when the paste dries. The disperse dye must move from the printed deposit into the polyester during the approved thermal fixation process.
Depending on dye type and equipment, fixation may involve high-temperature steaming, dry-heat thermofixation or another supplier-approved thermal route.
The exact temperature and time depend on the dye, polyester and machine.
This means the CMS thickener must do two apparently different jobs:
Hold the dye in the required pattern before fixation.
Release the dye effectively enough during fixation for transfer into polyester.
A thickener that controls printing perfectly but traps too much dye in its film can reduce useful color development.
Thickener Film and Disperse Dye Release
During drying, the thickener forms a solid or semi-solid layer containing disperse dye particles.
During thermal fixation, dye must leave this printed layer and diffuse into polyester.
A difference in final color can have several causes, including deposited dye quantity, fixation conditions, substrate variation and removal of surface material during finishing. Test these alternatives before attributing a weak print specifically to dye retention by the thickener film.
The practical lesson is not that CMS is always better.
Thickener-film behavior during fixation matters independently from wet-paste viscosity.
Therefore, compare final K/S or color strength only after using the same dye loading, drying, fixation and washing/clearing conditions.
When comparing formulations, record actual wet paste deposit and dry add-on as well as nominal dye concentration. Equal dye concentration in the mixing vessel does not guarantee equal dye delivered to the fabric.
CMS Thermal Stability and Surface Residue
The thickener system should remain suitable under the selected thermal process.
Possible problems include yellowing, surface darkening, sticky residue, difficult wash-off and harsh surface feel.
Thermal stability can be checked on white fabric treated with CMS paste but no dye, printed fabric after fixation, and fabric after the complete wash/clearing route.
This helps separate thickener discoloration from dye-related shade changes.
Washing or Reduction Clearing After Fixation
After disperse dye fixation, some processes use washing, soaping or reduction clearing to remove surface dye, unfixed particles, thickener residue and other auxiliaries.
The exact route depends on the disperse dye class, fixation process and required fastness.
CMS should therefore be evaluated for wash-off, surface cleanliness, rubbing fastness and fabric hand.
A paste that delivers high wet-print viscosity but leaves excessive residue after processing may have a higher Total Cost in Use.
Polyester Construction and Fabric Variables
Polyester fabrics differ substantially in structure and surface.
Important variables include woven vs. knitted construction, fabric weight, filament type, microfiber content, surface texture, brushing or raising, stretch content and finishing oils or silicone.
The same CMS paste can show different penetration and color development on different constructions.
For example, a lightweight open polyester may require different paste body and screen settings from a dense woven fabric.
Validate the grade on the actual production substrate.
CMS vs. Other Thickener Routes
Polyester disperse printing can use several thickener families depending on formulation and equipment.
Possible routes include CMS, sodium alginate, tamarind-derived thickeners, guar derivatives, synthetic thickeners and compound-thickener systems.
No family is universally best.
Compare required concentration, paste stability, shear response, screen running, color yield, fixation behavior, wash-off, fabric hand and cost.
A lower raw-material price does not automatically create the lowest-cost printing route.
When a Compound-Thickener Route Makes Sense
CMS can also be used as one component of a blended thickener.
Evaluate a blend against its component reference routes using a documented total dose. A changed blend can affect preparation and deposition, so any benefit requires complete-paste and finished-print evidence.
A compound system may be useful when the formulator wants to balance paste body, shear flow, dye release, cost and wash-off.
However, blending should solve a defined performance gap.
Do not add a second thickener only because the first one has a different viscosity number.
Evaluate the complete blend at the intended total dosage.
Separate Paste Deposit from Fixation and Wash-Off Effects
Compare the candidate with the approved reference using one fabric lot and a defined disperse-dye recipe. This suggested workflow distinguishes material selection from process effects; it is not a report of an FSX grade’s tested performance.
Sahne
Record
What the comparison can reveal
Preparation and holding
Grade, lot, concentration basis, water, hydration, pH, viscosity method and paste age
Whether the complete paste stays printable over the intended period
Screen transfer
Screen, settings, fabric area and actual paste deposit by a defined method
Whether a shade difference starts with unequal applied dye
Drying and fixation
Actual route, loading, exposure time and verified equipment conditions
Whether the print enters comparable thermal processing
Tedavi sonrası
Identical supported washing or clearing route and finished evaluation
Whether surface material or residue changes the final result
Use Blanks and Paired Stages
Process unprinted fabric and an appropriate dye-free treatment control alongside the printed specimens when investigating discoloration or harsh residue. A dye-free paste control can help locate a thickener/auxiliary contribution, but removing the dye dispersion also removes its associated formulation ingredients; note that limitation.
Retain matched specimens after fixation and after the complete post-treatment. Measure color with the same instrument setup, backing and specimen conditioning. K/S is an optical comparison, not a direct dye-fixation percentage. Do not declare improved fixation solely because one specimen looks darker before surface dye has been removed.
Confirm a Usable Finished-Print Window
Assess detail, uniformity, required fastness, residue and hand together. If a different thickener dose or screen setting is needed, identify it as a revised process rather than a 1:1 replacement. Repeat the selected route on representative production and retain its grade, formula and process scope for later batch comparison.
Production Trial and Approval Criteria
A successful laboratory print is not enough for final approval.
Production should verify large-batch hydration consistency, paste holding time, pump/circulation stability, screen running over a realistic machine length, left-center-right print uniformity, fixation consistency and wash/clearing performance.
Retain the CMS batch number, color-paste batch, fabric lot, screen settings, fixation record and finished reference fabric.
The most useful approval criterion is a stable operating window, not one perfect laboratory sample.
The laboratory result proves production suitability
Toplam Kullanım Maliyeti
CMS should not be selected from powder price alone.
A useful commercial comparison includes CMS price, required dosage, preparation time, screen-running efficiency, dye utilization, fixation energy, washing/clearing, rework and rejected fabric.
Total cost per accepted metre = attributable material, preparation, processing and quality-loss costs divided by accepted metres
A more expensive CMS grade can be commercially better if it uses a lower dosage and reduces screen interruptions. A cheaper grade can be better if it delivers stable printing and equivalent finished performance.
The answer must come from the production trial.
What Information Should You Send to a CMS Supplier?
For useful polyester disperse-printing grade matching, send:
Polyester fabric type and construction
Flat or rotary screen
Screen mesh/engraving information where available
Current thickener product or TDS
Mevcut kıvam arttırıcı dozu
Target viscosity and complete test method
Disperse dye brand/type
Representative dye loading
Complete or simplified printing formula
Plant-water information where relevant
Yapıştırma bekleme süresi
Kurutma koşulları
Thermal fixation method
Washing/reduction-clearing route where used
Current screen-running, color, residue or cost problem
FSX Chemical bu bilgileri şu yollarla kullanabilir: Numune ve Ürün Eşleştirme to review the current documentation for a candidate grade and determine the scope of a controlled trial. A model code alone is not production approval.
How Should CMS Be Qualified for Polyester Disperse Printing?
CMS Hydration → Complete Paste Stability → Screen Rheology → Print Transfer → Drying → Thermal Fixation → Dye Release → Wash/Clearing → Finished Fabric → Total Cost in Use
CMS is a product family, not one universal disperse thickener.
Paste holding stability must be tested after dye and auxiliaries are added.
Screen running depends on shear behavior, not only low-shear viscosity.
The thickener must hold the dye before fixation and release it effectively during thermal fixation.
Final color, fastness, residue and hand should be judged after the complete post-treatment.
Approve CMS through the actual polyester, dye, screen and fixation route.
Sık Sorulan Sorular
1. Can CMS be used for disperse printing on polyester?
Yes, CMS can be evaluated as a thickener or compound-thickener component in selected polyester disperse printing systems. Final suitability should be confirmed with the actual dye, screen and fixation route.
2. Is higher CMS viscosity always better for screen printing?
No. Screen printing requires suitable shear thinning, transfer and structural recovery. A very high low-shear viscosity can still give poor screen running.
3. Why does CMS viscosity change after disperse dye is added?
Dye dispersions and auxiliaries can change pH, ionic strength and polymer-particle interactions, which can alter apparent viscosity.
4. What does good screen running mean?
It means the paste transfers consistently through the screen without excessive pressure, clogging, foaming, pattern loss or major viscosity drift.
5. Can CMS be used on both flat and rotary screens?
Selected CMS systems can be used on either route, but the required rheology can differ with mesh, squeegee, speed and machine design. Validate the actual equipment.
6. Why can a paste print well but develop low color after fixation?
Possible causes include insufficient thermal fixation, unsuitable dye class, poor dye release from the thickener film or excessive penetration. Wet-print quality alone does not predict final K/S.
7. Does CMS affect disperse dye release during thermofixation?
The thickener film can influence dye release during thermal processing. CMS formulation and film behavior should therefore be evaluated after fixation, not only from wet-paste viscosity.
8. Does CMS need to be washed off after disperse printing?
The required washing, soaping or reduction-clearing route depends on the dye, fixation method and end-use requirement. Evaluate residue and fastness after the actual production post-treatment.
9. Can CMS be blended with sodium alginate or another thickener?
Yes, compound systems can be evaluated when there is a defined rheology, dye-release or cost target. The blend should be tested at the intended total dosage.
10. Why does the same CMS run differently on two factories’ machines?
Water quality, hydration, screen mesh, squeegee settings, machine speed, dye formula and holding time can all change screen behavior.
11. What should be compared besides CMS viscosity?
Compare hydration, paste stability, shear behavior, screen running, color strength after fixation, wash-off, residue, hand and Total Cost in Use.
12. What should I send FSX Chemical for disperse CMS matching?
Send the current thickener TDS or sample, viscosity method, polyester construction, disperse dye, printing formula, screen route, fixation and washing conditions plus the current production problem.
Evaluate CMS for Polyester Disperse Printing with FSX Chemical
If your current disperse printing paste shows viscosity drift, poor screen running, low color after fixation or difficult wash-off, FSX Chemical can help identify whether the next trial should focus on CMS grade, dosage, compound-thickener design or process conditions.
For a useful technical comparison, send your current thickener sample/TDS, polyester fabric construction, flat or rotary screen information, current dosage, viscosity method, disperse dye, formula, plant water where relevant, paste holding time, drying, thermal fixation, washing/clearing and the current screen, color, residue, hand or cost target.
For polyester disperse printing, a good CMS thickener must remain stable in the color paste, run predictably through the screen, and then get out of the dye’s way during thermal fixation. The final print—not the stock-paste viscosity—is the acceptance standard.
Konsantrasyon, sıcaklık, ölçüm cihazı, mil, hız, hazırlık yöntemi ve test süresi gibi faktörler eşleştirilmeden tekstil baskı kıvamlaştırıcılarının viskozite değerlerinin neden karşılaştırılamayacağını öğrenin.
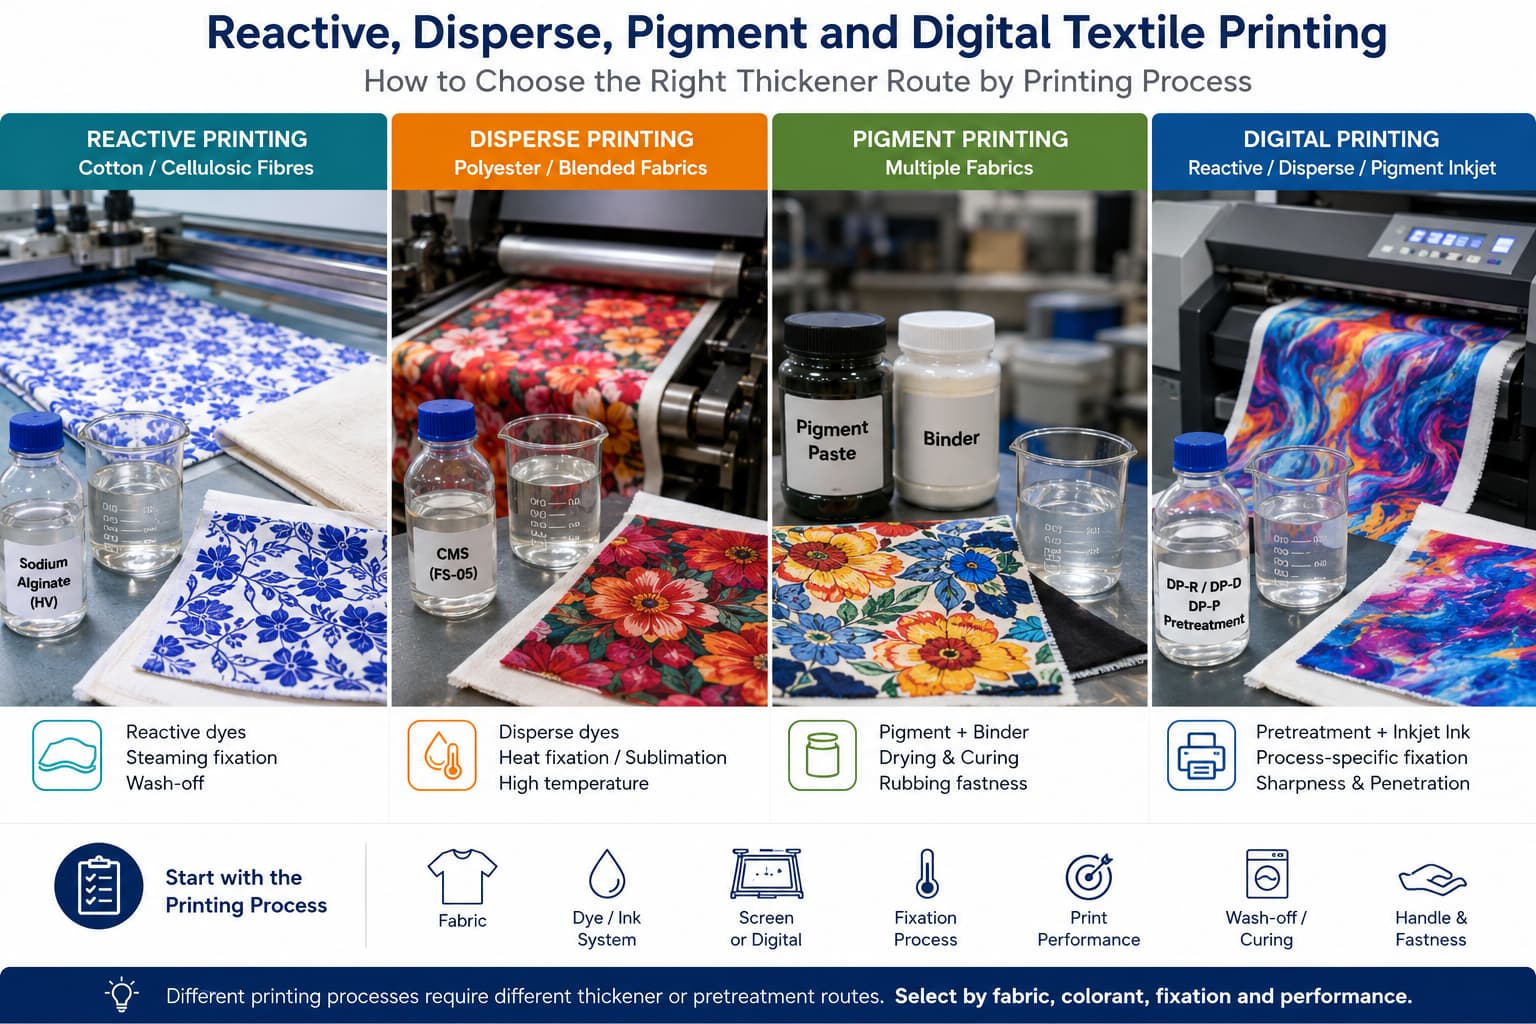
Kumaş, boya veya mürekkep, fiksaj, yıkamayla uzaklaştırılabilirlik ve baskı kalitesi gereksinimlerine göre reaktif, dispers, pigment ve dijital tekstil baskısı için kıvamlaştırıcı ve ön işlem seçeneklerini nasıl seçeceğinizi öğrenin.
Tekstil baskısı için CMC, CMS, sodyum aljinat ve dijital baskı patını karşılaştırın. Her ürün seçeneğinin reaktif, dispers, pigment ve dijital baskı süreçlerine nasıl uygun olduğunu ve alıcıların numune testi, ürün sınıfı eşleştirme ve toplu satın alma öncesinde neleri incelemesi gerektiğini öğrenin.
Karboksimetil selüloz (CMC), tekstillerin baskı, haşıllama ve boyama işlemlerinde yaygın kullanılır. Bu kılavuz; CMC sınıflarının nasıl değerlendirileceğini, hangi parametrelerin en önemli olduğunu ve FSX Chemical’ın satın alma kararlarını nasıl destekleyebileceğini açıklar.
Sodyum aljinatın parçacık boyutu (mesh), tozun ne kadar hızlı çözündüğünü, ne kadar homojen bir şekilde su emdiğini ve elde edilen macunun serigrafi baskısında nasıl bir performans gösterdiğini etkiler. Bu kılavuz, tekstil baskı macunu uygulamalarında mesh değerinin pratik sonuçlarını açıklamaktadır.
Sodyum aljinat saflık spesifikasyonları, tek bir rakamdan ibaret değildir. Bu kılavuzda, aktif madde, NaCl, çözünmeyen madde ve ağır metal verilerinin tekstil baskı macununun performansı açısından ne anlama geldiği ve standart endüstriyel sınıfa kıyasla daha yüksek saflığın ne zaman tercih edilmesi gerektiği açıklanmaktadır.
Sodyum aljinat kullanılarak yapılan reaktif boya serigrafi baskısı, doğru pasta formülasyonu, viskozite kontrolü ve buharlandırma koşullarını gerektirir. Bu kılavuz, düz ve döner serigrafi pastaları için gereklilikleri, alkali zamanlamasını, sık görülen üretim kusurlarını ve pastayla ilgili sorunların nasıl teşhis edileceğini ele almaktadır.
Sodyum aljinat, pamuk üzerine reaktif boya baskısı için standart kıvam arttırıcıdır; ancak polyester üzerine dispers boya baskısı için uygun değildir. Bu kılavuzda, bunun nedeni, boya kimyasında hangi farklılıkların söz konusu olduğu ve polyester ile polyester karışımlı kumaşlara baskı için hangi kıvam arttırıcı türlerinin uygun olduğu açıklanmaktadır.
Tekstil baskı pastası için kullanılan CMS, viskozitenin ayarlanmasına yardımcı olabilir, pastanın işlenebilirliğini artırabilir ve formülasyonun istikrarlı performansını destekleyebilir. Bu kılavuz, alıcıların toplu satın almadan önce CMS türlerini viskozite, DS, çözünürlük, pH, nem ve numune testleri açısından nasıl değerlendirebileceklerini açıklamaktadır.
Selüloz bazlı hammaddeler, tekstil baskısı, baskı macunu hazırlığı, kıvam artırma ve formülasyon desteği alanlarında kullanılmaktadır. Bu kılavuz, alıcıların CMC, CMS, sodyum aljinat, tekstil baskı kıvam arttırıcıları ve baskı macunu ürünlerini teknik özellikler, belgeler, numune testleri ve tedarikçi desteği açısından nasıl değerlendirebileceklerini açıklamaktadır.
Selüloz türevleri, tekstil baskısı, baskı macunu hazırlığı, kıvam artırma ve formülasyon desteği alanlarında yaygın olarak kullanılmaktadır. Bu kılavuz, yurtdışı alıcıların FSX Chemical’dan CMC, CMS, sodyum aljinat, tekstil baskı kıvam artırıcıları ve baskı macunu ürünlerini, TDS, COA, numune testi, kalite eşleştirme ve ihracat belgeleri desteği ile nasıl temin edebileceklerini açıklamaktadır.
Tekstil endüstrisi kimyasallarını seçmek, sadece ürün isimlerini karşılaştırmaktan ibaret değildir. Bu kılavuz, tekstil baskı alıcılarının CMC, CMS, sodyum aljinat, tekstil baskı kıvamlandırıcıları ve baskı macunu ürünlerini uygulama alanı, teknik özellikler, TDS, COA, numune testi ve parti tutarlılığı açısından nasıl eşleştirebileceklerini açıklamaktadır.
Ürün adını, uygulama alanını, miktarı, teslimat yerini ve elinizdeki TDS, numune fotoğrafı veya belgeleri paylaşın. FSX Chemical bu bilgileri inceleyerek fiyat teklifi, numune karşılaştırması veya ürün seçimi için bir sonraki adımı önerecektir.
Ürün BilgileriÜrün adı, sınıfı, modeli, etiket fotoğrafı veya tedarikçi referansı.
Mevcut BelgelerTDS, SDS, COA, numune fotoğrafı, ürün listesi veya test verileri.
Sipariş DetaylarıTahmini miktar, ambalaj, varış ülkesi, liman veya teslim şekli.
Uygulama veya SorunTekstil baskı süreci, formülasyon gereksinimi, mevcut sorun veya hedeflenen performans.