Acrylic Thickener for Dark Pigment Shades: Why High Pigment Loading Changes Viscosity and Color Yield
High pigment loading changes more than pigment concentration. It also changes water, dispersant, surfactant, electrolyte...
Dark pigment shades are a useful stress test for acrylic thickener because increasing pigment-dispersion dosage changes more than color concentration. It can also change water, dispersant, surfactant, electrolyte and pigment solids entering the paste. Depending on the complete formulation, viscosity may decrease, increase or drift during holding. Build a pigment-loading–rheology map and verify screen transfer, color, cure, rubbing and hand. Select a dosage inside a demonstrated operating window, with suitable allowance for the intended production variation, rather than treating the lowest passing laboratory point as a universal minimum.
Why Does High Pigment Loading Change Acrylic Thickener Performance?
High pigment loading changes the chemical and physical environment of the acrylic thickener.
When more commercial pigment dispersion is added, the paste can receive more:
Pigment solids
Вода
Диспергатор
Поверхнево-активна речовина
Електроліти
pH-control chemicals
Each of these variables can change viscosity or rheology.
The final response can therefore be:
Lower viscosity
Higher viscosity
Similar initial viscosity but poorer holding stability
Similar Brookfield viscosity but different screen rheology
The correct diagnostic chain is:
Pigment Loading → Complete-Paste Rheology → Screen Transfer → Penetration → Surface Color Yield → Curing / Fastness / Hand
Do not assume that every dark shade simply needs more thickener.
Why Dark Shades Are a Useful Stress Test
Dark shades often use a higher dose of pigment dispersion than pale shades.
This makes them a practical stress test for:
Толерантність до електролітів
Surfactant sensitivity
Сумісність з палітурками
Thickener efficiency
Screen-transfer uniformity
Dark solid areas also make certain defects easier to see:
Нерівномірний перенос
Недостатнє висвітлення
Надмірне проникнення
Нерівномірність поверхні
Розповсюдження по краях
A thickener that works in a pale shade should therefore not be approved automatically for a high-pigment black or navy formula.
Pigment Dispersion Is More Than Pigment
A commercial pigment dispersion is a formulated liquid, not pure dry pigment.
It can contain:
Pigment particles
Вода
Anionic or nonionic dispersants
Wetting agents
Поверхнево-активні речовини
Preservatives
pH-adjusting chemicals
Електроліти
Отже:
More Pigment Dispersion ≠ Only More Colorant.
Two black pigment dispersions with the same pigment content can still influence acrylic thickener differently because their dispersant, surfactant and salt packages differ.
For this reason, supplier changes in pigment dispersion should trigger a viscosity and compatibility recheck.
High Pigment Loading Can Lower or Raise Viscosity
The direction of viscosity change is system-specific.
Viscosity can decrease because:
Extra dispersion added on top of a batch can dilute the thickener; a fixed-final-mass recipe that replaces make-up water need not do so.
Electrolytes screen charged polyacrylate groups.
Surfactants disrupt associative thickening.
pH moves outside the ideal activation window.
Viscosity can increase because:
Pigment solids increase the suspended-particle volume fraction.
Particle crowding increases flow resistance.
Surfactants strengthen an associative HASE network in a certain concentration range.
Pigment or binder particles participate in associative thickening.
This is why the article title says high pigment loading changes viscosity rather than always lowers it.
Measure the response of the real formula.
1. Dilution from Pigment Dispersion
Whether more pigment dispersion dilutes the thickener depends on the batch mass balance. Adding it on top of an existing paste increases final mass and can lower the thickener mass fraction. In a formula made to a fixed final mass, increasing dispersion while reducing make-up water leaves the thickener mass fraction unchanged if its dose is unchanged. Carrier composition, ions and particle loading can still alter rheology.
Record each ingredient in grams per kilogram of final paste, including make-up water. Distinguish a production shade formula from an extra-addition troubleshooting experiment. A viscosity loss in a correctly mass-balanced dark shade cannot be attributed to thickener dilution without checking the actual concentration.
2. Dispersants and Surfactants
Pigment dispersants and surfactants keep pigment particles separated and wettable.
But these surface-active chemicals can change acrylic-thickener rheology.
For a conventional ASE-type thickener, they can modify the aqueous and particle environment.
For a HASE-type associative thickener, surfactants can participate directly in hydrophobic associations.
Depending on concentration, this can:
Increase viscosity
Decrease viscosity
Change elasticity
Change recovery after shear
Therefore, a high-pigment formula can move the thickener into a different surfactant-response region.
3. Electrolyte Load
Many acrylic/polyacrylate thickeners contain ionized carboxylate groups after neutralization.
Electrolytes can screen those charged groups and reduce polymer expansion.
A simplified mechanism is:
Electrolyte Load ↑ → Charge Screening ↑ → Polymer Expansion Can Decrease → Thickening Efficiency Can Fall
Dark shades can create more ionic stress if the higher pigment dose also introduces more salts or ionic dispersants.
But the effect remains grade-specific.
Hydrophobically modified systems can respond differently because associative interactions provide another rheological mechanism.
Do not assume one electrolyte-retention result applies to every acrylic thickener.
4. Pigment Solids and Particle Crowding
At higher pigment solids, the particles themselves occupy more volume inside the paste.
As particle concentration increases, interactions between particles can increase flow resistance.
This can partially offset dilution or electrolyte-related viscosity loss.
In some systems, the result can be:
More Pigment → Higher Apparent Viscosity
rather than thinning.
The particle effect depends on:
Pigment concentration
Particle size distribution
Якість дисперсії
Binder particles
Thickener architecture
This is another reason not to diagnose dark-shade viscosity from pigment percentage alone.
5. HASE and Associative-Thickener Interaction
HASE acrylic thickeners use both pH-driven swelling and hydrophobic association.
The hydrophobic groups can associate with:
Other HASE chains
Binder particles
Surfactant aggregates
Pigment-dispersion components
High pigment loading can therefore change the associative network in both directions.
Research on associative thickeners shows that pigment, dispersant, surfactant and latex concentration can all alter rheological behavior.
The practical implication is:
HASE Dark-Shade Performance Must Be Tested with the Real Pigment and Binder System.
6. Binder-to-Pigment Ratio
Compare pigment and binder on a stated mass basis. The dose of a commercial dispersion is not the mass of pigment; the dose of a binder emulsion is not necessarily the mass of functional film-forming polymer. Use composition information for the exact supplied grade when available.
Trial record
Calculation or evidence
Interpretation limit
As-supplied dispersion and binder dose
Record each in g/kg of final paste, with the complete water balance.
Equal liquid dosage does not establish equal pigment or binder content.
Pigment mass
Dispersion dose × supplier-confirmed pigment mass fraction.
Do not substitute total dispersion nonvolatile content for pigment fraction.
Functional binder mass
Binder dose × disclosed film-forming binder mass fraction, when confirmed.
Dry residue may include non-binder ingredients; label functional content as unknown if it is not disclosed.
Complete-paste nonvolatile residue
Measure with the agreed drying procedure and record its conditions.
This includes retained pigment and other nonvolatile components, not only active binder.
Printed deposit and acceptance
Record deposited paste or dry add-on, cure conditions, shade, rubbing and hand.
A recipe ratio alone does not predict the cured fabric result.
Hypothetical arithmetic, not an FSX test: 50 g/kg of a dispersion containing a confirmed 40% pigment contributes 20 g/kg pigment. A 100 g/kg binder dose with a separately confirmed 30% functional binder fraction contributes 30 g/kg binder. Their functional binder-to-pigment mass ratio is 1.5. If only total nonvolatile content is known, that functional ratio cannot be calculated. This example defines the basis; it is not a recommended ratio.
Increasing binder can also alter surfactants, ions, water balance and paste rheology. Evaluate the binder and pigment ladder together with the validated curing schedule. Cotton Incorporated describes the binder–fastness–hand trade-off; it does not prescribe a universal ratio for your pigment package.
7. pH and Neutralization
Pigment dispersions can change final paste pH.
If the acrylic thickener is pH-responsive, a dark-shade formula can move away from the grade’s most useful activation range.
Запис:
pH after thickener activation
pH after pigment addition
pH after binder addition
Кінцевий рН пасти
Holding-time pH
Do not increase thickener dosage before confirming the dark-shade paste remains inside the validated pH window.
High pigment loading can make an already electrolyte-sensitive system more vulnerable to variable process water.
Calcium, magnesium and dissolved salts can add to the ionic load from:
Пігментна дисперсія
Папка
Ремонтник
If dark shades are unstable but light shades are acceptable, test the formula in:
Reference low-hardness water
Normal plant water
Representative high-hardness condition if relevant
Do not assume the pigment is the only variable.
Should Dark Shades Use More Acrylic Thickener?
Not automatically.
A dark shade can require more thickener if the higher pigment loading lowers complete-paste viscosity below the approved printing window.
But more thickener may be unnecessary or harmful if:
Particle crowding has already raised viscosity.
The paste still prints cleanly at the lower Brookfield number.
The real problem is pH or electrolyte compatibility.
Higher thickener dosage worsens hand or screen transfer.
Use this sequence:
Measure Complete-Paste Rheology → Print → Then Decide Thickener Dosage
не:
Dark Shade → Automatically Add More Thickener.
How High Pigment Loading Changes Color Yield
More pigment can increase apparent color strength, but the relationship is not unlimited.
Color yield depends on:
Pigment amount
Surface pigment concentration
Відкладення пасти
Проникнення
Плівка для пакування
Dispersion uniformity
Отвердіння
If a higher pigment dose causes the paste to become too fluid, deeper penetration can reduce the pigment concentration visible at the surface.
If the paste becomes too thick, incomplete transfer can reduce actual deposited pigment.
Отже:
More Pigment ≠ Automatically Higher Surface K/S.
Penetration vs. Surface Color
For many pigment prints, the target is enough penetration for uniform coverage without losing too much pigment below the visible surface.
Low viscosity can increase:
Fabric penetration
Reverse-side show-through
Розповсюдження по краях
High viscosity can reduce:
Перенесення зображення на екран
Вирівнювання
Coverage of textured fabrics
The preferred penetration depends on:
Структура тканини
Fabric weight
Design
Pigment shade
Binder system
Evaluate the printed fabric—not viscosity alone.
Screen Transfer and Solid-Area Uniformity
Dark shades frequently include large solid areas where transfer uniformity is easy to judge.
High pigment loading can change:
High-shear viscosity
Вихід фільму на екрани
Squeegee pressure demand
Відкладення пасти
Check:
Beginning-to-end solid-area density
Screen filling
Мікроотвори
Streaks
Patchiness
A dark-shade paste that meets a low-shear viscosity target but produces patchy solids has not passed rheology qualification.
Fine Lines vs. Large Dark Solid Areas
Use both pattern types during testing.
Fine Lines
Reveal:
Post-print edge spreading under a defined drying delay
Spreading
Edge definition
Large Dark Solid Areas
Reveal:
Transfer uniformity
Coverage
Проникнення
Foam / pinholes
Shade variation
Fine-line prints show edge behaviour under the selected deposit, fabric and drying conditions; they do not alone quantify rheological recovery time. Measure recovery separately with defined shear history and elapsed time when that parameter is required. A thickener should not be approved from one simple design only.
Black and Very Dark Shades
Black can be a particularly useful stress test because many defects are visually obvious.
Check:
Solid coverage
Surface depth
Uneven penetration
Розповсюдження по краях
Screen running
But black pigment dispersion from one supplier should not be assumed to represent all dark pigments.
Carbon black and other dark pigments can use different:
Dispersant systems
Поверхнево-активні речовини
Particle concentrations
Qualify the actual commercial pigment used in production.
Holding-Time Stability in Dark Shades
High-pigment paste can be more sensitive to delayed interactions.
Measure:
Свіжа в’язкість
Intermediate viscosity
End-of-shift viscosity
pH
Піна
Separation / flocculation
A dark paste that looks stable at 10 minutes but thins or thickens strongly after several hours is not production-stable.
Compare light and dark shades at the same holding times.
Foam and Air Entrainment at High Pigment Loading
Higher pigment-dispersion dosage can increase the surfactant load in the paste.
Longer or stronger mixing can also introduce more air.
This can increase:
Visible foam
Microfoam
Apparent viscosity variation
Мікроотвори
Uneven deposit
If dark shades foam more strongly, check the pigment surfactant package and mixing before increasing defoamer blindly.
Rubbing Fastness and Binder Demand
Pigment fixation depends mainly on binder and curing.
Higher pigment loading can require review of the binder-to-pigment ratio to maintain rubbing performance.
If binder is increased, the thickener must then operate in a different:
Solids environment
Surfactant environment
Electrolyte environment
This is why dark-shade formulation should be evaluated as:
Pigment + Binder + Thickener + Curing
rather than adjusting pigment alone.
Fabric Hand and Total Polymer Solids
Dark shades can contain more pigment, more binder and sometimes more thickener.
This raises the total solids deposited on the textile.
Excess:
Плівка для пакування
Thickener polymer
Pigment solids
can contribute to a heavier or stiffer printed area.
Select a thickener dose within the verified screen-rheology and finished-fabric window. Repeat the candidate conditions with representative pigment, water, holding and machine variation before defining the production lower limit.
Do not restore the light-shade viscosity target at any cost if the dark paste prints acceptably at a different value.
Build a Light–Medium–Dark Shade Ladder
A practical qualification can use three pigment levels.
Shade Level
Purpose
Main Stress
Light
Low-pigment baseline
Reference rheology
Medium
Normal production range
Routine compatibility
Dark
High-pigment challenge
Surfactant / electrolyte / solids stress
Keep the thickener test method, fabric, screen and curing conditions constant.
This ladder compares the tested pigment-loading points under the recorded conditions. Repeat the relevant points and intended production variation before treating the grade as robust across a wider operating window.
Use a Water-Dilution Control
For an extra-addition diagnostic, split one homogeneous reference paste into equal weighed portions. Leave A unchanged, add a weighed amount of process water to B, and add the same as-supplied mass of extra pigment dispersion to C. Record the new final mass and thickener mass fraction for every portion. B is an all-water addition control, not an exact reconstruction of the dispersion carrier.
If the dispersion water fraction is disclosed, an additional carrier-water control can be informative, but any remaining mass and carrier ingredients must also be accounted for. Without that information, similarity between B and C is consistent with dilution but does not prove dilution is the only cause; different effects can offset one another.
For the separate production shade ladder, make all batches to the same final mass, retain the intended thickener dose and subtract extra pigment dispersion from make-up water. Compare pH, conductivity where useful, fresh and held rheology, screen transfer and cured fabric. This fixed-mass experiment tests the complete formulation response rather than automatic dilution.
Build a Pigment-Loading–Viscosity Curve
Instead of testing only one light and one dark shade, build several controlled pigment levels around the production range.
For each point, record:
Pigment-dispersion dosage
Кінцеве значення рН
Свіжа в’язкість
Стала в'язкість
Піна
Screen result
Plot:
Pigment Loading → Complete-Paste Viscosity
Do not force the trend into a straight line.
The curve may:
Fall
Rise
Remain flat initially and change sharply later
This is useful production information.
Build a Thickener Working Window for Dark Shades
If the dark-shade curve leaves the approved rheology window, build a small thickener dosage ladder at the high-pigment condition.
For each thickener point, evaluate:
Complete-paste viscosity
Shear thinning
Відновлення
Перенесення зображення на екран
Колірна віддача
Рука
The objective is:
A Validated Thickener-Dosage Window at the Required Dark-Shade Performance
не:
Restore the Exact Light-Shade Brookfield Number.
Recommended Laboratory Workflow
Define the current light and dark production formulas.
Use the same thickener batch and viscosity method.
Build a light–medium–dark pigment ladder.
Record pH and viscosity after pigment and binder.
Run a water-dilution control.
Measure fresh and held viscosity.
Print both fine-line and dark-solid-area patterns.
Cure under identical conditions.
Compare K/S, penetration, dry/wet rubbing and hand.
Adjust thickener only if the dark shade leaves the approved printing window.
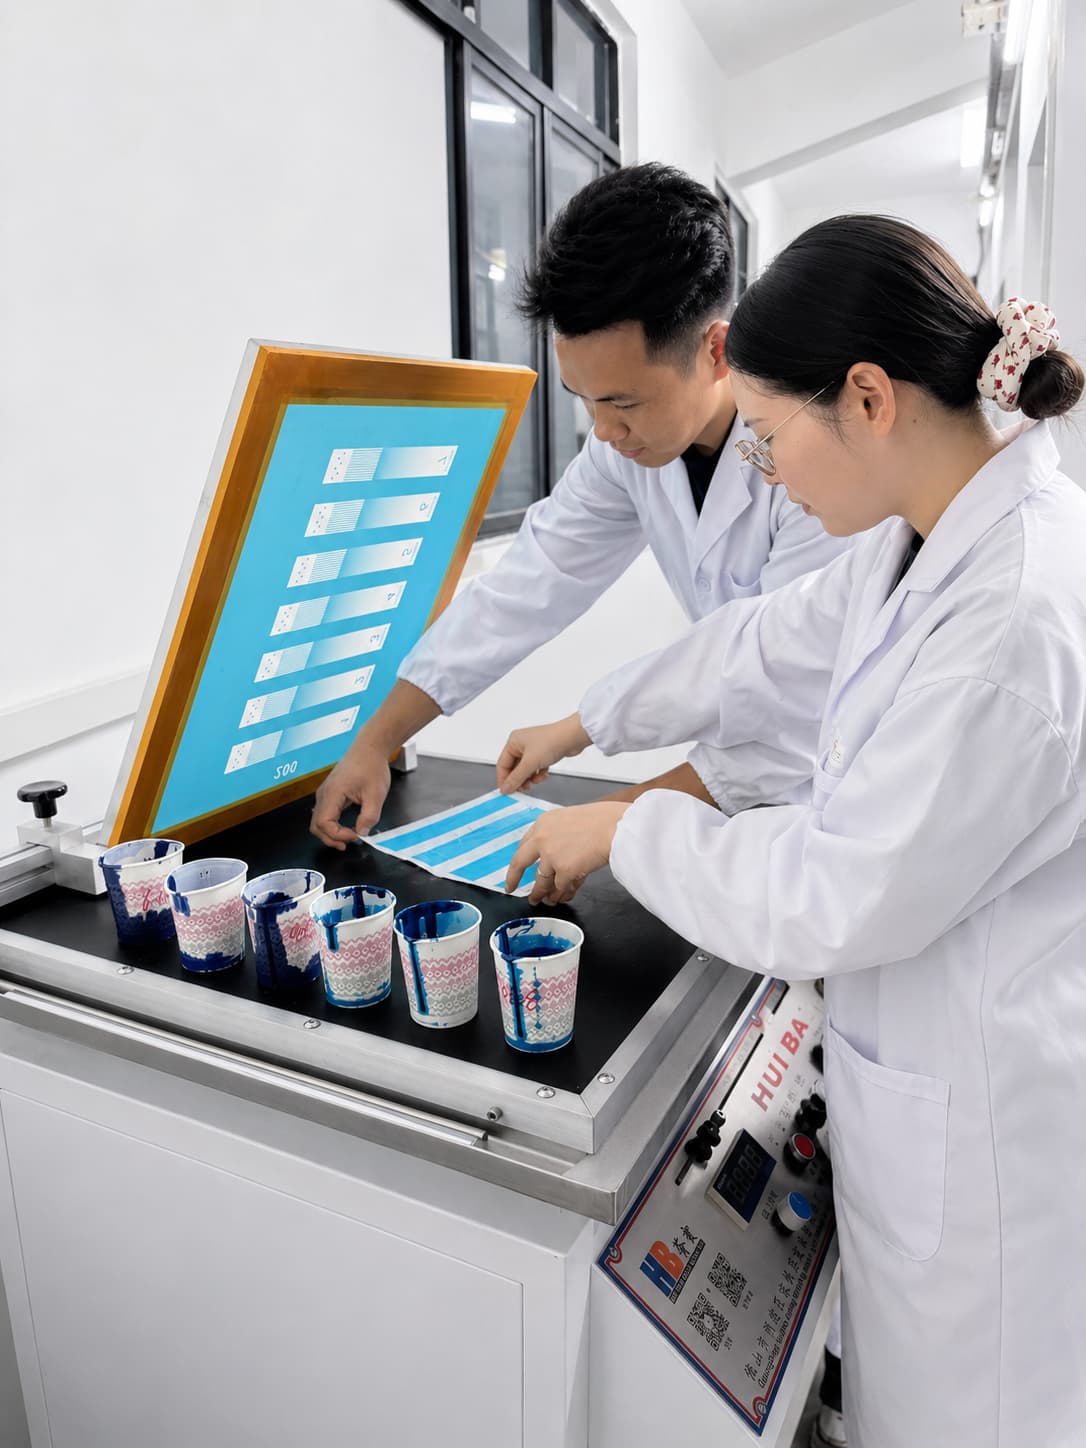
For a controlled current-vs-candidate comparison, FSX Chemical can review the formula through Зразки та підбір.
Затвердження випробувального виробництва
Run the best dark-shade laboratory condition on the actual production machine.
Запис:
Thickener grade and batch
Thickener dosage
Pigment product and dosage
Binder dosage
Кінцеве значення рН
В'язкість на початку / в середині / наприкінці циклу
Піна
Швидкість роботи верстата
Screen / squeegee settings
Покриття суцільної області
Затінення від початку до кінця
Проникнення
Отвердіння
Сухе / вологе протирання
Тканина ручної роботи
Approve a dark-shade operating window—not one successful laboratory swatch.
Common Dark-Shade Troubleshooting Mistakes
1. Assuming Dark Shade Always Needs More Thickener
Viscosity can decrease, increase or remain acceptable depending on the pigment package.
2. Treating Pigment Dispersion as Pure Pigment
It also adds water, dispersant, surfactant and sometimes electrolytes.
3. Ignoring Binder-to-Pigment Ratio
Fastness may change when pigment rises without an appropriate binder review.
4. Restoring the Light-Shade Brookfield Number Blindly
The dark paste may print correctly at a different viscosity.
5. Ignoring Particle Loading
High pigment solids can increase apparent viscosity or modify flow behavior.
6. Testing Fresh Paste Only
Dark shades can develop delayed rheology or compatibility changes.
7. Increasing Defoamer Without Checking Pigment Surfactants
Dark-shade foam can originate from higher dispersion/surfactant loading.
8. Approving from One Black Pigment
Different pigment products can use different dispersant and surfactant packages.
Dark-shade optimization should include more than pigment and thickener price.
A useful model is:
Cost per Saleable Unit = Total Attributable Production Cost ÷ Accepted Printed Output
Choose one denominator before comparing trials: accepted printed area in m² or accepted fabric mass in kg. Use the same fabric, design, quality criteria and costing boundary. Linear meters are comparable only when fabric width is also matched.
Cost component
Calculate in currency for the same trial or production run
Materials
Sum actual consumed quantity × unit price for pigment, binder, thickener and other auxiliaries. For a recipe estimate, thickener g/kg paste ÷ 1,000 × paste kg × supplied-product price/kg gives thickener cost. Reconcile actual use with returned or reusable paste.
Preparation and machine time
Recorded preparation, printing, cleaning and occupied equipment hours × the applicable cost rate. Lower speed or downtime changes these costs; efficiency is not a currency amount that can be added directly.
Energy, water and curing
Recorded consumption × unit tariff, including the relevant drying, curing and any approved washing route.
Additional rework or disposal
Include extra material, time, energy and documented disposal costs attributable to the failed output.
Accepted output
Use only printed area or fabric mass meeting the agreed color, fastness, definition and hand criteria as the denominator.
Dosage is an input to material cost, not an additional cost term. Avoid double counting: if an equipment rate already includes labor or energy, do not add them again. Material and processing spent on rejected output are already included in the run’s numerator and its lower accepted-output denominator; add only separate losses not yet counted. This is a proposed comparison worksheet, not an FSX measured cost-saving result.
A lower-cost pigment dispersion can become expensive if it creates:
Higher thickener demand
More foam
More binder correction
Lower machine speed
Poor color uniformity
A higher-efficiency thickener can justify a higher price if it keeps dark shades stable with lower dosage and softer hand.
Compare cost per acceptable printed meter.
Яку інформацію слід надіслати постачальнику загущувачів?
For useful dark-shade matching, provide:
Current acrylic thickener / TDS
Поточна доза згущувача
В'язкість та повна методика випробувань
Pigment product / color and dosage
Pigment solids if known
Binder grade and dosage
Фіксатор / допоміжні пристрої
Кінцевий рН пасти
Water hardness / conductivity if available
Тканина
Плоске або обертове сито
Час витримки
Light-shade vs. dark-shade viscosity data
Main issue: viscosity, color yield, transfer, rubbing, foam or hand
Компанія FSX Chemical може використовувати цю інформацію за допомогою Зразки та підбір to define a controlled pigment-loading and thickener-dosage comparison.
How Should a Mill Optimize Acrylic Thickener for Dark Pigment Shades?
A practical decision chain is:
Define Light / Dark Reference → Measure Pigment Loading → Check pH / Dilution / Surfactants / Electrolytes → Build Pigment-Loading Curve → Hold → Print Fine Lines & Dark Solids → Adjust Thickener Only If Needed → Cure → Check Color / Rubbing / Hand
Основними принципами є:
Higher pigment-dispersion dosage changes more than pigment concentration; it also changes the water, dispersant, surfactant and ionic environment.
High pigment loading can decrease or increase viscosity depending on dilution, electrolyte effects, particle loading and associative interactions.
Dark shades should not automatically use more thickener.
Color yield depends on transfer, penetration and surface pigment concentration—not pigment dosage alone.
Binder-to-pigment balance, foam and holding stability should be checked at the same time.
The best dark-shade formulation is the one that remains inside the approved rheology and finished-fabric window at the lowest practical Total Cost in Use.
Поширені запитання
1. Why does dark pigment paste become thinner?
If dispersion is added on top of an existing batch, dilution may contribute. At fixed final paste mass with make-up water adjusted, an unchanged thickener dose need not be diluted. Surfactants, dispersants, ions, pH and particle interactions can still alter rheology; check the actual mass balance and controlled comparisons before assigning the cause.
2. Can high pigment loading make the paste thicker instead?
Yes. Higher pigment solids can increase particle crowding, and associative thickener interactions can also raise viscosity in some formulas.
3. Should I always add more thickener for black pigment printing?
No. First measure the complete-paste rheology and printing result. Add more thickener only if the dark shade falls outside the validated production window.
4. Why can two black pigment dispersions give different viscosity?
They can contain different pigment solids, particle size, dispersants, surfactants, salts and pH-control chemistry.
5. Why can dark shades give weaker surface color than expected?
Excessive penetration, incomplete screen transfer, poor pigment dispersion or binder distribution can reduce surface color even when pigment dosage is higher.
6. Does higher pigment loading require more binder?
It may require a binder-ratio review to maintain rubbing fastness, but the correct level depends on pigment, fabric, binder chemistry and curing.
7. Why do dark shades foam more?
Higher pigment loading can introduce more surfactant/dispersant and can require longer or stronger mixing, increasing air entrainment and foam stability.
8. How can I tell whether viscosity loss is just dilution?
First check the final paste mass. Added dispersion can dilute an existing batch, while replacing make-up water at fixed final mass need not dilute the thickener. An equal-mass water addition is a screening control only; confirm carrier composition and other formulation effects before assigning the cause.
9. Should I test only the darkest shade?
No. A light–medium–dark ladder shows how the formula changes across the normal pigment-loading range and helps define a production window.
10. Why can HASE thickener behave differently at high pigment loading?
HASE uses hydrophobic association, so changes in pigment particles, dispersants, surfactants and binder can alter the associative network.
11. What should be checked after printing?
Evaluate print definition, solid-area uniformity, penetration, K/S or shade, dry/wet rubbing, foam-related defects and fabric hand after controlled curing.
12. What should I send FSX Chemical for dark-shade matching?
Send the current thickener/TDS, light and dark pigment dosage, viscosity method, binder, pH, water quality, machine route, holding time and the main color or rheology problem.
Match Acrylic Thickener to High-Pigment Dark Shades
If your light shades print well but black, navy or other dark pigment pastes become thinner, thicker, foamier or less uniform, FSX Chemical can help structure a controlled pigment-loading comparison.
Щоб отримати корисний технічний огляд, надішліть:
Your current acrylic thickener sample, TDS or COA
Поточна доза згущувача
Light- and dark-shade pigment products / dosages
В'язкість та повна методика випробувань
Binder grade and dosage
Fixer / auxiliary route
Кінцевий рН пасти
Water hardness / conductivity
Fabric and screen-printing route
Час витримки
Current color yield, transfer, rubbing, foam or hand target
Почніть з Зразки та підбір for a controlled current-vs-candidate evaluation.
The appropriate dark-shade dose is a validated operating range for the specific pigment, binder, fabric and process. Confirm that the selected production point maintains rheology, screen transfer, color, fastness and hand through the intended variation; one lowest passing laboratory point does not establish a universal minimum.
Separate reactive dye fixation from retained color and fastness. Review alginate preparation, application, alkali, paste age, steaming and wash-off through defined control comparisons; shade or rinse color alone does not establish fixation percentage.
Textile printing thickeners differ in chemistry, rheology, dye compatibility and wash-off behavior. This guide compares the main thickener families, their common application directions and the parameters buyers should verify before production trials.
Low color yield or poor fastness in reactive dye printing rarely has a single cause. This guide explains how fabric preparation, dye selection, thickener rheology, alkali, moisture, steaming and wash-off interact, and provides a practical troubleshooting and quality-control workflow.
Fabric pick-up determines how much pretreatment chemistry and water actually remain on the fabric after application. Too little or excessive pick-up can change color yield, bleeding, penetration, drying and fixation. This guide explains how to measure and optimize a stable working window for reactive inkjet printing.
Вибір синтетичного загущувача для пігментного друку повинен ґрунтуватися на повній системі «пігмент-сполучна речовина». Слід порівнювати такі параметри, як активація, рН, стійкість до електролітів, сумісність зі сполучною речовиною, реологічні властивості, ефективність дозування, результат затвердіння та кінцеві тактильні властивості тканини, а не лише в’язкість у воді.
Many acrylic liquid thickeners develop viscosity after neutralization, but the pH window is grade-specific. Evaluate the actual product dose, neutralizer, pigment, binder, electrolytes and holding time; nonvolatile content does not by itself identify active polymer.
В'язкість синтетичного загущувача може знизитися після додавання пігменту, сполучного або допоміжних речовин через розбавлення, зміну рН, екранування електролітів або несумісність складу. Правильний діагноз полягає в тому, щоб готувати пасту поетапно та визначити першу точку, в якій змінюється збереження в'язкості.
Пігментне сполучне може впливати на в’язкість акрилового загущувача шляхом розведення, зміни вмісту електролітів, зміни рН, взаємодії з поверхнево-активними речовинами та іонної сумісності. Повне випробування на сумісність має включати оцінку збереження в’язкості, стабільності при витримці, якості трафаретного друку, затвердіння, стійкості до стирання та тактильних властивостей тканини.
Ефективність синтетичного загущувача в трафаретному друку залежить не лише від статичної в’язкості. Оптимальні реологічні властивості поєднують в собі низьку в’язкість при зсуві, розрідження під ракелем та контрольоване відновлення після нанесення, що забезпечує хорошу друкованість, проникнення фарби та чіткість друку.
Зв’язок між дозуванням акрилового рідкого загущувача та в’язкістю не є чітко лінійним. Виробники повинні побудувати контрольовану робочу криву, використовуючи фактичний комерційний сорт, фіксований рівень pH та метод визначення в’язкості, а потім повторити відповідні точки дозування у повній рецептурі пігменту та зв’язувача.
Define the exact grade before comparing pigment-printing thickeners. Distinguish acrylic, CMC and documented carboxymethyl-starch chemistry from the FSX CMS commercial synthetic family, then compare complete-paste rheology and cured-fabric results.
Акриловий загущувач впливає на колірну віддачу пігментного друку, стійкість до стирання та тактильні властивості тканини головним чином через реологічні властивості, нанесення пасти, розподіл пігменту та сполучного, а також вміст твердих речовин полімеру. Перед оцінкою загущувача необхідно окремо контролювати сполучний та процес затвердіння.
Надайте назву продукту, сферу застосування, кількість, місце призначення, а також будь-які технічні специфікації (TDS),
зразки фотографій або документів, які у вас вже є. Компанія FSX Chemical розгляне цю
інформацію та надасть рекомендації щодо подальших кроків: підготовки комерційної пропозиції, підбору зразків
або вибору продукту.
Інформація про товарНазва товару, сорт, модель, фото етикетки або код постачальника.
Доступні документиTDS, SDS, COA, фото зразка, перелік продукції або дані випробувань.
Деталі замовленняОрієнтовна кількість, упаковка, країна призначення, порт або умови торгівлі.
Заявка чи проблемаПроцес друку на текстилі, вимоги до складу, поточні проблеми або цільові показники ефективності.