How to Test a Synthetic Textile Printing Thickener Before Production Approval
A synthetic textile printing thickener should not be approved from one viscosity result. Production approval...
Approve a synthetic textile printing thickener only after it passes defined tests in the complete production paste and on finished fabric. For the conventional pigment-screen route discussed here, compare activation, rheology, binder compatibility, holding stability, screen transfer, curing and agreed fastness against the current approved product. Connect the successful trial to a traceable commercial grade and verify the first bulk batch.
How Should a Synthetic Textile Printing Thickener Be Tested Before Production Approval?
Does it meet production and finished-textile requirements?
Screen running, definition, color, curing, rubbing, hand
Production approval is achieved only when all relevant levels pass.
Start with a Current Production Reference
The current approved thickener is the most useful control.
Run:
Current Approved Product vs. Candidate Synthetic Thickener
under the same:
Water
Pigment
Binder
Fixer / auxiliaries
Fabric
Screen
Squeegee conditions
Drying
Curing
Do not force equal dosage if the products have different thickening efficiency.
Instead, find the useful rheology window for each grade and compare the complete printing result.
A current reference prevents the laboratory from approving a candidate that looks technically acceptable in isolation but performs worse than the existing production standard.
1. Confirm Product Identity and Batch Traceability
Before technical testing, confirm exactly what has been received.
Record:
Supplier
Commercial grade
Batch / lot
Manufacturing or retest date where supplied
Package identification
TDS version
SDS version
COA
A development sample without a permanent commercial grade code can be useful for early screening, but it should not move directly into purchasing approval.
The approved sample must be connected to a repeatable production grade.
2. Inspect Appearance and Physical Condition
For liquid synthetic thickeners, check:
Color and uniformity
Separation
Settling
Surface skin
Gel particles
Graininess
Unusual odor
Damaged or swollen packaging
Appearance does not prove application performance, but abnormal physical condition should be investigated before the product enters the formulation.
If the product has experienced suspected freeze or heat exposure, use a separate storage-excursion review instead of normal approval testing.
3. Check Solids or Active Content
Separate as-supplied product dose, measured nonvolatile content and active thickening polymer. They are different quantities. The dried residue of a liquid commercial product can include polymer and other nonvolatile ingredients; a solids result alone does not establish active-polymer content.
Solids affect:
Effective polymer addition
Dosage comparison
Cost
Final polymer deposit
Compare:
As-Supplied Dosage
and:
Defined Nonvolatile Addition; Active-Polymer Addition Only When Documented
A lower dosage does not automatically mean a more efficient or lower-solids product.
Record the supplied specification and the exact drying method: sample mass, temperature, duration and endpoint. Nonvolatile addition = as-supplied dose × measured nonvolatile mass fraction. Calculate active-polymer addition only if its mass fraction is separately documented. ASTM D2369 is a coatings method for volatile/nonvolatile content; it is not a selective assay for active polymer and should not be adopted for an unfamiliar thickener without confirming applicability.
4. Check pH and Activation Behavior
Many acrylic and polyacrylate thickeners are pH-responsive.
Before comparing viscosity, determine:
Is the product supplied ready to use?
Is it partially neutralized?
Does it require controlled alkali activation?
What activation window does the TDS recommend?
Then standardize:
Neutralizer identity
Neutralizer concentration
Addition order
Mixing speed
Equilibration time
Final pH
Do not reject an alkali-swellable grade as “low viscosity” before confirming it has been activated correctly.
5. Build a Dosage–Viscosity Working Curve
Do not test only one dosage.
Prepare several controlled points around the supplier-recommended or current working region.
Measure:
Dosage
pH
Fresh viscosity
Held viscosity
Appearance
Plot:
Dosage → Complete-Paste Viscosity
The objective is to find:
A stable useful region
A steep region where small dosage changes create large viscosity changes
The lowest practical dosage that remains inside the production window
Do not assume dosage and viscosity are linear.
6. Compare Rheology, Not One Viscosity Number
A synthetic thickener can pass one Brookfield viscosity target and still print poorly.
Screen printing requires a flow sequence:
Low-Shear Body → Shear Thinning → Screen Transfer → Structural Recovery
Evaluate:
Low-shear viscosity
Multi-speed viscosity where available
Shear thinning
Recovery after controlled shear
Elasticity / stringiness
Thixotropy
ASTM D2196 distinguishes apparent viscosity, shear thinning and time-dependent recovery. For a mill comparison, fix concentration, water, preparation/rest history, temperature, instrument, spindle or geometry, container and reading time. Record torque and use a documented valid measuring range. A low-to-high speed series followed by defined low-speed recovery readings can screen differences; RPM is not a universal shear-rate conversion, and a two-speed ratio alone does not establish recovery or yield stress.
Therefore:
Same Brookfield Viscosity ≠ Same Printing Performance.
7. Run an Electrolyte-Tolerance Test
Many conventional polyacrylate thickeners are sensitive to ionic load.
Electrolytes can enter from:
Pigment dispersion
Binder
Fixer
Process water
Other auxiliaries
Run the candidate under a representative production electrolyte environment.
Measure:
Viscosity retention (%) = challenged-paste apparent viscosity ÷ matched unchallenged-control apparent viscosity × 100. Define the challenge chemical and its dose on the final-paste basis. Keep final dilution, temperature, mixing, rest period and measurement conditions matched; use a water-addition control where the challenge is supplied in solution. Calculate this ratio separately for each grade, then compare both absolute viscosity and print results. If the control is outside the instrument range or zero, do not report a ratio.
Compare with the current product.
Do not use a universal salt challenge if it does not represent the real formula.
8. Test Binder Compatibility
Binder is one of the most important compatibility variables in pigment printing.
Use a water-dilution control to separate simple dilution from chemical interaction.
A candidate should not be approved because it mixes into the binder without visible precipitation.
9. Test Pigment Dispersion Compatibility
Pigment dispersions can add:
Water
Dispersants
Surfactants
Electrolytes
pH-control chemicals
When the mill prints a wide shade range, check:
Representative light shade
Normal production shade
High-pigment / dark shade
A thickener that performs well at low pigment loading may lose viscosity at high loading.
Do not qualify the product on one easy shade only.
10. Check Filtration, Gel and Insoluble Risk
Even a liquid synthetic thickener can produce screen-blocking problems if the formula contains:
Gel particles
Coagulated polymer
Binder/pigment floc
Foreign contamination
Evaluate the relevant stage:
As-supplied product if applicable
Activated thickener base
Complete pigment paste
Held paste
Record filtration method, mesh or filter specification, time and residue appearance.
Filtration can remove particles, but it does not correct an incompatible formula.
11. Evaluate Foam and Mixing Behavior
Foam can interfere with:
Viscosity measurement
Pumping
Screen filling
Solid-area printing
Record:
Mixing speed
Mixing time
Foam generation
Foam collapse time
Defoamer response if used
A candidate that requires unusually aggressive defoamer correction can change the complete formula and should be evaluated on that final formula.
12. Verify Holding Stability
The complete paste should remain inside the approved window for the actual production holding time.
Measure at realistic points such as:
Fresh
Intermediate hold
End-of-shift
Record:
Viscosity
pH
Temperature
Foam
Separation
Gel / floc
One good fresh reading does not prove production stability.
13. Run Flat- or Rotary-Screen Application Tests
Use the intended production route.
Flat Screen
Check:
Squeegee transfer
Pause / restart
Recovery
Screen drying
Print definition
Rotary Screen
Check:
Pumpability
Continuous shear
Circulation stability
Mid-run viscosity
End-run viscosity
The candidate should be tested with representative screen geometry and fabric.
14. Dry and Cure Under Controlled Conditions
Pigment-printing qualification does not end at the printing machine.
The binder develops its fixation film during curing.
Keep constant:
Drying condition
Curing temperature
Curing time
Fabric lot
Use the binder supplier’s validated cure route and record the fabric thermal exposure, dwell time and drying condition, rather than relying only on an oven setpoint. Test reference and candidate after the same agreed conditioning. For example, ISO 105-X12 specifies dry and wet rubbing tests; name the method and edition in the report and apply the buyer’s agreed acceptance grades. The method does not set a universal pass grade for every pigment print.
If curing changes between candidate and reference, the thickener comparison becomes difficult to interpret.
15. Evaluate the Finished Fabric
Final approval should include the properties that matter commercially.
Depending on the buyer specification, evaluate:
Color strength / K/S or agreed shade comparison
Print definition
Penetration
Levelness
Dry rubbing fastness
Wet rubbing fastness
Wash fastness where relevant
Surface residue
Fabric hand
Use the mill’s agreed test standards and acceptance limits.
Do not invent new fastness requirements only for the candidate sample.
16. Check Fabric Hand and Polymer Deposit
Pigment printing places a binder film on the textile.
The thickener adds its own polymer solids.
Excessive total polymer deposit can make the printed area stiff.
Compare:
Candidate dosage
Active thickener solids
Binder solids
Paste deposit
Cured hand
A higher required dose is a reason to investigate deposit and cost, not proof that a grade is technically inferior. Compare measured paste consumption, documented nonvolatile addition, cured hand and agreed fastness inside each grade’s usable rheology window.
Use Go / Conditional / Fail Decision Gates
Decision
Recorded basis
Permitted next step
GO for this stage
Every agreed critical requirement for this stage passes under the named method and reference conditions. Record results, criteria and reviewer.
Advance to the next stage. Stage approval is not blanket commercial release; production and first-batch checks still apply.
CONDITIONAL — controlled test only
Name the unresolved criterion, proposed adjustment and authorized trial window: formulation range, duration/scale, responsible person and stop criteria.
Run only the next authorized controlled test and retest the affected requirements. This status does not permit commercial release. A change beyond the defined window, commercial grade or process route triggers requalification.
FAIL for this stage
An agreed critical requirement fails or the candidate cannot work inside the approved practical window.
Stop progression. Investigate or evaluate another grade through a newly defined controlled trial; do not bypass the failed criterion.
Examples of conditional results:
Viscosity slightly low but pH activation is not yet optimized
Good rheology but dosage curve is incomplete
Good lab printing but holding time has not been verified
Examples of fail conditions can include:
Severe binder incompatibility
Unacceptable electrolyte sensitivity
Persistent screen blocking
Unacceptable rubbing fastness under the approved binder/curing route
Unacceptable fabric hand at the dosage needed for stable printing
Scale from Lab to Production Carefully
Laboratory approval does not prove production-scale mixing.
Scale-up changes:
Impeller geometry
Mixing energy per unit volume
Addition time
Local concentration gradients
Temperature rise
Foam
When scaling up, preserve the process logic rather than copying laboratory RPM directly.
Confirm:
Addition order
Neutralization control
Mixing completion
Final pH
Final viscosity
Production Trial Approval
Run one controlled production trial with the best candidate condition.
Record:
Candidate grade and batch
Dosage
Complete formula
Final pH
Start viscosity
Mid-run viscosity
End-run viscosity
Machine speed
Screen / squeegee settings
Foam / cleaning events
Beginning-to-end shade
Print definition
Curing
Rubbing fastness
Fabric hand
A candidate should not be approved because the first few meters look acceptable.
The entire intended production window should remain stable.
First Commercial Batch Verification
Sample approval and commercial supply should be connected.
For the first commercial batch:
Confirm grade code and batch.
Review COA against the approved specification.
Run incoming QC.
Compare with retained approved sample.
Run a reduced application verification if required.
Release to normal production only after acceptance.
This step helps detect a common procurement risk:
Approved Sample ≠ Delivered Bulk Grade
especially when development samples were prepared separately from normal factory production.
Define Incoming QC Before Routine Supply
After production approval, define a practical incoming specification.
For a liquid synthetic thickener, this can include:
Product identity / grade
Appearance
pH
Solids or defined active-content parameter
As-supplied viscosity where meaningful
Standardized activated viscosity where appropriate
COA / batch traceability
Periodic application verification can include:
Electrolyte tolerance
Binder compatibility
Complete-paste viscosity
Screen trial
Incoming QC should detect batch drift without requiring a full production approval trial on every shipment.
This helps distinguish a thickener-batch issue from a printing-process issue.
Common Approval Mistakes
1. Approving on Water Viscosity
The complete pigment-binder formula can behave differently.
2. Comparing Equal Dosage Only
Different synthetic thickeners have different efficiency and solids.
3. Changing Thickener, Binder and Curing Together
The cause of improvement or failure becomes impossible to isolate.
4. Ignoring Holding Time
Fresh-paste success does not prove shift-long stability.
5. Ignoring Rheology
One Brookfield value does not describe screen transfer or recovery.
6. Stopping Before Curing
Pigment fixation is evaluated on the cured fabric.
7. Approving One Development Sample Without Grade Traceability
The commercial batch may not match the sample.
8. Selecting by Price per Kilogram
Working dosage, machine efficiency and quality loss determine real cost.
Practical Approval Matrix
Approval Area
Pass Question
Critical Failure Example
Identity
Is it the repeatable commercial grade?
Sample has no commercial traceability
Activation
Does it develop viscosity predictably?
Unstable pH response
Rheology
Does it transfer and recover correctly?
Severe stringing or spreading
Compatibility
Stable with binder / pigment?
Viscosity collapse, floc or gel
Holding
Stable for real production time?
Major end-of-shift drift
Screen Trial
Runs cleanly on intended machine?
Blocking, unstable transfer
Finished Fabric
Meets color, rubbing and hand requirements?
Fastness or hand failure
Bulk Consistency
First commercial batch matches approval?
Bulk material differs materially from sample
Total Cost in Use
Production approval should include the real economic effect.
A useful model is:
Cost per accepted printed metre = attributable material and operating costs for the trial run ÷ accepted printed metres. Use the same finished width and acceptance criteria; where widths differ, divide by accepted printed area (m²). Include the actual thickener and neutralizer consumed, any validated formula adjustment, preparation, printing, curing, cleaning and rework. Express all entries in the same currency and count each item once. Running speed changes operating time and rejected output changes the denominator; neither is a cost that can be added as a bare number.
A higher-priced thickener can be lower cost if it:
Uses lower dosage
Maintains viscosity with binder and pigment
Runs faster
Requires less correction
Reduces rejection
A cheaper thickener can become expensive if it requires more dosage, creates downtime or produces a harsher finished fabric.
Compare cost per acceptable printed meter rather than purchase price per kilogram. Where the product will run on both structures, include a controlled knit-versus-woven pigment printing trial; passing one fabric does not qualify the other automatically.
What Information Should You Send to a Thickener Supplier?
For efficient synthetic-thickener qualification, provide:
Current thickener sample / TDS
Current dosage
Complete viscosity method
Current solids / active content if available
Pigment dispersion
Binder grade and dosage
Fixer / auxiliaries
Final paste pH
Fabric
Flat or rotary screen
Screen mesh / engraving
Holding time
Curing temperature / time
Current rubbing and hand requirements
Estimated monthly usage
FSX Chemical can use this information through Samples & Matching to define a controlled current-vs-candidate trial.
One viscosity number does not qualify a synthetic thickener.
Use the current production product as the reference.
Test the complete pigment-binder formula before printing.
Evaluate rheology, holding stability and screen performance separately.
Final approval requires cured-fabric color, rubbing and hand results.
Commercial approval requires grade traceability and first-batch verification.
Frequently Asked Questions
1. What is the first test for a synthetic textile printing thickener?
Start by confirming the commercial grade, batch, TDS/COA and physical condition, then standardize solids, pH and activation before comparing viscosity.
2. Is water viscosity enough to approve a synthetic thickener?
No. The product must also be tested with the real pigment, binder, fixer and auxiliaries, followed by printing and curing.
3. Should two synthetic thickeners be compared at the same dosage?
Not as the only comparison. Find the useful rheology window for each grade, then compare printing, finished fabric and cost.
4. Why is electrolyte testing important?
Pigment, binder, fixer and process water can introduce ions that reduce thickening efficiency in some acrylic/polyacrylate systems.
5. How should binder compatibility be tested?
Add the binder under controlled conditions, record pH and viscosity, compare with a water-dilution control and check holding stability and final printing behavior.
6. Why should dark pigment shades be included?
High pigment loading can add more water, surfactant, dispersant and electrolyte, creating a stronger compatibility challenge.
7. How long should holding stability be tested?
Use the real production holding period. A four-hour production process requires evidence that the paste remains acceptable over that period.
8. What should be checked on the printed fabric?
Evaluate agreed color or K/S, print definition, penetration, dry/wet rubbing, relevant wash fastness, surface residue and fabric hand.
9. Is a successful laboratory trial enough for purchase approval?
No. Run a controlled production trial and verify the first commercial batch against the approved sample and specification.
10. Why keep retained samples?
They allow complaint batches to be compared with the approved reference using the same method and help separate batch issues from process issues.
11. What incoming QC is useful after approval?
Typical controls include identity, appearance, pH, solids or active-content parameter, applicable viscosity and batch documentation, with periodic application verification.
12. What should I send FSX Chemical before requesting a candidate synthetic thickener?
Send the current thickener/TDS, dosage, viscosity method, pigment, binder, pH, fabric, machine route, curing conditions, finished-fabric targets and estimated usage.
Qualify a Synthetic Thickener Before Bulk Production
If your mill is evaluating a new synthetic textile printing thickener, FSX Chemical can help structure a controlled current-vs-candidate comparison from laboratory screening through first commercial batch verification.
A synthetic thickener should be approved as a repeatable commercial system, not as one successful laboratory sample. Production approval begins with grade identity and ends with first-batch consistency, cured-fabric performance and a defined incoming-QC specification.
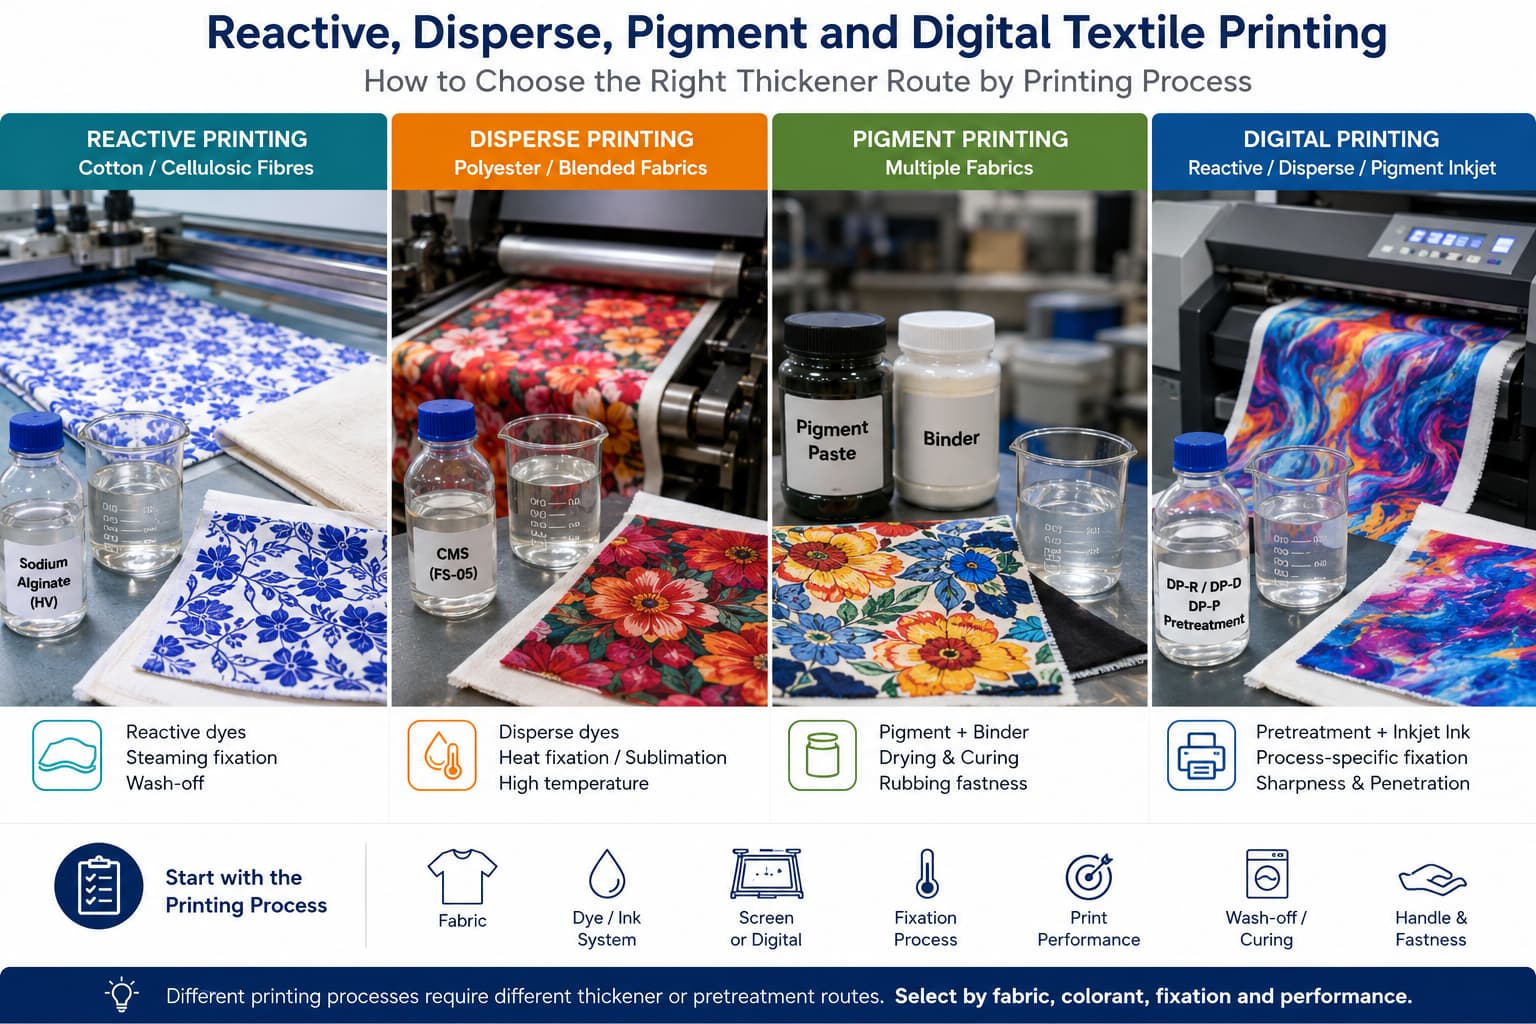
Learn how to choose thickener and pretreatment routes for reactive, disperse, pigment and digital textile printing based on fabric, dye or ink, fixation, wash-off and print-quality requirements.
Learn how to evaluate a textile printing thickener manufacturer by checking company identity, production capability, test methods, batch traceability, technical documents, sample support and export supply.
CMC-based printing paste is used across pigment, reactive, and digital textile printing. This guide explains what parameters matter, how to compare suppliers, and what to request before placing a bulk order.
Both sodium alginate and CMC are used as thickeners in textile printing, but they suit different dye systems and process conditions. This guide explains the key differences and when to use each.
Understanding sodium alginate raw material source and manufacturing process helps procurement teams ask better questions and evaluate suppliers more effectively. This guide covers seaweed species, extraction steps, impurity origins, and what consistent manufacturing looks like in supplier documentation.
Learn how to store sodium alginate powder and prepared paste, check shelf-life limits, and decide when a textile printing batch needs quarantine or retesting.
Technical datasheets vary in format and completeness between suppliers, and not every field matters equally for every application. This guide walks through a typical sodium alginate TDS section by section, explaining what each parameter means and how to spot gaps or red flags.
Define a sodium alginate customization request by the proposed material or packing change, agreed methods and evidence. Separate grade matching from a verified change, then qualify the sample, application and commercial lot before release.
Diagnose sodium alginate printing defects through controlled checks for bleeding, blockage, viscosity drift, low shade and wash-off. Treat causes as hypotheses, and verify them against the approved paste and process.
Sodium alginate prices vary significantly between suppliers and grades, but not all price differences reflect genuine quality differences. This guide explains what drives cost, how to structure a like-for-like quote comparison, and what red flags to watch for when evaluating supplier proposals.
The right textile printing thickener is determined by more than fabric type. Buyers should match the thickener to the dye or pigment system, printing method, target rheology, wash-off requirements and actual factory trial conditions.
Share the product name, application, quantity, destination and any TDS,
sample photo or document you already have. FSX Chemical will review the
information and recommend the next step for quotation, sample matching
or product selection.
Product InformationProduct name, grade, model, label photo or supplier reference.
Available DocumentsTDS, SDS, COA, sample photo, product list or test data.
Order DetailsEstimated quantity, packaging, destination country, port or trade term.
Application or IssueTextile printing process, formulation need, current issue or target performance.